Featured Industrial & Municipal Gas Monitoring Series
Explore our factory-direct, high-integrity detection devices, multi-gas systems, and automatic shut-off safety hardware engineered under ISO 9001 and certified explosion-proof parameters.
Global Procurement Imperatives for SO2 & Toxic Gas Instrumentation
Procurement officers, HSE plant directors, and international EPC project leads face an increasingly demanding matrix of sulfur dioxide (SO2) surveillance requirements driven by decarbonization, occupational hygiene mandates, and flue gas emissions monitoring.
Ultra-Low PPM Resolution
Sulfur dioxide presents severe pulmonary toxicity at minimal levels (OSHA PEL: 5 ppm, ACGIH STEL: 0.25 ppm). Tier-1 facilities require electrochemical cells engineered for 0.01 ppm detection thresholds with zero drift across -40°C to +70°C ambient shifts.
Harsh Corrosive Resilience
Flue-gas desulfurization (FGD), coal-fired power boilers, and non-ferrous smelters expose detection probes to sulfur trioxide (SO3) and moisture-induced sulfuric acid condensation, demanding 316L stainless steel or PTFE hydrophobic diffusion membranes.
Full Ecosystem Interlock
Detectors must not exist as isolated nodes. OEM architectures necessitate instantaneous Modbus RTU / 4-20mA HART handshakes with PLC/SCADA systems, driving emergency ventilation banks and fast-acting solenoid safety shut-off valves.
Turnkey White-Label Agility
Distributors require agile OEM customization—including modular sensor swap designs, private label casting enclosures, personalized firmware alarm curves, multilingual UI displays, and country-specific conformity documentation.
Industrial Solutions: Mitigation from Extraction to Stack
Deploying ruggedized fixed point gas detectors, distributed control-room consoles, and portable multi-gas platforms across critical enterprise infrastructures.
Sulfuric Acid Manufacturing & Mining Leaching
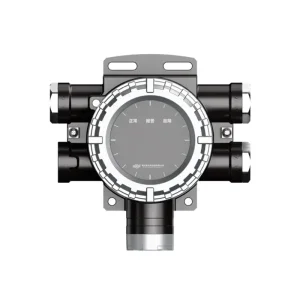
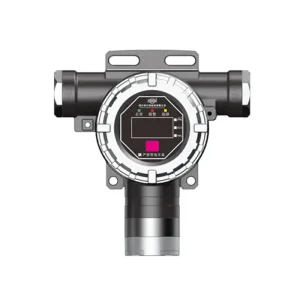
In double-contact double-absorption (DCDA) plants and copper/zinc froth-flotation roasting, SO2 concentrations reach thousands of ppm, while fugitive leaks threaten operator safety. Our SD2100E and point-transmitters utilize anti-acid housings with dual-range electrochemical or NDIR modules to provide instantaneous threshold triggers and prevent environmental non-compliance fines.
Petrochemical Refining & Claus Sulfur Recovery
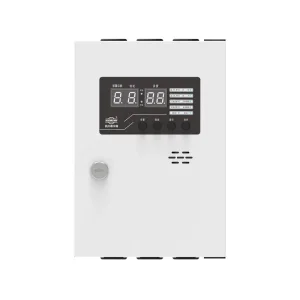
Petroleum refineries processing sour crude must monitor sulfur recovery units (SRU) and tail gas treating units (TGTU). Fixed-point explosion-proof detectors integrated with the SD8001A/B alarm controller system continuously verify seal boundaries around reactors, knockout drums, and hydrogen sulfide/SO2 thermal conversion chambers.
Thermal Power Generation & FGD Scrubbers
Continuous Emission Monitoring Systems (CEMS) rely on pre-scrubber and stack inlet monitoring to optimize limestone slurry dosers. Shield OEM fixed heads feed real-time digital analytics to central Distributed Control Systems (DCS), ensuring scrubbing uptime, lowering reagent consumption, and guaranteeing regional clean air compliance.
Pulp & Paper, Food Preservation & Cold Logistics
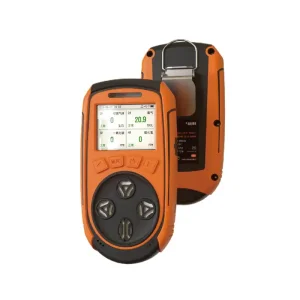
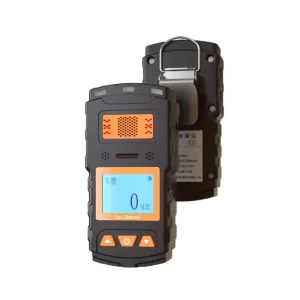
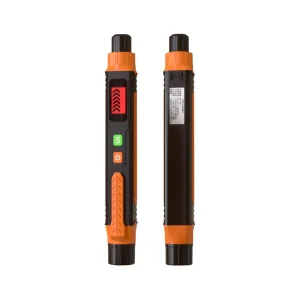
From bleaching towers in paper mills to winemaking and dried fruit processing where sulfur dioxide acts as an antimicrobial antioxidant, controlled atmosphere maintenance is imperative. Our 4-in-1 BTYQ-Z4 portable platforms and JLY-50A sniffer pens allow personnel to conduct tank vessel entry sweeps and valve packing checks with unmatched ergonomic speed.
Sensing Technology Roadmap: From Electrochemistry to Quantum Photonics
Sichuan Shield Technology integrates next-generation signal compensation algorithms, multi-layer ceramic sensing structures, and multi-spectral absorption technologies to overcome cross-sensitivity and environmental saturation.
Standardization of 3-electrode and 4-electrode micro-fuel cells with auxiliary reference electrodes, eliminating carbon monoxide (CO), hydrogen sulfide (H2S), and nitric oxide (NO) cross-interference during continuous atmospheric surveillance.
Integration of folded optical path Non-Dispersive Infrared and Ultra-Violet DOAS micro-benches for flue gas extraction, completely overcoming the electrolyte dry-out limitations in hot, high-humidity extraction stacks.
Implementation of embedded on-chip neural algorithms mapping temperature, humidity, and baseline calibration histories, alerting plant management 30 days prior to sensor exhaustion and automating zero-calibration cycles.
Next-generation Tunable Diode Laser Absorption Spectroscopy targeting specific SO2 absorption lines around 7.4 µm, realizing non-contact, maintenance-free, sub-second response monitoring directly inside process ductwork.
| Evaluation Parameter | Advanced Electrochemical (Shield Pro) | UV Resonance Absorption (Shield Opti) | Solid-State Semiconductor (Conventional) |
|---|---|---|---|
| Target Measuring Range | 0-20 ppm, 0-100 ppm, 0-500 ppm | 0-5,000 ppm, up to 10% Vol | 10-1,000 ppm (Non-linear) |
| Repeatability & Accuracy | ±2% Full Scale (Trace Precision) | ±1% Full Scale (Laboratory Grade) | ±10% to ±15% (High Variability) |
| T90 Response Latency | < 15 seconds | < 2 seconds | 30 - 60 seconds |
| Cross-Gas Immunity (CO, CH4, H2S) | Very High (Built-in Chemical Filtering) | Absolute (Direct Spectral Fingerprint) | Poor (Prone to broad hydrocarbon false trips) |
| Calibration Interval | 180 - 365 Days | 365 - 730 Days | 30 - 60 Days |
Rigorous Manufacturing Verification & Global Conformity
Every gas sensing terminal, multi-gas station, and solenoid shut-off valve leaving our Chengdu facilities undergoes automated multi-gas verification, climatic chamber stress testing, and explosion safety qualification.
Atmospheric Environmental Profiling
100% of our SO2 instruments are calibrated inside fully sealed automated mixing chambers, tracking span response under dynamic humidity (10% to 95% RH non-condensing) and extreme temperature excursions from -40°C to +70°C to guarantee field accuracy.
Explosion-Proof & Ingress Validation
Enclosures are hydrostatically burst-tested to Ex d IIC T6 Gb standards, combined with vacuum-sealed silicon O-rings ensuring IP66/IP67 ingress ratings. Units resist salt spray, high-velocity particulate abrasion, and petrochemical vapor penetration.
Multi-Tier Regulatory Harmonization
Our systems comply with China Mandatory CCC certifications, CE-EMC, ATEX, and IECEx engineering standards. Complete OEM documentation packages include certified circuit schematics, SIL2 reliability metrics, and bilingual calibration certificates.
Technical & Procurement FAQ: Sulfur Dioxide Detection Systems
Direct, engineer-verified solutions addressing critical system design, mounting physics, signal interfacing, and safety linkage questions.
Q1: How does sulfur dioxide density impact detector installation height?
Sulfur dioxide (SO2) has a molecular weight of 64.06 g/mol, approximately 2.2 times heavier than ambient air (28.97 g/mol). When released, SO2 settles toward low-lying elevations, floor channels, and trenches. Fixed SO2 detector heads must be mounted 0.3m to 0.6m above the finished floor level, adjacent to potential release fittings, valves, or process pumps, avoiding dead air corners or active floor extraction draughts.
Q2: Why should industrial projects integrate emergency shut-off valves with gas detectors?
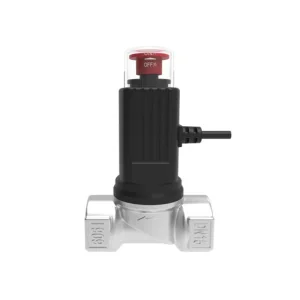
A gas monitor identifies leakage, but detection alone cannot eliminate hazard escalation. Coupling point detectors or controllers with our JYFJS-011 aluminum alloy electromagnetic shut-off valves establishes an instantaneous closed-loop safeguard. Upon reaching the low-alarm threshold, the controller sends a millisecond pulse to trip the solenoid, mechanically sealing the pipeline until manual reset confirms complete hazard abatement.
Q3: What is the operational difference between bus-type and stand-alone detectors?
Stand-alone detectors like our SD2130 series house internal audible-visual alarms and onboard auxiliary relays to directly switch ventilation fans or cut-off valves without control panel overhead—ideal for decentralized utility rooms. Bus-type systems (SD2100A / SD2100E) stream telemetry via 4-wire RS-485 Modbus or 4-20mA current loops back to central SD8001 consoles, enabling facility-wide mapping and automated fire matrix interlocks.
Q4: How do your electrochemical SO2 cells minimize cross-sensitivity to H2S and CO?
Shield electrochemical SO2 sensors utilize an optimized chemical electrolyte formulation paired with a high-capacity internal catalytic chemical filter. This absorbs hydrogen sulfide (H2S), nitrogen dioxide (NO2), and carbon monoxide (CO) prior to reaching the sensing electrode, ensuring selective oxidation and preventing catastrophic false alarm shutdowns in complex petrochemical environments.
Q5: What customizations are available under your OEM / ODM contracts?
As an integrated manufacturer with in-house tooling, SMT lines, and calibration bays, Shield provides full-spectrum OEM services: bespoke enclosure casting (aluminum alloy or 316L SS), custom front-panel silkscreening, tailor-made firmware baud rates, specialized Modbus memory registers, bespoke measurement ranges, private-label packaging, and country-tailored certification reports.
Q6: How often do SO2 detection platforms require bump testing and span calibration?
In accordance with OSHA and international ISA guidelines, portable devices should receive a quick functional bump test prior to each daily shift. Fixed point transmitters operate reliably with quarterly bump checks and full zero/span calibration intervals every 180 to 365 days, facilitated non-intrusively via our magnetic wand or infrared remote controls without opening the explosion-proof housing.
Industrial Point Monitors, Controllers & Isolation Hardware
Sichuan Shield Technology Co., Ltd. provides factory-direct integration spanning commercial kitchens, municipal distribution networks, refinery tank farms, and deep mining tunnels.