Certified Production Lineup
Precision Gas Detection Hardware Platforms
Turnkey OEM-ready instruments and field-tested actuators optimized for multi-zone combustible gas monitoring, personal safety telemetry, and emergency shut-off linkage.
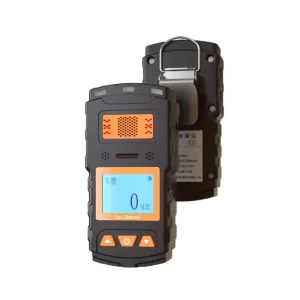
High-Quality China Supplier Portable Gas Detector SD3001 Series - Reliable Safety Monitoring
View Specifications →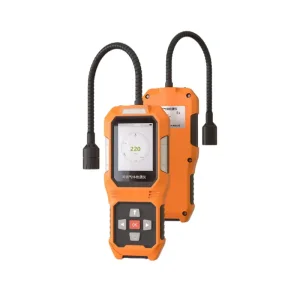
High-Quality Portable Gas Leak Detector Shield JLY-CP100 Series Manufacturer
View Specifications →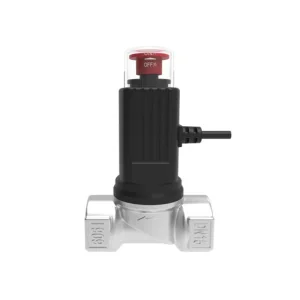
JYFJS-011 Aluminum Alloy Electromagnetic Shut-off Valve - Emergency Gas Safety Systems
View Specifications →
High-Quality 4 in 1 Portable Gas Detector Shield BTYQ-Z4 Series Reliable Safety Solution
View Specifications →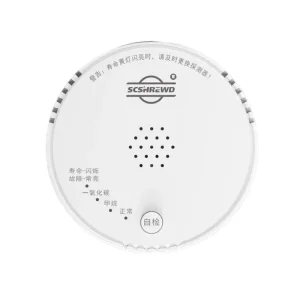
Wholesale Household Combustible Gas Detector SD6103K Series - Smart Gas Alarm
View Specifications →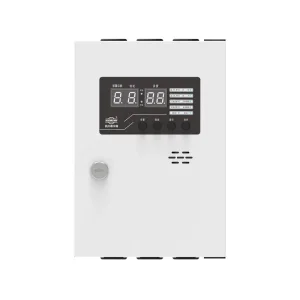
OEM Gas Alarm Controller Shield 8001AB Series Multi-Channel Centralized Monitoring
View Specifications →
OEM 4-in-1 Portable Gas Detector BTYQ-Z4 Series Industrial Factory Customization
View Specifications →
Industry White Paper
Macro Dynamics Driving Global Gas Safety Procurement
Enterprise buyers and municipal operators are migrating away from isolated alarms toward integrated toxic and combustible gas mitigation infrastructures driven by stricter ESG compliance and zero-tolerance workplace mandates.
18+
Years R&D Specialization
40+
Patented Sensing Technologies
80+
Standardized Hardware Platforms
<2s
Electromagnetic Valve Response
Dual CO/CH₄ Coexistence Risks
Combustion appliances generate both toxic Carbon Monoxide (CO) through incomplete fuel burn and volatile Methane (CH₄) via line pressure variations. Modern procurement specifications dictate integrated dual-channel sensing to prevent asphyxiation and Lower Explosive Limit (LEL) runaway inside single plant zones.
Stringent Regulatory Penalties
Enforcement across OSHA, ATEX, NFPA 715, and EU EN 50291 standardizes strict auditing protocols. Industrial infrastructure operators require verifiable zero-calibration stability and self-diagnostic fault signalling rather than basic passive indication.
IoT & Centralized Control Loops
Standalone buzzer alarms no longer satisfy large-scale facilities. Global developers demand RS485 Modbus, 4-20mA analog telemetry, and low-latency solenoid driving capabilities that automatically sever mainline fuel supplies without relying on human intervention.
“Systemic failure in industrial gas monitoring rarely originates from absolute sensor failure; rather, it stems from architectural disconnection between the gas threshold trigger and physical pipeline isolation mechanics. Total system reliability demands unified sensor-to-actuator engineering.”
Complete System Engineering
End-to-End Gas Detection & Physical Mitigation Architecture
Sichuan Shield Technology bridges the operational gap between early warning and mechanical safety isolation through five interdependent product layers engineered to eliminate common-mode failures.
1. Fixed Point Detection Layer
Stationary industrial point detectors (SD2100A, SD2100E) continuous monitor LEL concentrations in pump stations, boiler rooms, and petrochemical distillation sites, utilizing catalytic bead or infrared optics calibrated against ambient false-trigger cross-sensitivities.
2. Centralized System Supervisory Layer
The SD8001 series gas alarm controllers sit inside non-hazardous centralized control rooms, aggregating bus-line inputs from up to hundreds of remote sampling nodes. Programmable logic sets tiered pre-alarms (AL1 @ 25% LEL) and critical alarms (AL2 @ 50% LEL).
3. Fail-Safe Mechanical Isolation Layer
Integrated electromagnetic shut-off valves (JYFJS-011) deploy high-torque spring return mechanisms powered by millisecond electrical discharge pulses. Once triggered, the mechanical seat locks hermetically; physical manual intervention is strictly required to reopen the supply.
4. Personal Telemetry & Field Survey
Portable instruments including the BTYQ-Z4 4-in-1 multi-gas detector and JLY-CP100 sniffers safeguard field personnel entering confined vaults, utility trenches, and manholes where invisible, odorless stratification of CH₄, CO, and H₂S poses acute life risks.
Future Outlook
Technological Roadmap: The Evolution of Gas Sensing
How Sichuan Shield is navigating the generational shift from legacy electrochemical cells to micro-machined MEMS and optical dispersion systems for high-reliability detection.
Phase 1: Present Core
Catalytic & Electrochemical
Pellistor beads for high-concentration LEL combustible checks paired with room-temperature chemical cells for ppm CO detection. High reliability, field-proven over 18+ years of deployment.
Phase 2: Transition
MEMS & Low-Power NDIR
Silicon micromachined MEMS sensors with integrated micro-heaters drastically reduce current consumption, enabling extended battery endurance in portable units like the JLY-50A and BTYQ-Z4.
Phase 3: High Precision
Spectroscopic TDLAS Integration
Tunable Diode Laser Absorption Spectroscopy (TDLAS) calibrated to target methane's specific 1.65 µm absorption band, completely eliminating false alarms triggered by cleaning vapors or alcohol.
Phase 4: AI & Predictive
Edge-AI Drift Compensation
Embedded machine learning models inside the SD8001A/B supervisory processors calculate thermal drift, humidity fluctuation curves, and background noise to predict sensor end-of-life before failure.
Global Compliance
Enterprise OEM/ODM Localization & Regulatory Assurance
Meeting local technical codes is critical to commercial feasibility. Shield provides comprehensive customization suites to help global distributors clear regional testing authorities.
Standardized Certifications
Our complete gas-safety portfolio holds mandatory 3C (CCC) certifications, CE directives, explosion-proof testing compliance, and factory audit verification under ISO 9001:2015 quality management systems.
Custom Firmware & Telemetry
We tailor bus protocols to integrate seamlessly with third-party BMS architectures. Whether your regional infrastructure relies on Modbus RTU, BACnet, Zigbee, LoRaWAN, or NB-IoT, our in-house firmware engineers configure the stack.
Private Labeling & Mold Tooling
From injection molding alterations, UV-stabilized fire-retardant housings (UL94-V0), and custom screen printing to retail packaging, brand guidelines are strictly preserved for global Tier-1 distribution partnerships.
Engineering Insights
Frequently Asked Technical & Procurement Questions
Direct technical answers addressing setpoints, installation methodologies, cross-sensitivity management, and system architecture design.
Is the Lower Explosive Limit (LEL) the same as the detector alarm setpoint?
No. The LEL represents the minimum volume percentage at which a gas combusts in air (for methane, roughly 5% VOL equals 100% LEL). Safety alarm thresholds are programmed far below this point—typically at 10% to 25% LEL—ensuring actionable containment time before explosive mixtures form.
Where should combination or standalone gas detectors be mounted?
Placement depends on target vapor density. Natural gas (Methane) is lighter than air (relative density ~0.55) and rises, requiring detector placement 30cm below the ceiling. LPG is heavier than air (~1.55) and settles, requiring placement 30cm above the floor. CO shares near-neutral atmospheric density (~0.97) and should be mounted at breathing level (~1.5m).
Why do oxygen sensors read in %VOL while CO sensors read in ppm?
Atmospheric oxygen occupies 20.9% of normal air by volume, making volume percent (%VOL) the standard metric for hypoxia (<19.5% VOL) or hyperoxia (>23.5% VOL). Carbon Monoxide is acutely toxic at tiny trace quantities; safe occupational exposure limits (OSHA PEL 50 ppm) necessitate high-resolution parts-per-million electrochemical measurement.
Can Shield detectors automatically trigger physical pipeline isolation?
Yes. Shield detectors (including household SD6200 and industrial SD2130 units) incorporate onboard pulse/relay outputs paired with JYFJS-011 aluminum alloy electromagnetic valves. Upon reaching alarm thresholds, an impulse drops the valve seal in milliseconds, requiring a secure manual pull-reset after leak remediation.
What defines the choice between standalone and bus-type point detectors?
Standalone units (SD2130) operate autonomously with integrated audio-visual sounders and direct valve drive for single boiler rooms or commercial kitchens. Bus-type detectors (SD2100A/E) run multi-drop network lines to an SD8001 central controller, which provides consolidated SCADA telemetry, multi-stage voting logic, and unified facility safety management.
What are the lead times and Minimum Order Quantities (MOQs) for OEM branding?
Standard catalog models are stocked for rapid assembly with typical turnaround of 7-14 business days. Custom OEM orders (housing colorways, private badging, packaging) generally start at low trial-run MOQs (50-200 units), while full firmware protocol development and specialized tooling run along a 4-8 week validation cycle.
Complete Series Platforms
Integrated Household, Commercial & Portable Safety Hardware
Explore our extended series of point-type transmitters, leak sniffers, and multi-gas monitors ready for enterprise labeling and international deployment.
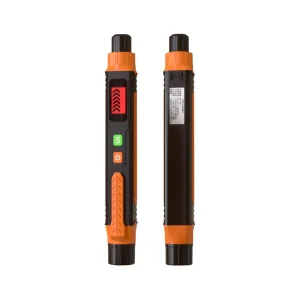
OEM Portable Gas Detector Pen JLY-50A Series - High-Sensitivity Inspection Equipment
View Specifications →
High-Quality China SD6200 Series Household Combustible Gas Detector Factory Solution
View Specifications →
High-Quality China Household Combustible Gas Detectors 6101 Series Safety Solutions
View Specifications →
High-Quality China Household Combustible Gas Detector SD6103K Series Reliable Safety
View Specifications →
High-Quality Portable Gas Detector Shield SD3001 Series Supplier & Factory
View Specifications →
ODM China Gas Detector Shield SD2100E Series - Industrial Safety Solutions
View Specifications →
ODM China Industrial and Commercial Gas Detector SD2130 Series Factory Solutions
View Specifications →