High-Reliability Fixed & Portable Safety Instrumentation
Explore our core explosion-proof transmitters, central controller mainframes, and pipeline safety shut-off systems deployed by global industrial integrators, utility plants, and EPC distributors.
The Global Imperative for Fixed Continuous Gas Monitoring
Stringent decarbonization goals, fugitive emissions mandates, and rigorous occupational health regulations have catalyzed a structural shift from passive, walk-around gas inspections to intelligent, continuously instrumented fixed monitoring architectures.
Regulatory Compliance Mandates
Global regulatory bodies including OSHA (29 CFR 1910.120), the European Seveso III Directive, and China's State Administration for Work Safety (GB 50493 & GB 15322) mandate uninterrupted telemetry for toxic and explosive atmospheric threats. Plants lacking certified fixed continuous instrumentation face immediate operational shutdown orders, prohibitive non-compliance fines, and invalidation of corporate risk insurance underwriting.
Continuous Zero-Blindspot Telemetry
Unlike portable sniffers that rely on human patrol cadence, fixed monitoring arrays operate 24/7/365 within dangerous, unventilated, and classified explosive zones. Real-time ppm and %LEL concentration tracking detects sub-surface valve seat leakage, pipeline flange micro-fractures, and process vessel seal breaches before hazardous combustible vapor reaches flammable lower explosive threshold levels.
Direct Factory Wholesale Procurement
Industrial distributors and EPC contractors are progressively moving away from regional third-party brand markups in favor of direct engagement with tier-1 original design manufacturers (ODMs). Factory-direct sourcing enables precision hardware adaptation, specialized firmware protocol customization (Modbus-RTU, BACnet, HART), rapid SIL certificate provisioning, and substantial unit-cost economies of scale.
| Detection Technology | Target Gas Spectrum | Operating Principle | Response Time (T90) | Drift Stability | Optimal Industrial Deployment |
|---|---|---|---|---|---|
| Catalytic Combustion (Pellistor) | Combustible Hydrocarbons (Methane, Propane, LPG, H2) | Catalytic oxidation across active vs reference ceramic beads creating a Wheatstone bridge balance shift | < 15 seconds | Moderate (requires recalibration every 3-6 mos) | Refineries, natural gas boiler rooms, chemical storage facilities |
| Non-Dispersive Infrared (NDIR) | Methane, CO2, Hydrocarbons (fail-safe optical path) | Target gas absorption across narrow infrared spectrum (3.3 – 3.4 µm) without oxygen dependence | < 10 seconds | Superior (dual-beam auto-compensation, zero-drift) | Offshore oil rigs, inert gas purging chambers, hypoxic environments |
| Electrochemical Amperometric | Toxic Gases (CO, H2S, NH3, Cl2, SO2, NO2, O2) | Redox electrochemical reactions across working, counter, and reference electrodes generating linear current | < 25 seconds | High accuracy, cell electrolyte depletion over 2-3 years | Water treatment plants, pharmaceutical synthesis, chemical reactors |
| Photoionization (PID - High Energy UV) | Volatile Organic Compounds (VOCs, Benzene, Toluene) | Ionization of chemical molecules via 10.6 eV / 11.7 eV krypton ultraviolet radiation lamp | < 3 seconds | High sensitivity (ppb/ppm levels), lamp cleans periodic | Semiconductor cleanrooms, petrochemical fenceline monitoring |
End-to-End Fixed Gas Monitoring Hardware Ecosystem
A resilient gas safety system requires absolute hardware cohesion between field sensing nodes, central supervisory processing logic, and automatic mechanical hazard mitigation actuators.
1. Hazardous Area Sensing Layer
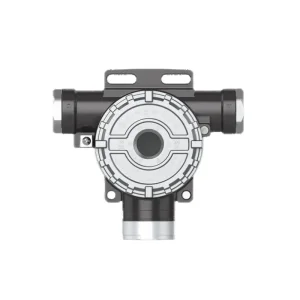
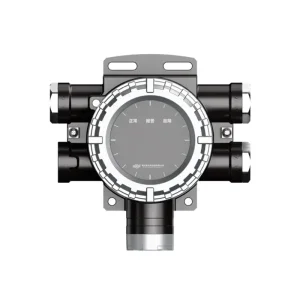
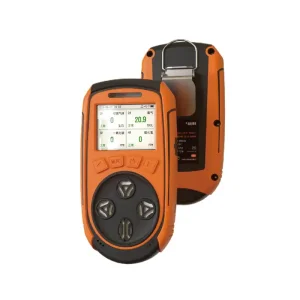
Our SD2100A and SD2130 series field detectors are encased in die-cast aluminum alloy or 316 stainless steel explosion-proof housings rated Ex d IIC T6 Gb / IP66. They feature pre-calibrated smart sensor cassettes, non-intrusive magnetic wand / infrared remote calibration, and localized daylight-visible OLED concentration displays with audible-optical strobes.
- Continuous sampling via natural molecular diffusion or optional vacuum draw
- Integrated temperature and humidity micro-compensation algorithms
- Multi-drop 4-wire M-Bus / RS-485 Modbus RTU & 3-wire 4-20mA HART output
2. Control Room Central Logic Layer
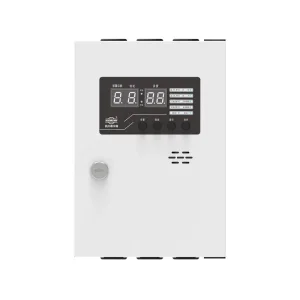
Positioned inside the safe control room, the Shield 8001AB series gas alarm controller processes continuous telemetry from dozens to hundreds of field detection nodes. Featuring a dual-microcontroller voting architecture and SIL-2 functional capability, it arbitrates alarm priorities, maintains time-stamped rolling blackbox audit logs, and coordinates multi-stage trip routines.
- High-contrast multi-channel LCD matrix showing live %LEL/ppm values
- Independently programmable Low (A1) and High (A2) alarm thresholds
- Seamless DCS/SCADA handshake through dual isolated RS-485 and Ethernet
3. Automated Mechanical Isolation Layer
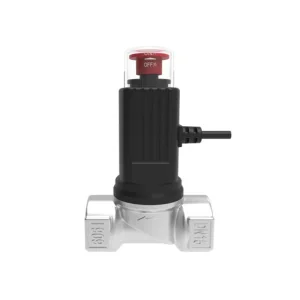
Detection without isolation fails to prevent catastrophe. Our JYFJS-011 aluminum alloy electromagnetic solenoid emergency shut-off valves interface directly with the controller or stand-alone detector relays. Upon exceeding the A2 safety limit, a millisecond electromagnetic pulse triggers an immediate mechanical spring-assisted valve cutoff, isolating pipeline fuel flow.
- Ultra-fast closing execution time: less than 0.5 seconds
- Strict manual mechanical reset requirement preventing unauthorized gas re-entry
- Zero internal spark generation: fully certified explosion-proof coil build
Mission-Critical Application Scenarios & Tailored Configurations
From explosive hydrocarbon processing to toxic chemical manufacture, each operating environment poses unique chemical reactivity, temperature variations, and airflow turbulence challenges.
Petrochemical & Refinery Complexes
Primary Hazards: Fugitive methane, volatile hydrocarbons (C1-C8), hydrogen sulfide (H2S), and catalytic reforming by-products within Zone 1 and Zone 2 hazardous areas.
System Configuration: High-density array of SD2100A point-type combustible detectors equipped with poison-resistant catalytic beads and NDIR optical sensors situated at pump seals, distillation columns, and pipe racks. Interlinked directly to rack-mount 8001AB control panels with automated dry contacts triggering site-wide explosion-proof sirens and water deluge monitors.
Battery Energy Storage Systems (BESS)
Primary Hazards: Lithium-ion battery cell thermal runaway off-gases (Carbon Monoxide, Hydrogen, Methane, Hydrofluoric Acid) preceding catastrophic cell fire.
System Configuration: Specialized multi-sensor arrays deploying dual CO (ppm) and H2 (%LEL) electrochemical and catalytic sensors mounted in container ceiling spaces. Early off-gas detection at ppm levels signals HVAC purge dampers and fire-suppression dry-chemical deployment long before standard smoke or thermal detectors trigger.
Cryogenic LNG Bunkering & Vaporization
Primary Hazards: Super-chilled methane boil-off gas (BOG), localized cryogenic oxygen displacement, and rapid thermal expansion vapor clouds.
System Configuration: Low-temperature compensated NDIR transmitters rated down to -40°C installed around LNG regasification skids, marine loading arms, and storage sphere perimeters. Transmitters communicate via fail-safe isolated current loops to emergency shut-off valves capable of sealing manifold lines in under half a second.
Hydrogen Production, Electrolysis & Fueling Stations
Primary Hazards: High-pressure H2 leaks possessing an exceptionally wide explosive limits profile (4.0% to 75.0% by volume) and microscopic molecular dispersal velocity.
System Configuration: Ultra-fast response pellistor and thermal conductivity transmitters installed at high containment peaks and canopy ceilings. System logic integrates with automatic blowdown vents, emergency nitrogen blanket purges, and automated plant-wide power interlocks.
Commercial Hospitality, Boiler Rooms & District Heating
Primary Hazards: Natural gas pipeline joint failure, incomplete gas burner combustion (CO hazards), and commercial cooking manifold leaks.
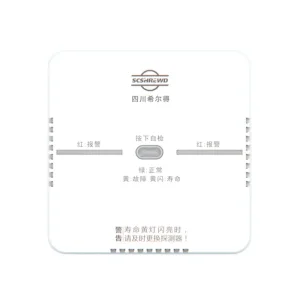
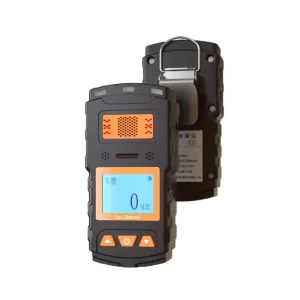
System Configuration: Cost-effective, stand-alone SD2130 and SD6200 commercial detectors operating without costly central cabinets. The internal relay outputs directly switch mechanical ventilation exhaust louvers while instantly cutting JYFJS-011 gas pipeline solenoid valves upon A1 trip detection.
Global Regulatory Compliance & OEM/ODM Factory Infrastructure
Gas safety devices are life-critical instrumentation. Sichuan Shield Technology couples rigorous scientific metrology calibration with state-of-the-art automated contract electronics manufacturing.
Certified Explosion-Proof
Standard compliance with ATEX Directive 2014/34/EU, IECEx, and China CCC explosion-proof standards for Ex d IIC T6 Gb flameproof enclosures, allowing direct deployment in flammable vapor atmospheres without explosion risk.
SIL-2 Functional Safety
Designed and documented according to IEC 61508 / IEC 61511 functional safety standards, ensuring ultra-low Probability of Failure on Demand (PFD) and robust hardware fault tolerance across critical process loops.
NIST-Traceable Calibration
Every detector is calibrated across precision environmental chambers using certified primary standard test gases. Automated burn-in regimens verify zero thermal drift and response linearity across 0% to 100% LEL.
Agile OEM/ODM Solutions
We supply turnkey OEM/ODM engineering: custom die-cast toolings, private-label branding, customized register maps for industrial Modbus/BACnet networks, and custom voltage inputs for defense, marine, and mining contractors.
Technology Roadmap: The Evolution of Gas Safety Monitoring
The convergence of artificial intelligence, low-power industrial wireless telemetry, and solid-state photonic sensing is driving the next generation of fixed gas monitoring ecosystems.
Edge AI Baseline Self-Calibration
Future iterations of Shield fixed transmitters incorporate edge-computing microcontrollers running real-time statistical inference. These algorithms track ambient environmental drift, humidity fluctuations, and minor sensor aging effects, dynamically recalibrating the zero-point baseline without requiring technician site visits, effectively eliminating false positive nuisance trips.
Explosion-Proof Wireless Mesh (LoRaWAN / 5G RedCap)
Retrofitting multi-kilometer industrial plants with traditional explosion-proof armored conduit cabling represents up to 60% of total project capital cost. Our technology roadmap incorporates intrinsically safe, ultra-low power wireless mesh transmitters that transmit continuous health and gas telemetry over kilometer distances with battery lifespans exceeding 5 years.
Spectroscopic Miniaturized Laser Absorption
Migrating beyond traditional chemical cells, we are pioneering compact Tunable Diode Laser Absorption Spectroscopy (TDLAS) modules. TDLAS provides absolute gas specificity for methane and hydrogen without any cross-sensitivity to other volatile hydrocarbons, unaffected by sensor poisons like silicone vapors or hydrogen sulfide.
Frequently Asked Questions: Engineering & Procurement
Detailed technical guidance for safety instrumentation managers, system integrators, and procurement directors evaluating fixed gas detection systems.
Q01 What is the operational distinction between Lower Explosive Limit (%LEL) and Parts Per Million (ppm)?
The Lower Explosive Limit (LEL) represents the minimum volume concentration of a combustible gas in air necessary to support flame propagation upon ignition. For example, the LEL of methane is 5.0% by volume in air; therefore, a display reading of 100% LEL corresponds to 50,000 ppm of methane. Monitoring in %LEL is used for combustible fire and explosion mitigation, with primary alarms usually configured at 20% to 25% LEL. Conversely, toxic gas detection (such as CO, H2S, or NH3) operates at the much more sensitive ppm (or ppb) scale to prevent physiological injury, chronic toxicity, or immediate lethal asphyxiation long before combustible thresholds are reached.
Q02 What factors dictate whether to select catalytic combustion (pellistor) or infrared (NDIR) transmitters for hydrocarbon gas detection?
Catalytic pellistor sensors operate through chemical oxidation and are optimal for detecting hydrogen (which does not absorb infrared radiation) as well as lower-cost hydrocarbon protection. However, pellistors require at least 10-12% oxygen to operate and are vulnerable to irreversible poisoning by silicones, lead, sulfur compounds, and halogenated hydrocarbons. NDIR optical sensors utilize infrared light absorption and do not require oxygen, allowing continuous operation in inert nitrogen-blanketed tanks. NDIR sensors are entirely immune to chemical poisons and exhibit negligible zero drift, resulting in significantly lower lifecycle maintenance overhead despite higher upfront equipment costs.
Q03 How are spatial sensor density and mounting elevation determined across plant topologies?
Mounting elevations strictly follow target gas molecular density relative to air (air = 1.0). For gases lighter than air (e.g., Methane at 0.55, Hydrogen at 0.07), sensors must be installed within 30 to 60 cm of the ceiling or directly above potential leakage points like flanges, valves, and compressors. For gases heavier than air (e.g., Propane at 1.55, H2S at 1.19, Chlorine at 2.45), transmitters are installed 30 to 60 cm above floor level or drainage sumps where vapors accumulate. Sensor density is typically engineered with a 5-meter coverage radius in unobstructed indoor facilities and a 2.5-meter radius in dense industrial equipment structures, adhering strictly to standards like EN 60079-29-2 and NFPA 72.
Q04 Why is manual mechanical reset mandatory for emergency gas solenoid shut-off valves?
Safety engineering regulations (including NFPA 54, EN 161, and GB 50028) prohibit the automatic re-energization or reopening of gas supply pipelines after a safety trip. When a detector signals the JYFJS-011 solenoid valve to trip, an unlatching spring isolates the flow within 0.5 seconds. Forcing a physical human intervention to inspect the site, identify the leak, repair the defect, and physically reset the valve handle guarantees that fuel cannot flow back into an uncleared, compromised hazard zone.
Q05 What communication topology is superior: Point-to-Point 4-20mA current loop or Multi-Drop RS-485 Modbus?
The choice depends on plant architecture and safety integrity requirements. An analog 3-wire 4-20mA loop (with HART protocol) provides dedicated, point-to-point physical cabling directly to safety PLC cards, offering immunity from communication packet collisions and meeting SIL-2/SIL-3 functional safety requirements with instant line fault detection (e.g., <3.6 mA signaling sensor fault). Conversely, 4-wire RS-485 / M-Bus networks dramatically reduce installation cabling costs by daisy-chaining up to 128 transmitters on a single twisted pair, transmitting concentration data, diagnostic codes, and temperature readings over a single network loop.
Q06 What are the lead times, minimum order quantities (MOQs), and customization capabilities for factory OEM/ODM orders?
As an original manufacturer with over 18 years of technical history, Sichuan Shield Technology maintains rapid B2B factory throughput. Standard white-box or branded production runs typically feature MOQs starting at 50 to 100 units with 2-to-3 week delivery turnarounds. Comprehensive ODM contracts involving custom die-cast molds, proprietary PCB design, private-label firmware register development, and international certification submissions (ATEX, CE, UL) follow a structured 8-to-12 week milestone schedule from engineering validation to full-scale SMT line manufacturing.
OEM/ODM Gas Detection & Safety Isolation Hardware
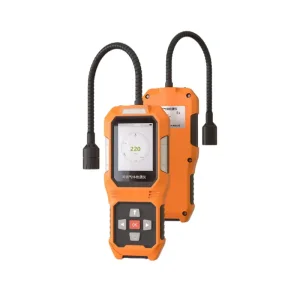
Review our specialized commercial detectors, handheld pinpoint leak survey pens, high-volume residential safety platforms, and pipeline electromagnetic shut-off valves.