Precision Gas Detection Hardware: Featured Supply Series
Verified gas-tight detectors, localized point monitors, and emergency shut-off linkage components engineered by Sichuan Shield Technology Co., Ltd. for turnkey project integration.
The Global Landscape of Fixed Wall-Mounted Gas Detection
How statutory environmental mandates, aging utility pipelines, and volatile green energy transitions drive industrial demand for reliable wall-mounted gas sensing platforms.
Strict Regulatory Compliance
Occupational Safety and Health Administration (OSHA), ATEX (2014/34/EU), IECEx, and China’s mandatory CCC (GB 15322 series) strictly stipulate fail-safe combustible and toxic gas monitoring across hydrocarbon handling hubs. Modern installations necessitate redundant alarms well before reaching Lower Explosive Limits (LEL), driving retrofits from uncalibrated point sensors to intelligent bus-connected wall monitors.
Energy Transition & Hydrogen Blends
With municipal gas utilities trialing up to 20% hydrogen-methane admixtures (HCNG) to curb carbon footprints, standard catalytic pellistors encounter cross-sensitivity challenges and accelerated thermal drift. Leading factories have innovated dual-channel pellistor/electrochemical and Non-Dispersive Infrared (NDIR) wall monitors capable of dynamically linearizing mixed-gas concentrations.
Uninterrupted Industrial 24/7 Operations
In continuous petrochemical, metallurgical, and municipal processing plants, false alarms trigger costly downtime and emergency ventilation cycles. EPC contractors now demand wall-mounted sensing modules with on-board drift compensation, self-test diagnostics, and sealed ingress (IP65/IP66) to survive hostile industrial atmospheres without drifting out of calibration.
Why Tier-1 Global Procurement Selects Advanced Chinese Factories
Inside Sichuan Shield Technology's Chengdu precision manufacturing center: how consolidated R&D, in-house tooling, and automated calibration chambers disrupt traditional safety instrumentation economics.
End-to-End Vertical Ecosystem
Unlike European and North American brand assemblers who outsource sensor packaging, circuit layout, casting, and valve production to disjointed third parties, premier Chinese manufacturers integrate the entire safety loop within a single facility. At Sichuan Shield Technology:
- Component Fabrication: Proprietary high-precision die-cast aluminum alloy housings with anti-static powder coatings.
- PCB SMT Production: In-house surface-mount robotics with automated optical inspection (AOI) to eliminate solder bridging.
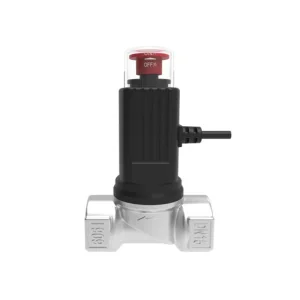
- Synchronized Isolation Valves: Co-engineering electromagnetic shut-off valves (JYFJS-011 series) ensures pulse current triggering matches detector drivers down to the millisecond.
Cost Efficiency & Agile OEM/ODM Scalability
The concentration of industrial sensor raw materials, microelectronics, and precision machining in China provides an unassailable bill-of-materials (BOM) advantage. Sichuan Shield Technology leverages this supply chain agility to offer international OEM partners:
- Rapid Prototyping: Custom enclosure modifications, proprietary communication protocols, and tailored multi-pin connectors within 15-20 business days.
- Automated Gas Chamber Testing: Multi-point zero/span calibrations performed within hermetic gas blending tunnels with strict traceability.
- Flexible Low-Volume Minimums: Tiered OEM licensing and brand customization starting at practical quantities for regional distributors.
Engineering Deployments Across Real-World Industrial Environments
Optimal mounting height, physical dispersion parameters, and automated fail-safe linkage architectures for localized hazard zones.
1. Commercial Kitchens & Boiler Rooms
Risk Profile: High humidity, vaporized grease, thermal shock, and constant vibrations from ventilation dampers.
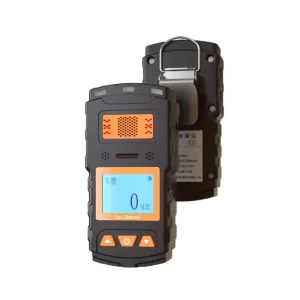
System Blueprint: Stand-alone wall-mounted detectors such as the SD2130 Series are installed 0.3m to 0.6m beneath the ceiling for methane (natural gas), or 0.3m above the floor plate for LPG. Built-in relay contacts directly trigger exhaust fans and activate a pipeline shut-off valve without needing an external PLC rack.
2. Petrochemical, Refineries & Storage
Risk Profile: Explosive hydrocarbons (methane, propane, benzene) plus deadly hydrogen sulfide (H₂S) byproduct pockets.
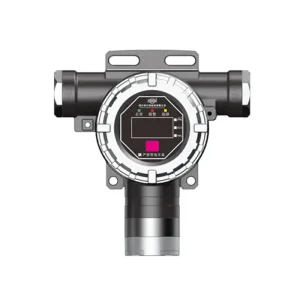
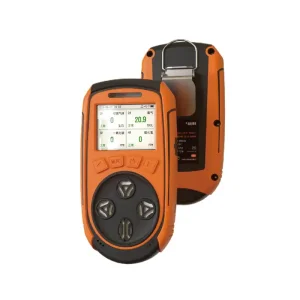
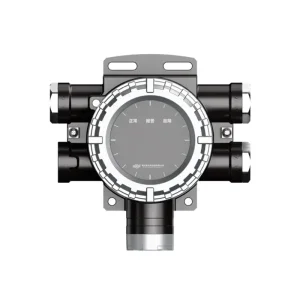
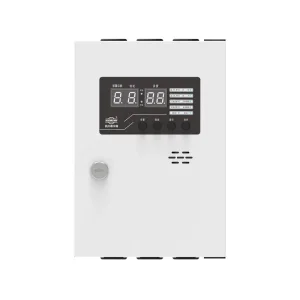
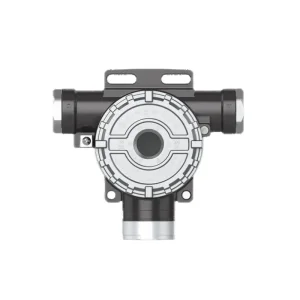
System Blueprint: Fixed explosion-proof point detectors (SD2100A / SD2100E Series) engineered inside Ex d IIC T6 Gb rated enclosures. Wired via multi-drop RS-485 Modbus or M-Bus loops back to central control room console (Shield 8001AB). Maintenance teams carry BTYQ-Z4 4-in-1 instruments for tank entry clearance.
3. Municipal Regulator Stations & Gas Gates
Risk Profile: High-pressure gas letdown junctions, micro-fissures in valve glands, and unattended equipment sheds.
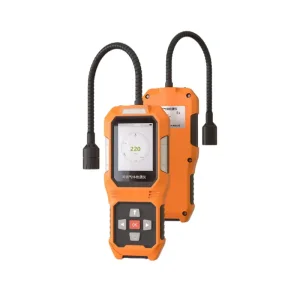
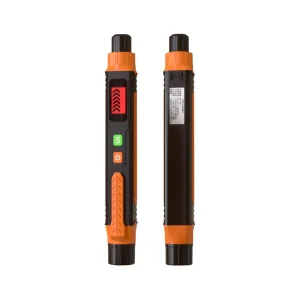
System Blueprint: Continuous wall-mounted point monitoring networked to SCADA RTUs with automated secondary battery backup. Mobile survey teams deploy pen-type JLY-50A and handheld JLY-CP100 sniffer sniffers to conduct weekly gland audits and detect subterranean pipeline seepage before pressure drops register.
Emerging Technological Trends in Gas Detection Instrumentation
A technical comparison of sensor physics, wireless telemetry protocols, and predictive lifecycle algorithms shaping modern safety infrastructure.
| Detection Technology | Target Gas Families | Core Strengths | Operational Limitations | Optimal Deployment |
|---|---|---|---|---|
| Catalytic Combustion (Pellistor) | Methane (CH₄), Propane, Butane, Hydrogen (H₂) | Linear 0-100% LEL response, budget-friendly replacement cost, mature industrial track record. | Susceptible to silicon, sulfur, and lead poisoning; requires oxygen (>10% VOL) to operate. | Commercial Kitchens / Boiler Rooms |
| Non-Dispersive Infrared (NDIR) | Hydrocarbons, CO₂, Refrigerants (R32, R410a) | Poison-immune, functions in inert (zero-O₂) atmospheres, long 5-10 year sensor lifespan. | Higher initial capital expenditure; cannot detect symmetric diatomic gases like Hydrogen (H₂). | Offshore Rigs / Refining Voids |
| Electrochemical Cells (EC) | Toxic Gases: CO, H₂S, NH₃, Cl₂, O₂ Deficiency | Extreme sub-ppm sensitivity, low power consumption, highly selective target calibration. | Electrolyte evaporation over time, temperature dependent, finite lifespan (24-36 months). | Chemical Plants / Wastewater Halls |
| MEMS Metal Oxide (MOS) | Volatile Organics, Methane, Refrigerant Micro-leaks | Miniature physical footprint, ultra-fast sub-second response, excellent sniffer integration. | Non-linear output requiring advanced MCU curve correction, cross-sensitive to ambient humidity. | Handheld Sniffers / Smart Home IoT |
IoT & Cloud Telemetry
Transitioning from isolated local bells to unified wireless telemetry. Modern wall detectors incorporate LoRaWAN, NB-IoT, and 4G industrial gateways, sending real-time concentration matrices to cloud dashboards. Plant engineers receive immediate instant SMS, webhook, and SCADA push alerts before field workers even perceive odorants.
Edge AI & Predictive Maintenance
On-board 32-bit ARM microprocessors analyze sensor baseline decay patterns in real time. Rather than waiting for total element failure during a mandatory annual inspection, the detector calculates remaining sensor life (RSL) and flags a predictive recalibration notice when catalytic baseline impedance drifts past safety limits.
Modular Sensor Cartridges
Eliminating hot-work permits during plant maintenance. Modern field point monitors (SD2100E Series) utilize factory pre-calibrated smart plug-in sensor cartridges. Onsite field technicians can swap out spent electrochemical or pellistor heads in under two minutes without declassifying the hazardous explosive zone.
Global Enterprise Procurement Checklist for Wall-Mounted Gas Detectors
Essential electrical, mechanical, and regulatory criteria for vetting overseas OEM/ODM manufacturing partners before issuing RFQs.
Key Mechanical & Electrical Specs
- Ingress Protection & Corrosion Resistance: Verify housing is die-cast aluminum alloy or 316 stainless steel with an IP65 or IP66 rating to prevent dust deposition and water jet ingress.
- Explosion-Proof Ratings: Ensure certificates match project hazardous boundaries: Ex d IIC T6 Gb for continuous Zone 1 explosive process areas, or Ex ia IIC T4 Ga for intrinsically safe field sensors.
- Signal Interfaces: Demand standardized 4-20mA 3-wire analog output alongside galvanically isolated RS-485 Modbus RTU or M-Bus interfaces for seamless DCS/SCADA handshake.
- Integrated Solid-State Relays: Verify independent dual passive contact relays (Low Alarm / High Alarm / Fault) rated at least 250VAC 3A or 30VDC 5A for direct fan and valve interlocks.
Supplier Factory Qualification Criteria
- R&D Longevity & Patent Portfolio: Review whether the supplier has independent IP (e.g., Sichuan Shield Technology’s 18+ years, 80+ commercialized models, and 40+ national patents).
- End-to-End Safety Chain Testing: Does the vendor design and manufacture their own gas alarm controllers (SD8001 series) and emergency solenoid shut-off valves (JYFJS-011)? Single-source suppliers eliminate finger-pointing during commissioning.
- Mandatory Production Certifications: Audit CCC (China Compulsory Certification) test reports, ISO9001/ISO14001 compliance, and third-party metrology verification certificates.
- Batch Consistency Verification: Inquire about automated aging burn-in cycles (72+ hours thermal cycling) and standardized span gas verification procedures.
Frequently Asked Questions: Wall-Mounted Gas Detection Systems
In-depth responses compiled by senior instrumentation engineers regarding alarm threshold calculation, installation physics, and fail-safe automation logic.
Q1: What is the exact scientific distinction between Lower Explosive Limit (%LEL) and Volume Percentage (%VOL)? +
Q2: What are the strict engineering guidelines for wall-mounting height based on target gas molecular weight? +
1. Lighter-Than-Air Gases (e.g., Methane CH₄ ≈ 16 g/mol, Hydrogen H₂ ≈ 2 g/mol, Ammonia NH₃ ≈ 17 g/mol): The detector must be installed high on the wall, approximately 0.3m to 0.6m below the ceiling, and within a 4m to 7.5m horizontal radius of potential leak sources (flanges, valves, manifolds). Avoid dead air pockets right at the ceiling apex corners.
2. Heavier-Than-Air Gases (e.g., LPG/Propane C₃H₈ ≈ 44 g/mol, Butane C₄H₁₀ ≈ 58 g/mol, Hydrogen Sulfide H₂S ≈ 34 g/mol): The detector must be wall-mounted low, approximately 0.3m to 0.6m above the finished floor level, and within 3m horizontal radius from potential emission sources, ensuring it is elevated sufficiently above floor washdown or dirt accumulation lines.
Q3: How does the emergency shut-off linkage operate between a wall detector and a solenoid valve? +
Q4: When should an enterprise deploy a Stand-Alone Point Detector versus a Bus-Networked Central Controller system? +
Specify Stand-Alone Detectors (e.g., SD2130 Series): Ideal for isolated zones, single-unit commercial kitchens, standalone boiler rooms, or decentralized paint spray booths. Stand-alone units feature local visual displays, audible sirens, and onboard dry contact relays to drive shut-off valves or exhaust dampers directly without incurring the cost of running long homerun cables back to a central control cabinet.
Specify Bus/Branch Networked Systems (e.g., SD2100A / SD2100E Detectors + SD8001A/B Controller): Mandated for expansive chemical complexes, multi-story buildings, municipal regulator gates, and large-scale industrial plants. In this architecture, up to dozens of wall-mounted field detectors communicate across a 2-wire or 4-wire M-Bus / RS-485 network back to an SD8001 gas alarm controller located in a safe, non-hazardous control room. The host console provides centralized datalogging, zone-by-zone matrix voting, fault supervision, and SCADA/BMS building management integration.
Q5: How frequently must wall-mounted gas detectors undergo calibration, and what is bump testing? +
Bump Testing (Functional Check): Exposing the sensor to a brief blast of certified span gas (above the AL1 threshold) to verify sensor cell response, visual/audible alarms, and relay activation. In mission-critical chemical environments, bump tests are conducted weekly or monthly.
Full Calibration (Zero and Span Adjustment): Zero calibration adjusts baseline electronic noise in clean air, followed by span gas calibration (e.g., introducing a certified 50% LEL balance-air mixture) to adjust amplifier gain curves. Industrial catalytic and electrochemical wall-mounted detectors should be calibrated every 3 to 6 months, while robust NDIR infrared optical detectors can maintain calibration for 6 to 12 months depending on ambient particulates and operating temperature extremes.
Q6: Can Sichuan Shield Technology accommodate OEM brand customization and bespoke communication protocols? +
Integrated Detection & Safety Control Catalog
Explore our extended series of point-type wall monitors, portable gas detectors, central supervision consoles, and automated shut-off hardware ready for volume export.