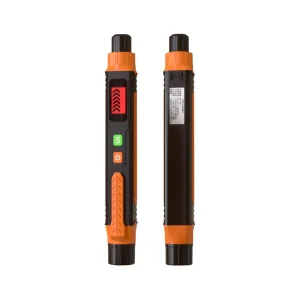
Primary Wholesale Gas Detection Instruments
Engineered for high-throughput reliability, certified hazardous-area safety compliance, and direct factory-level OEM/ODM customization.
Global CO2 & Combustible Gas Detection: Engineering White Paper
Analyzing structural shifts in natural refrigerant transitions (R744), stringent workplace occupational safety limits, and turnkey gas containment architecture.
The Global Phase-Down of HFCs & Transcritical CO2 (R744)
Driven by the Kigali Amendment to the Montreal Protocol, European F-Gas regulations (Regulation EU 2024/573), and the US EPA AIM Act, commercial refrigeration is undergoing a rapid transition toward natural refrigerants. Carbon Dioxide (R-744) has emerged as the premier non-flammable, zero-ODP, and ultra-low-GWP (GWP=1) working fluid for commercial supermarket racks, hypermarkets, and cold-storage distribution logistics.
However, transcritical CO2 systems operate at extreme pressures ranging from 75 to over 130 bar. Leaks in indoor mechanical machinery rooms, walk-in coolers, or manifold trenches pose rapid asphyxiation hazards without olfactory warning. Sichuan Shield Technology’s dedicated wholesale CO2 leak detection systems provide crucial real-time PPM and %VOL optical monitoring, ensuring immediate mechanical exhaust activation and automated emergency shut-off before toxic thresholds are breached.
- Compliant with ASHRAE Standard 15 and EN 378 safety specifications
- Multi-level audible-visual alarm outputs configured to 5,000 ppm (TWA) and 30,000 ppm (STEL)
- Factory integrated relay triggers for mechanical extractors and solenoid safety valves
Occupational Safety & Confined Space Mandates
Carbon dioxide is fundamentally heavier than ambient air (relative vapor density of ~1.52). Consequently, accidental release in beverage dispensing cellars, microbreweries, wineries, industrial carbon capture utilization and storage (CCUS) sites, and bio-fermentation tanks causes the gas to displace oxygen and pool in low-lying areas, pits, and floor trenches.
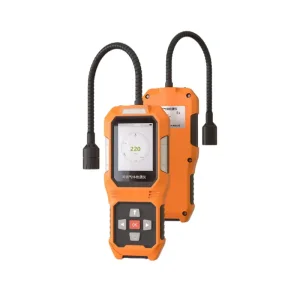
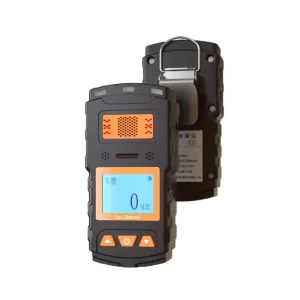
Occupational Health and Safety Administration (OSHA) and European directive standards stipulate an 8-hour Time-Weighted Average (TWA) Permissible Exposure Limit (PEL) of 5,000 ppm (0.5% VOL) and a Short-Term Exposure Limit (STEL) of 30,000 ppm (3.0% VOL). Concentrations exceeding 40,000 ppm pose Immediate Danger to Life or Health (IDLH). Fixed wall-mount point detectors and handheld leak sniffers engineered by Shield provide dual-channel sensing to prevent tragedy before personnel enter confined compartments.
- Continuous diffusion and pump-suction sampling modes
- Fast T90 response times below 15 seconds to mitigate acute hypoxic risks
- Robust IP65/IP66 enclosure ratings with anti-condensation heated optical cells
Localized Application Scenarios & System Integration
From commercial hospitality cellars to high-tech controlled environment agriculture, our sensor architectures deliver field-tailored performance.
Beverage Dispensing, Breweries & Cellars
Pressurized CO2 bulk cylinders, carbonators, and beverage draught lines inside fast-food restaurants, bars, and brewpubs are situated in enclosed, sub-ground storage. Undetected leaks saturate basements rapidly.
Shield provides split-architecture systems: an IP65 detector mounted 12 inches (30 cm) from the floor to monitor heavy gas pooling, wired directly to a remote audible-visual display unit installed at the entrance before staff enter.
Controlled Environment Agriculture (CEA)
Modern commercial greenhouses and vertical indoor farming operations inject CO2 up to 1,200–1,800 ppm to accelerate photosynthetic crop yield. However, delivery manifolds and burner faults can over-enrich spaces to toxic levels.
Our dual-channel NDIR transmitters deliver stable 4-20mA and RS-485 Modbus telemetry to climate computer controllers, automating enrichment dosing while maintaining worker safety overrides.
Industrial CCUS & Chemical Synthetics
Carbon Capture, Utilization, and Storage (CCUS) facilities, enhanced oil recovery (EOR), and dry ice manufacturing plants handle high-volume liquid and supercritical CO2. Infrastructure requires heavy explosion-proof certifications.
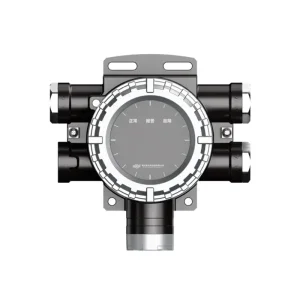
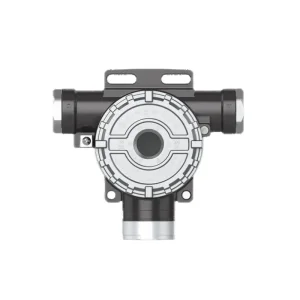
Shield manufactures cast-aluminum explosion-proof point detectors (SD2100 series) with Ex d IIC T6 Gb ratings, immune to airborne cross-contaminants, acid vapors, and extreme thermal cycling.
Sensor Physics: Dual-Beam NDIR vs. Alternative Methodologies
Evaluating optical absorption physics, cross-sensitivity risks, and total cost of ownership across industrial leak detection platforms.
| Evaluation Parameter | Dual-Beam NDIR (Shield Standard) | Photoacoustic Spectroscopy (PAS) | Electrochemical Sensing (Solid State) | Catalytic Bead / Pellistor |
|---|---|---|---|---|
| Operating Principle | Beer-Lambert Law optical absorption at 4.26 µm with active reference channel | Acoustic pressure pulse detection generated by modulated IR photon absorption | Electromotive force change through solid-state ion-conducting electrolyte | Thermal combustion of target gas on catalytically active ceramic bead |
| Target Specificity | Exceptional (Optical bandpass filter rejects hydrocarbons, NH3, CO, solvents) | High, but vulnerable to ambient sonic noise, mechanical vibration, and drafts | Moderate; subject to chemical cross-interference from acidic gases | Non-specific (Detects combustible hydrocarbons only, entirely blind to CO2) |
| Calibration Drift | Ultra-Low (<1% full scale per year via internal reference optical channel) | Low to moderate; acoustic microphone sensitivity drifts over temperature extremes | High drift; electrolyte dries out or saturates with continuous exposure | High drift caused by silicon, lead, or sulfur poisoning and sintered catalyst aging |
| Operating Lifespan | 10 to 15+ Years (Solid-state infrared emitter & detector) | 5 to 8 Years (Mechanical miniature microphone membranes degrade) | 1.5 to 3 Years (Chemical consumption requires frequent replacement) | 2 to 3 Years (Subject to baseline burn-off and catalytic poisoning) |
| Oxygen Dependency | Zero dependency (Functions perfectly in 100% N2, zero-oxygen, or inert purges) | Zero dependency on oxygen presence | Requires ambient atmospheric oxygen to sustain redox reaction | Mandatory requirement: minimum 10-15% ambient O2 to sustain combustion |
| Total Cost of Ownership | Lowest (Zero consumable chemistry, multi-year field stability) | Moderate (High initial equipment cost, moderate calibration overhead) | High (Frequent sensor module replacement, regular field span calibration) | High in harsh settings due to frequent sensor head burn-outs |
China Supply Chain Resilience & Chengdu High-Tech Efficiency
Combining vertically integrated component fabrication, high-volume automated SMT, and proprietary automated calibration chambers.
Vertically Integrated Ecosystem
Situated in the Southwest Airport Economic Development Zone of Chengdu, Sichuan Shield Technology operates a holistic manufacturing matrix. We control optical design, precision mold making, automated surface-mount SMT placement, enclosure casting, and final validation.
Unlike trading vendors who assemble disparate third-party modules, we fabricate both the detector telemetry electronics and the physical cast-aluminum emergency shut-off valves in-house, ensuring 100% interoperability and zero supply bottlenecks.
Multi-Stage Dynamic Gas Calibration
Every detector passing through our Chengdu facility is subjected to rigorous multi-point temperature and humidity compensation tests inside automated climate-controlled gas chambers. We utilize certified primary standard gas balances (NIST-traceable methane, CO, CO2, and H2S blends).
Sensors are thermally cycled from -40°C to +70°C to map individual digital polynomial curves into onboard EEPROM, preventing false alarms caused by seasonal thermal shifts in unconditioned refrigeration mechanical rooms.
Agile OEM/ODM White-Label Programs
We provide full-scope turnkey branding support for multi-national safety equipment brands, system integrators, and regional fire engineering distributors. From private-label industrial mold injection colors to customized firmware modbus register mapping, we accelerate time-to-market.
Our rapid prototyping facility can produce customized housing samples, custom laser-etched nameplates, bespoke bilingual packaging, and specialized relay trigger routines within 15–20 working days.
Technology Roadmap: The Future of Smart Gas Safety
Pioneering edge-computing diagnostics, self-correcting optical chambers, and long-range LPWAN wireless telemetry.
Dual-Beam Micro-Optics & Bus Topology
Complete deployment of high-stability dual-wavelength NDIR optical benches across all point-type models. Integration of 4-wire M-Bus / RS-485 digital architectures, allowing up to 128 field detectors to run on a single branch loop to the central SD8001 controller.
Edge-AI Drift Compensation & LoRaWAN
Integration of low-power machine-learning algorithms directly on the ARM Cortex microcontroller to analyze optical degradation and dust accumulation. Deployment of wireless LoRaWAN, NB-IoT, and Cat-M1 modules for remote utility pipeline and agrarian greenhouse telemetry.
Micro-Electro-Mechanical Systems (MEMS) & Self-Healing Systems
Transition toward miniaturized MEMS-based multi-gas optical spectrometers capable of simultaneously measuring CO2, combustible LEL, and refrigerant blends on a single chip. Development of autonomic shut-off manifolds with dynamic pressure-drop leak verification algorithms.
Global Compliance Standards & Engineering Support
Rigorous regulatory verification to guarantee frictionless market access across European, American, and Asia-Pacific jurisdictions.
International Statutory Compliance
Gas monitoring equipment deployed in commercial and industrial settings is governed by stringent performance criteria. Shield detectors and solenoid cut-off valves are engineered and validated according to international benchmarks:
- EN 378 & ASHRAE 15: Mandatory safety parameters for refrigerating systems and heat pumps utilizing R744 carbon dioxide.
- ATEX & IECEx (Ex d IIC T6 Gb): Certified flameproof construction for explosive atmosphere point detectors (petrochemical & gas infrastructure).
- China Compulsory Certification (3C / CCCF): Mandatory national certification for gas detection, fire alarm signaling, and emergency shut-off valves.
- EN 50270 & FCC Part 15: High-grade electromagnetic compatibility (EMC) testing ensuring high immunity against VFD drive interference and RF noise.
Localized Engineering & After-Sales Lifecycle
Selecting Shield as your wholesale manufacturing partner provides access to specialized field engineering expertise:
- Pre-Engineering Specification Support: Detailed wiring schematics, loop impedance calculations, and zone coverage advice for EPC engineering tenders.
- Comprehensive Documentation: Full English datasheets, 3D CAD step files, Modbus register manuals, and factory calibration certificates shipped with every batch.
- Rapid Replacement & Modular Spares: Hot-swappable, pre-calibrated smart sensor modules allow swift field maintenance without dismounting main field wiring.
Frequently Asked Questions (FAQ)
Comprehensive technical guidance for procurement directors, safety engineers, and HVAC-R system integrators.
1. What is the fundamental difference between Dual-Beam NDIR and single-beam CO2 sensors?
2. At what physical height should CO2 leak detectors be mounted in refrigeration rooms?
3. How does the gas detector interface with the JYFJS-011 emergency shut-off valve?
4. Can these gas detectors be deployed outdoors in sub-zero winter temperatures?
5. What communication protocols are supported for Building Management Systems (BMS)?
6. What is the minimum order quantity (MOQ) and production lead time for OEM orders?
Specialized Industrial & Portable Safety Instrumentation
Explore our extended series of point-type monitoring units, portable leak locators, and pen-type maintenance instruments.