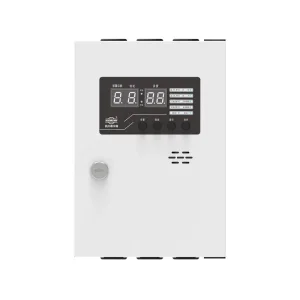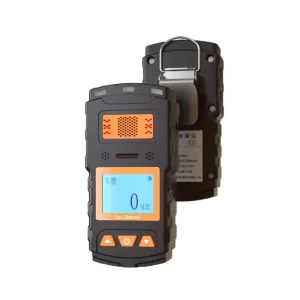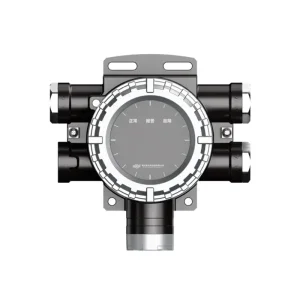
Featured Gas Safety & Monitoring Hardware
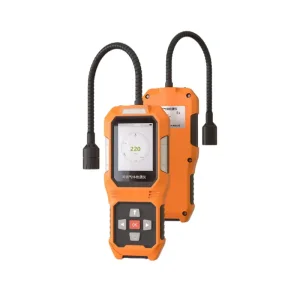
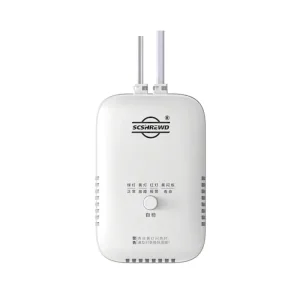
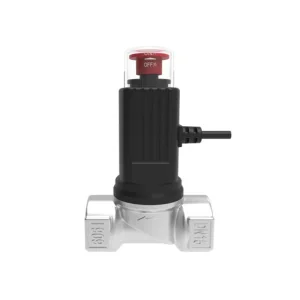
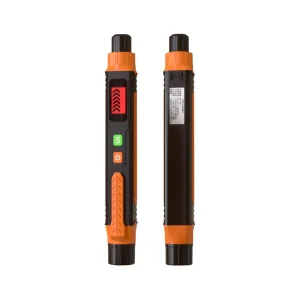
Explore precision-engineered portable detectors, fixed point-type industrial monitoring heads, smart controllers, and automatic electromagnetic emergency shut-off valves.
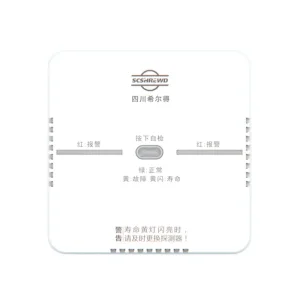
Industrial CO Alarm Engineering Architecture
A rigorous examination of core transducer chemistry, false-alarm mitigation algorithms, cross-sensitivity compensation, and fail-safe safety integrity levels (SIL).
Electrochemical Transducers & Chemical Specificity
Industrial carbon monoxide monitoring operates in extreme thermal and atmospheric environments where false positives lead to catastrophic plant shutdowns, and undetected leaks hazard human life. At Sichuan Shield Technology, our industrial CO detectors employ sealed, multi-electrode fuel-cell grade electrochemical sensing elements. By tracking the electrochemical oxidation of CO at a catalytic working electrode (producing CO₂ + 2H⁺ + 2e⁻) balanced against oxygen reduction at the counter electrode, our sensors generate an analog current strictly linear to toxic concentration from 0 to 1,000 ppm.
Cross-Interference Mitigation: Equipped with dual internal chemical filtration layers, our sensing heads effectively eliminate cross-sensitivity against ambient Hydrogen (H₂), Ethanol vapors, and Sulfur Dioxide (SO₂), adhering strictly to UL 2075 and EN 50545-1 specifications.
Embedded Firmware & Zero-Point Baseline Tracking
Zero-point drift caused by seasonal humidity shifts and ambient thermal variance has historically plagued electrochemical sensors. Shield Technology solves this via edge-embedded algorithmic temperature compensation using high-precision NTC thermistors soldered millimeters from the sensor reservoir. Our firmware continuously computes dynamic baseline corrections, preventing baseline sag in cold sub-surface utility tunnels and false tripping in high-heat commercial kitchens.
SIL2 System Integrity: Critical internal circuit loops perform continuous self-diagnostics—detecting open loops, sensor electrolyte depletion, output pin freezing, and supply voltage transients within 50 milliseconds.
| Transducer Architecture | Target Gas Range | T90 Dynamic Response | Thermal & Humidity Range | Typical Service Lifespan | Ideal Industrial Setting |
|---|---|---|---|---|---|
| Industrial 3-Electrode Electrochemical | 0 - 1000 ppm CO | < 25 seconds | -40°C to +65°C / 10%–95% RH | 5 - 7 Years (Ultra-life) | Boiler Rooms, Metallurgy, Tunnels |
| Dual-Beam NDIR Infrared Sensor | 0 - 100% Vol / % LEL (CO₂/CH₄) | < 20 seconds | -20°C to +60°C / Non-condensing | > 10 Years Continuous | Chemical Processing, Refineries |
| Poison-Resistant Catalytic Bead (Pellistor) | 0 - 100% LEL Combustible | < 15 seconds | -40°C to +70°C / High durability | 3 - 5 Years | Hazardous Class I Div 1 / Zone 1 |
| Smart Micro-Electromechanical (MEMS) | 0 - 500 ppm CO / VOCs | < 30 seconds | -10°C to +50°C / Commercial | 5 Years | Commercial Parking & Smart Building |
China Factory 4.0: Supply Chain Resilience & Quality Rigor
Inside our Chengdu manufacturing center: Automated SMT placement, robotic calibration gas manifolds, thermal aging stress-testing, and complete lot traceability.
Automated SMT & Dual-Layer Conformal Coating
Precision electronics demand zero human assembly contamination. Our production lines deploy fully automated Yamaha high-speed SMT machines capable of 0201 component mounting. Finished PCBA boards undergo automated optical inspection (AOI) followed by robotic three-proof conformal coating (anti-corrosion, anti-fungus, anti-moisture), indispensable for sulfurous petrochemical atmosphere survivability.
Dynamic Multi-Gas Automated Calibration Matrix
Unlike workshops relying on manual syringe injections, Shield operates computer-controlled mass flow controller (MFC) gas mixing chambers. Every batch of CO alarm devices is subjected to a 4-point calibration run (Zero, Low Alarm AL1, High Alarm AL2, Over-range Span) with standard NIST-traceable gases, writing customized calibration coefficients directly to on-board EEPROM memory.
100% High-Temperature & Electrical Burn-In
Infant mortality failure in industrial safety electronics is unacceptable. Every assembled unit undergoes a continuous 72-hour thermal stress screening at 55°C and 85% RH inside environmental chambers under power load. Surge immunity testing, electrostatic discharge (ESD) over ±8kV, and fast transient burst tests are verified prior to final laser marking and packing.
Macro-Industry Solutions: Deploying Integrated Detection Systems
Engineered to mitigate catastrophic risks across critical production verticals through linked detection, alarming, and emergency gas shutdown.
Metallurgical Plants & Blast Furnace Gas Ducts
Steel processing and smelting operations generate vast volumes of blast furnace gas rich in Carbon Monoxide (often exceeding 25% by volume). Leaks at flange connections, valves, and water seals pose immediate fatal risks. Shield supplies explosion-proof point-type detectors (such as our SD2100A/E series) linked over 4-20mA or RS485 Modbus directly to centralized SD8001 alarm consoles. Integrated dry contact relays instantly trip warning sirens, activate forced ventilation, and drive emergency valves.
Underground Utility Corridors & Municipal Tunnels
In modern urban infrastructure, combined pipelines house natural gas, electrical conduits, and telecommunication fiber inside confined tunnels. Poor air exchange causes rapid pooling of both combustible methane and toxic carbon monoxide. Our dual-channel and 4-in-1 diffusion systems provide 24/7 continuous telemetry back to municipal SCADA centers via 4G/NB-IoT or LoRaWAN, empowering field teams to execute zero-risk entries.
Industrial Boiler Rooms & Commercial Kitchens
Incomplete combustion from heavy-duty commercial burners generates silent CO accumulation alongside volatile natural gas leaks. Standalone units like the SD2130 paired with our JYFJS-011 aluminum alloy electromagnetic gas shut-off valve provide an airtight localized safety perimeter: detecting the leak, sounding an audible-visual 85dB alarm, and physically snapping the gas supply line shut within 1 second.
Underground Enclosed Parking & HVAC Energy Control
Automotive exhaust fumes in underground parking garages create lethal CO spikes. Rather than running massive exhaust ventilation fans 24/7—wasting tens of thousands of kilowatt-hours—building management systems rely on Shield industrial CO sensors communicating via BACnet/Modbus to throttle exhaust dampers dynamically, maintaining air purity below 25 ppm while slashing operational carbon footprints.
Technological Roadmap: The Next Era of Industrial Gas Intelligence
How Sichuan Shield is integrating AI-driven predictive drift modeling, ultra-low power wireless mesh topologies, and solid-state MEMS sensor arrays.
Edge AI & Predictive Sensor Health Modeling
Traditional alarms wait for toxic gas to reach a preset threshold. Our upcoming edge-AI firmware monitors the micro-slope of concentration curves ($dC/dt$). By correlating rate-of-rise metrics against historical airflow dynamics, the instrument flags fugitive micro-leaks days before catastrophic buildup occurs. Simultaneously, the system computes sensor internal impedance, predicting electrolyte end-of-life 6 months in advance.
Self-Powered Wireless Mesh (LoRaWAN & NB-IoT)
Trenching explosion-proof conduit in established refineries can exceed $150 per meter. Shield is pioneering intrinsically safe battery-powered detectors utilizing LoRaWAN mesh and NB-IoT protocols. Operating on high-energy lithium thionyl chloride (Li-SOCl₂) batteries paired with micro-power wake-sleep algorithms, these sensors achieve 5-year uninterrupted field life without requiring a single wired cable.
Solid-State MEMS Multi-Gas Fusion Arrays
Next-generation industrial alarms will transcend single-target monitoring. By consolidating Carbon Monoxide, Methane, Hydrogen, and volatile organic compounds (VOCs) onto a single silicon MEMS die smaller than a fingernail, Shield is developing multi-gas fusion hardware that slashes device dimensions by 60% while exponentially expanding industrial hazard discernment.
Global Regulatory Compliance & Localized Engineering Support
Bridging Chinese manufacturing velocity with North American and European regulatory certifications for smooth import and compliance authorization.
International Safety Norms: UL, EN, ATEX & SIL2
Navigating international cross-border compliance demands meticulous engineering documentation. Sichuan Shield manufactures products under an ISO 9001 and ISO 14001 accredited quality management system, and our hardware platforms comply with key global life-safety standards:
- UL 2034 & UL 2075: Time-weighted response thresholds (e.g., 70 ppm within 60–240 mins, 150 ppm within 10–50 mins, 400 ppm within 4–15 mins) with false-alarm immunity against typical solvent exposures.
- EN 50291 & EN 50545-1: Demanding performance criteria for domestic and commercial garage toxic gas apparatus, specifying rigid calibration stability and digital communication bus logging.
- ATEX & IECEx Certification: Ex d IIC T6 Gb flameproof enclosures and Ex ia IIC T4 Ga intrinsic safety designs for continuous operation inside Zone 1 and Zone 2 explosive environments.
- Mandatory 3C (CCC) & Fire Protection Approval: Chinese national compulsory certification validating electrical explosion safety and municipal gas safety compliance.
Turnkey Localized Support for Global Distributors
A partnership with Shield extends far beyond purchasing hardware. We equip distributors, EPC contractors, and brand owners with complete engineering collateral to streamline local regulatory filings, bidding, and commissioning:
- Custom Firmware Protocols: Tailored register maps for Modbus RTU, BACnet MSTP, 4-20mA current loop calibrations, and cloud MQTT payloads conforming to your local SCADA architecture.
- Bilingual Technical Documentation: Comprehensive architectural CAD wiring schematics, white-label user manuals, exploded assembly diagrams, and test inspection sheets.
- Full Lifecycle Support: Rapid provision of factory calibration replacement sensor modules, warranty turnaround within 48 hours, and dedicated online engineering support.
Global B2B Procurement: OEM/ODM Engineering Framework
Accelerating time-to-market through our proven 5-stage New Product Introduction (NPI) workflow, flexible MOQ requirements, and white-label manufacturing.
1. Structural Tooling & Industrial ID
Whether modifying our existing IP66/IP67 cast aluminum enclosures or building custom flame-retardant ABS housings, our in-house mold tooling shop delivers 3D rapid SLA prototypes in 5 business days and production steel injection tooling within 30 days.
2. Custom Firmware & UI Branding
Inject your brand identity directly into bootup LCD screens, private labeled high-contrast front facings, silk-screened metal chassis, and customized alarm threshold configurations. We support multi-language voice alarm prompts (English, Spanish, Arabic, Russian).
3. Production Velocity & Logistics Buffer
Benefit from predictable lead times: 2-3 weeks for standard recurring OEM production batches. For Tier-1 distributors with scheduled rollouts, Shield maintains raw material safety stock (sensors, microcontrollers, cast housings) to guarantee rapid replenishment and zero pipeline disruption.
Technical FAQ: Industrial Gas Detection & Procurement
In-depth engineering answers addressing installation physics, calibration standards, false-trip prevention, and system integration.
Q1 What is the precise mounting height for Carbon Monoxide vs. Methane vs. LPG detectors?
Mounting height is governed strictly by the molecular vapor density relative to ambient air (Air = 1.0). Carbon Monoxide has a molar mass of 28.01 g/mol, making it marginally lighter than air (28.97 g/mol) with roughly neutral buoyancy; industrial CO detectors should be installed at breathing height (1.5 to 1.8 meters above the floor), or near suspected combustion sources. Methane (natural gas, ~16 g/mol) is significantly lighter than air and demands mounting 30 cm below the ceiling. LPG (propane/butane, >44 g/mol) is heavy and pools in low spots, requiring mounting 30 cm above the finished floor.
Q2 How does Shield eliminate false alarms caused by cleaning agents, paints, or alcohol vapors?
Low-grade electrochemical and semiconductor sensors frequently cross-react with ethanol, isopropanol, or paint solvents. Shield industrial CO alarms integrate a mechanical and chemical charcoal filter layer directly on top of the sensor diffusion barrier. This filter adsorbs heavy hydrocarbon and alcohol molecules while permitting small CO molecules to pass unobstructed, preventing nuisance alarms and unnecessary facility shutdowns.
Q3 What is the recommended calibration and bump test schedule for industrial gas alarms?
OSHA and international best practices recommend routine bump testing before each daily work shift for portable personal safety detectors (e.g., BTYQ-Z4, JLY-CP100) to confirm sensor response and alarm functionality. For fixed point-type industrial detectors (SD2100A/E), full calibration with certified reference span gas should be performed every 6 to 12 months, depending on atmospheric dust, humidity, and trace chemical exposure.
Q4 Can your fixed detectors operate stand-alone without an expensive central alarm controller?
Yes. The SD2130 series is specifically engineered for standalone industrial and commercial utility. It incorporates local audible and visual strobe lights along with built-in high-capacity relay dry contacts (normally open / normally closed). When a gas leak or CO hazard exceeds the setpoint, the detector autonomously drives external exhaust fans, rings external horn strobes, and cuts the JYFJS-011 emergency solenoid valve without requiring an external control panel.
Q5 How does the JYFJS-011 solenoid emergency shut-off valve ensure safety after an incident?
The JYFJS-011 electromagnetic shut-off valve is engineered with a fail-safe mechanical latch mechanism. Upon receiving a momentary pulse signal (DC 9V–24V) from the gas detector, fire panel, or emergency stop push-button, the solenoid trips and snaps the valve closed in under 1 second. To prevent dangerous gas repressurization before pipeline integrity is verified, the valve cannot be opened electrically; it requires authorized personnel to physically inspect the premises and manually pull the reset knob.
Q6 What communication architectures are supported for large-scale industrial integration?
Shield supports three principal industrial telemetry topologies: standard 4-20mA analog current loops with HART protocol compatibility; digital 4-wire RS485 Modbus RTU facilitating multi-drop daisy chaining over 1,200 meters to our SD8001 series controllers; and non-polarity two-wire power-bus systems that dramatically reduce field wiring complexity and labor costs during municipal retrofits.
Complete Industrial & Residential Gas Instrumentation Series
Explore our complete commercial and municipal safety catalog. Select a product below to access full datasheets, wiring schematics, and private-label customization options.