Household Series
Direct manufacturer supply for international procurement programs, safety audits, and customized firmware requirements.
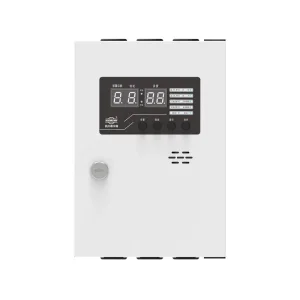
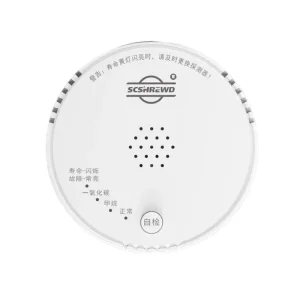
Critical considerations for professional sourcing directors, safety supply chains, and large-scale utility infrastructure.
In the global life-safety equipment industry, selecting an OEM Carbon Monoxide Detector and Alarm supplier involves stringent scrutiny beyond mere unit cost. Carbon monoxide (CO)—often characterized as the "silent killer"—is colorless, odorless, and tasteless. When incomplete combustion occurs in fossil-fuel heating units, commercial boilers, underground parking facilities, or metallurgical furnaces, undetected accumulation rapidly leads to debilitating intoxication or catastrophic workplace fatalities. Consequently, tier-one international importers, gas utilities, and systems integrators demand that OEM manufacturing partners deliver verified sensor consistency, deep standard harmonization (such as UL 2034, EN 50291, and NFPA 720), and low total lifecycle cost.
Modern corporate supply chains face acute geopolitical, logistical, and technological transitions. In Europe and the United Kingdom, statutory regulations mandate the inclusion of dedicated CO warning devices in any residential or commercial tenancy that houses fuel-burning installations. In North America, the International Building Code (IBC) and NFPA regulations enforce centralized monitoring architectures with secondary power redundancy and interconnected signaling. To serve these markets without friction, an established manufacturing factory must maintain vertical control over every tier of assembly: starting from raw electrode preparation and ASIC signal filtering, through surface mount technology (SMT) fabrication, to final gas-mixture testing within automated environmental wind tunnels.
Strategic Procurement Takeaway: Tier-one OEM suppliers do not merely assemble prefabricated components. True manufacturers perform automated calibration against certified balance gas mixtures, embed microprocessor-level anti-interference routines, and supply complete traceability records with every serial number batch.
Electrochemical cells formulated with high-purity catalytic electrodes prevent zero-baseline drift and guarantee sustained accuracy over 5 to 10 years of operational service.
Advanced digital filtering discriminates carbon monoxide from household and commercial background gases like ethanol, hydrogen sulfide, cooking vapours, and cleaning solvents.
Every PCBA runs through optical AOI inspection, automated gas exposure chambers, and functional verification, logging full telemetry for total buyer peace of mind.
Customized sensor packaging, environmental enclosures, and relay topologies engineered for specialized enterprise risks.
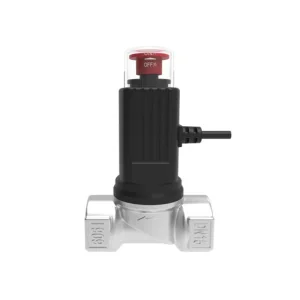
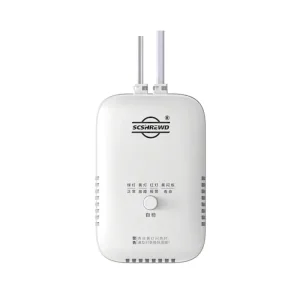
In centralized domestic housing, modern energy conservation strategies result in airtight building envelopes. A faulty water heater or compromised heating flue can induce lethal CO buildup in bedrooms within minutes. Shield's OEM residential portfolio incorporates low-profile ceiling or wall mount designs, sealed 10-year lithium power reserves, and direct 12V pulse outputs capable of driving solenoid shut-off valves (such as the JYFJS-011 series) to instantly sever the fuel supply line upon alarm verification.
Integrated interconnectivity options (wired 4-wire bus, 868MHz / 915MHz RF wireless mesh, and Zigbee/Tuya smart protocols) empower property management firms to centralize residential status feeds while delivering loud >85dB local acoustic warning for rapid resident evacuation.
Underground parking structures, bus interchanges, and vehicle logistics hubs face intermittent surges of toxic emissions from idling internal combustion motors. Operating massive ventilation extraction arrays 24/7 incurs excessive, unsustainable power expenditure. Shield delivers fixed point-type industrial detectors (like the SD2100E and SD2130 series) equipped with calibrated 0–300ppm or 0–500ppm electrochemical transducers.
Equipped with standard 4-20mA current loops and RS485 Modbus RTU communications, these detectors integrate seamlessly into Building Automation Systems (BAS) and variable frequency drives (VFDs). Ventilation fans activate only when concentrations breach safe thresholds (e.g., 25ppm or 35ppm), slashing electrical usage by up to 60% while strictly complying with OSHA and international air quality codes.
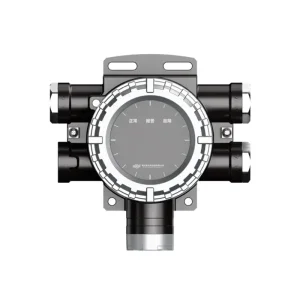
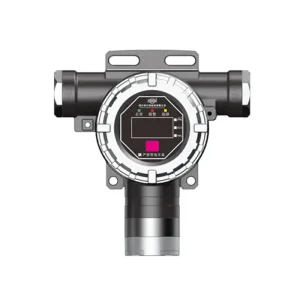
Heavy processing plants, industrial gas kilns, metallurgical smelting lines, and commercial boiler rooms present volatile thermal extremes, mechanical vibrations, and airborne contaminants. In these harsher environments, Shield's explosion-proof casting housings (rated Ex d IIC T6 Gb and IP66) protect the precision sensor core against environmental moisture, acid mist, and mechanical shock.
Interfacing directly with our centralized SD8001A/B multi-channel gas alarm controllers placed in safe engineering control rooms, the installation provides real-time digital monitoring, programmable dual-stage alarm dry contacts, audible-visual strobes, and automated failsafe emergency plant shutdown linkages.
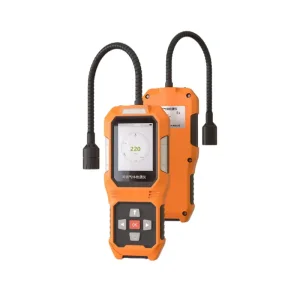
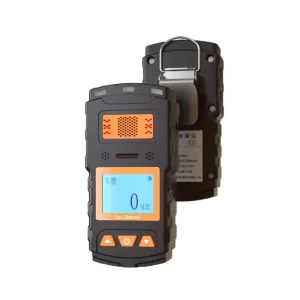
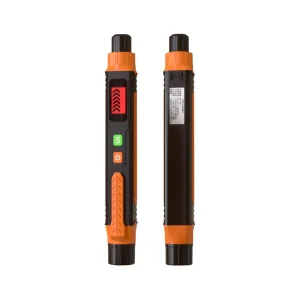
Underground utility tunnels, petrochemical inspection pits, and sewer maintenance routes require lightweight, intrinsically safe, personal monitoring tools. Technicians carrying the JLY-50A portable sniffer pen or the BTYQ-Z4 4-in-1 multi-gas instrument can verify zero-hazard conditions prior to ingress.
Shield's portable diagnostics feature immediate tactile vibration alarms, ultra-bright 360-degree LED indicators, and ultra-fast diffusion response times. These personal instruments safeguard field maintenance crews against unseen carbon monoxide pockets and explosive gas mixtures before workers step inside confined environments.
A rigorous breakdown comparing OEM device parameters across global industrial and residential certification benchmarks.
Unlike combustible hydrocarbon gases that are indexed as percentages of their Lower Explosive Limit (%LEL), toxic carbon monoxide monitoring is universally registered in parts-per-million (PPM) or converted milligrams per cubic meter (mg/m³). Human toxicological reaction to carbon monoxide correlates directly with Carboxyhemoglobin (COHb) saturation curves in the bloodstream. Consequently, regulatory bodies do not mandate instantaneous trip switches for low concentrations; instead, they prescribe strict Time-Weighted Average (TWA) multi-tier exposure algorithms to avoid false alarms while ensuring immediate trip responses during lethal surges.
| Evaluation Parameter | EN 50291 (European / UK Standard) | UL 2034 (North American Standard) | Shield OEM Industrial Spec |
|---|---|---|---|
| 30 PPM Exposure | No alarm prior to 120 minutes | No alarm prior to 30 days continuous | Programmable telemetry threshold |
| 50 PPM Exposure | Alarm response within 60–90 min | Alarm response within 60–240 min | High accuracy display; opt. low alarm |
| 100 PPM Exposure | Alarm response within 10–40 min | Alarm response within 10–50 min | Standard AL1 Trip Point (Factory default) |
| 300 PPM Exposure | Alarm triggered in < 3 minutes | Alarm triggered in < 3 minutes | Instant emergency cut-off < 15 seconds |
| Sensor Architecture | Electrochemical Cell with Acid/Neutral Gel | Electrochemical or Biomimetic Cell | Industrial Multi-Electrode Electrochemical |
| Relay & Linkage Output | Optional or Dry-contact relay output | Wired interconnect or dry contacts | Active 12V Pulse + SPDT 250VAC/5A Relay |
| Operating Temperature | -10°C to +40°C | 4.4°C to 37.8°C (Standard Residential) | -30°C to +60°C (Extended Extreme Range) |
| Factory Traceability | Batch testing records required | Quarterly factory production audits | 100% individual calibration logs retained |
For industrial procurement engineers specifying products like our SD2100A, SD2100E, and SD2130 series, sensor lifespan, temperature compensation, and moisture resistance remain paramount. Electrochemical carbon monoxide sensors function via chemical oxidation: CO molecules diffuse through a porous gas-permeable membrane into an electrolyte solution, generating a micro-amperage current proportional to gas concentration between working, counter, and reference electrodes. Low-grade sensors suffer from evaporation or electrode degradation when subjected to dry winter heating or tropical summer humidity. Shield solves this engineering bottleneck by implementing hermetically sealed electrolyte reservoirs, proprietary anti-drying gel matrices, and on-board dual NTC thermistor micro-compensators that correct readouts across wide temperature fluctuations.
A closer look inside Sichuan Shield Technology's modern production lines, cleanrooms, and testing facilities in Chengdu, China.
High-speed Yamaha surface-mount placement lines ensure zero lead-bridging, tight solder meniscus control, and precise placement of high-impedance low-noise operational amplifiers.
Units travel through specialized continuous gas calibration tunnels flooded with certified 50PPM, 100PPM, and 300PPM balance air to permanently program digital coefficient tables.
High-temperature burn-in chambers, humidity freeze tests, drop shock stations, and rigorous EMC immunity testing ensure long-term stability in adverse global regions.
Anticipating next-generation market requirements with proactive R&D engineering and forward-compatible hardware platforms.
The worldwide transition toward decarbonized domestic heating and industrial power is altering fuel dynamics. Across the UK, Europe, and Asia-Pacific, municipal gas distribution utilities are actively pilot-testing hydrogen blending (H2 blends from 5% to 20% into municipal natural gas infrastructure). This introduces a major challenge: classical electrochemical carbon monoxide sensors can experience catalytic cross-sensitivity when unburned hydrogen is present during incomplete combustion events, potentially triggering false alarms.
To maintain market leadership, Shield's OEM engineering roadmap integrates proprietary dual-sensor hybrid matrices. By pairing selective NDIR (Non-Dispersive Infrared) or solid-state thermal conductivity sensors with high-selectivity filtered electrochemical cells, next-generation Shield OEM devices simultaneously monitor volatile gas leaks and toxic CO without mutual cross-interference.
Native integration of low-power wireless chipsets supporting Matter, Thread, NB-IoT, and LoRaWAN. Enables multi-family properties and smart utilities to track battery life and device health without manual field visits.
Embedded microcontroller algorithms analyze electrolyte impedance in real time. Rather than waiting for complete sensor failure, the system alerts facility engineers when cell sensitivity degrades below 80%.
Patented secondary microphone feedback chips verify the physical sound output of the 85dB piezoelectric buzzer on scheduled cycles, guaranteeing life-safety compliance in tenant dwellings.
A streamlined workflow designed to accelerate your private-label time-to-market with minimized technical risk.
Custom exterior aesthetics, injection mold tooling, color matching, and bespoke bracket architectures to match brand identities.
Custom calibration thresholds, multilingual LCD visual interfaces, custom Modbus register mappings, and regional LED blink sequences.
Dedicated engineering support assisting clients through regional laboratory testing at BSI, UL, TÜV, and Intertek for accelerated approvals.
Bilingual technical documentation, SDK integration assistance for controllers, and batch warranty guarantees backed by 18+ years of R&D.
In-depth responses to frequent engineering inquiries regarding gas sensor chemistry, integration topologies, and factory protocols.
Electrochemical sensors operate on a chemical fuel-cell oxidation process that generates an electrical current directly proportional to carbon monoxide concentration. They are characterized by outstanding accuracy down to 1 PPM, exceptionally low quiescent power consumption (ideal for 10-year battery powered devices), and high selectivity against common interferents.
Metal-Oxide Semiconductor (MOS) sensors require continuous heating of a metal tin-dioxide (SnO2) substrate to several hundred degrees Celsius. This consumes substantial electrical current (necessitating AC power) and exhibits broad cross-sensitivity to volatile organic compounds (VOCs), alcohols, and fluctuating relative humidity. Consequently, for reliable life-safety CO compliance across residential and industrial settings, professional OEM buyers mandate electrochemical sensors.
This is dictated by the physiological hazard profile of the target gases:
Yes. Direct hardware linkage is a cornerstone of Shield's unified safety ecosystem. Our standalone detectors—including the household SD6200 and SD6101 series and commercial SD2130 series—contain dedicated output circuitry providing a high-amperage 12V pulse or a form-C dry-contact relay.
When a validated alarm threshold is breached, the detector trips the JYFJS-011 aluminum alloy electromagnetic solenoid shut-off valve within <1 second. The valve features a manual-reset mechanical latch, guaranteeing that the gas supply line remains hermetically sealed until a qualified technician inspects the premises and manually resets the plunger.
Shield's commercial and industrial instruments (including the SD2100A, SD2100E, and SD8001A/B supervisory controllers) support both 4-20mA analog three-wire current loops and non-polar two-wire / four-wire digital RS-485 Modbus RTU communication topologies.
Digital RS-485 allows up to 128 point detectors to be multi-dropped over a single shielded twisted pair line extending up to 1,200 meters. This dramatically reduces copper cabling costs, delivers live decimal concentration telemetry, and provides individual diagnostic fault flags (sensor dirty, zero drift, open loop) directly to the central control panel or building SCADA system.
For standard custom branding (laser-engraved logo, customized user manuals, localized label ratings, and custom master carton artwork), our baseline MOQ starts at 500 to 1,000 units per model platform.
Lead times for initial prototype validation typically take 2 to 3 weeks, followed by full production batch turnaround within 25 to 35 business days. For deep ODM engagements involving custom industrial exterior tooling, customized injection molds, and dedicated firmware protocols, initial tooling requires 45 to 60 calendar days with comprehensive DFM (Design for Manufacturing) validation.
Complete safety hardware portfolio for closed-loop gas isolation, municipal surveys, and facility protection.