High-Precision Detection Instrumentation Series (Part I)
Direct manufacturing solutions covering portable sniffing pens, smart combustible point sensors, and ATEX/SIL2 compliant industrial safety systems.
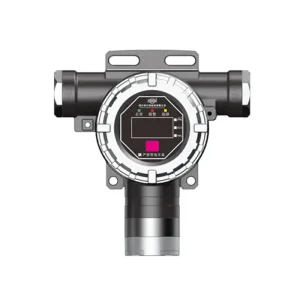
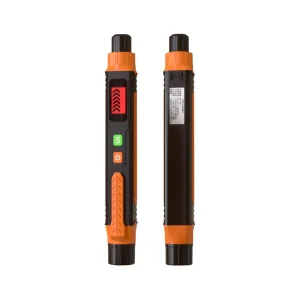
Advanced Principles of Combustible Gas Detection: LEL, NDIR & Catalytic Sensing
In modern industrial process engineering, the reliable detection of flammable hydrocarbons, methane (CH₄), liquefied petroleum gas (LPG), propane (C₃H₈), and hydrogen (H₂) is vital to preventing catastrophic deflagration and atmospheric hazards. A high-performance portable combustible gas detector monitors ambient air concentration relative to the Lower Explosive Limit (LEL)—the lowest concentration of gas or vapor capable of producing a flash of fire in presence of an ignition source.
Combustible gas monitoring does not operate on arbitrary parts-per-million (ppm) scales when personal safety thresholds are approached; rather, it computes hazardous saturation percentages where 100% LEL corresponds directly to the volumetric stoichiometric threshold (e.g., approximately 5.0% Vol for Methane, 2.1% Vol for Propane, and 4.0% Vol for Hydrogen). Engineering an industrial portable detector demands uncompromising fidelity in sensor chamber fluid mechanics, temperature-humidity drift compensation, and micro-power catalytic or optical architectures.
Pellistor (Catalytic Bead) Sensors
Utilizing a matched pair of active and reference platinum wire micro-coils embedded in alumina pellets. The active bead catalyzes oxidation, inducing a temperature variance that shifts resistance across a Wheatstone bridge. Optimal for broad-spectrum combustible gas detection from 0 to 100% LEL with rugged resistance to environmental shifts.
Non-Dispersive Infrared (NDIR)
Optical absorption technique targeting specific vibrational-rotational hydrocarbon absorption bands (typically 3.3 to 3.4 μm). Immune to chemical poisoning (silicones, lead, sulfides) and operates effectively in oxygen-deficient or inert atmospheres where catalytic oxidation fails to trigger, making it essential for closed vessels and purge lines.
Electrochemical & MOX Sensor Fusion
For sub-LEL ultra-trace leak pinpointing (ppm range) and toxic co-monitoring. Advanced Micro-Electro-Mechanical Systems (MEMS) metal oxide sensors provide instantaneous sniffing response times (<2 seconds) along pipe flanges, micro-valves, and structural joints during routine pre-commissioning.
| Detection Technology | Typical Measuring Range | Response Time (T90) | Oxygen Requirement | Poisoning Susceptibility | Target Gas Selectivity |
|---|---|---|---|---|---|
| Catalytic Bead (Pellistor) | 0–100% LEL | < 15 seconds | Requires >10% O₂ Vol | Susceptible to Silicones & H₂S | Broad Flammable Spectrum |
| Dual-Beam NDIR (Infrared) | 0–100% LEL / 0–100% Vol | < 20 seconds | Zero Oxygen Needed (0% O₂) | Immune to Chemical Poisons | Hydrocarbon Selective (No H₂) |
| MEMS Semiconductor (MOX) | 10–10,000 ppm / Trace | < 3 seconds | Ambient Required | Moderate (Degrades with volatile solvents) | General Hydrocarbons & Volatiles |
| Miniature Photoionization (PID) | 0.1–5,000 ppm (VOCs) | < 2 seconds | Ambient Independent | Lens Contamination Factor | VOCs with IP < Lamp eV |
Why Tier-1 Global Gas Safety Brands Rely on China ODM Factories
Exploring the vertical integration, rigorous metrological standards, and rapid prototype-to-production cycles that define Chengdu and Sichuan's high-tech instrumentation hubs.
Vertical Supply Chain Depth
From proprietary tooling and die-casting to cleanroom SMT chip placement, printed circuit assembly, and precision injection of anti-static explosion-proof ABS/polycarbonate enclosures, our production ecosystem eliminates tier delays.
Cost Engineering & Scalability
Direct factory procurement yields massive BOM (Bill of Materials) efficiencies, providing distributors with 30-45% higher operating margins while maintaining strict compliance with IEC 60079 and EN 60079 explosion protection.
Full ODM Turnkey Flexibility
Custom industrial ID design, bespoke LCD/OLED user interfaces, custom alarm parameters, language localization (EN, ES, FR, AR, RU), private-label mold customization, and firmware modifications completed in weeks, not quarters.
Rigid Quality Verification
Full compliance with ISO 9001:2015, mandatory China 3C (CCC) certifications, continuous multi-chamber dynamic gas blending tunnels, automated burn-in stress testing, and real-time environmental chamber validation (-40°C to +70°C).
End-to-End ODM Manufacturing Methodology
Requirement & Ex Architecture
Target gas matrix selection (CH₄, C₃H₈, H₂), Ex-proof design classification (Ex d ia IIC T4 Gb), casing ergonomics, and regulatory boundary scoping.
Electronic & Optical Prototyping
Schematic capture, multi-layer PCB routing with intrinsically safe galvanic isolation barriers, 3D rapid resin molding, and firmware sensor drift testing.
Tooling & Pilot Calibration
Hardened steel injection tooling, gas exposure chamber validation, baseline zero/span curve calibration, and drop/vibration/ingress (IP66/67) testing.
Mass Production & Compliance
Cleanroom robotic SMT assembly, automated span gas calibration tunnels, explosion-proof batch sampling, custom silkscreen branding, and worldwide shipping.
Emerging Industry Trends in Combustible Gas Detection for 2026–2030
The transition from isolated analog instrumentation to interconnected, cloud-aware, and predictive personal safety infrastructure.
IoT Telemetry & Wireless Mesh
Integration of low-power wide-area networks (NB-IoT, LoRaWAN) and Bluetooth Low Energy (BLE 5.3) allowing portable detectors to beam real-time coordinates, atmospheric data, and man-down alarms directly to the centralized control center dashboard.
AI-Powered Drift Mitigation
Machine learning routines running on low-power 32-bit ARM Cortex MCUs that continuously analyze temperature, ambient humidity, and baseline noise to eliminate false positive alarms caused by background atmospheric humidity spikes or pressure swings.
Ultralow-Power Optical MEMS
Micro-machined nondispersive infrared platforms operating on sub-milliamp current budgets. Enables multi-month continuous operational battery longevity on portable instruments without nightly recharge cycles, transforming turnaround operations.
High-Risk Operational Environments & Safety Compliance
Targeted safety engineering workflows tailored for hazardous classifications, confined utility spaces, and macro-industrial sectors.
Petrochemical & Refinery Turnarounds
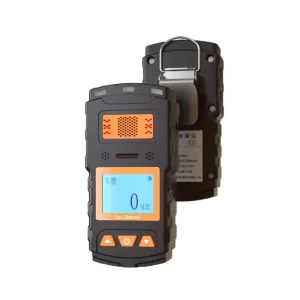
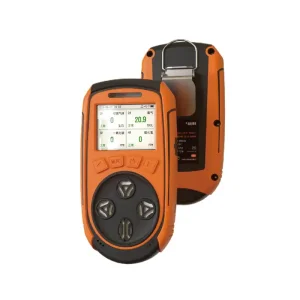
During plant turnarounds and hot work operations, volatile hydrocarbon vapor pockets pose catastrophic ignition risks. Operators utilize our intrinsically safe 4-in-1 portable gas detectors (LEL, O₂, H₂S, CO) for continuous air monitoring prior to hot work permit validation and inside hydrocracker containment zones.
Underground Utility & City Gas Corridors
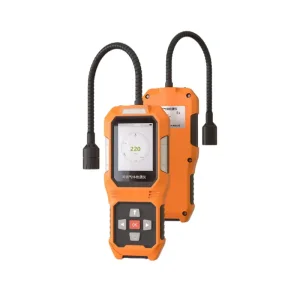
Gas distribution authorities require rapid sniffing pens (like the JLY-50A) and diffusion survey instruments to patrol subterranean valve chambers, flange couplings, and buried transit pipelines. Immediate acoustic-optic pulsing allows operators to pinpoint minute leaks before hazardous underground vapor pockets form.
Commercial Kitchens & Boiler Infrastructure
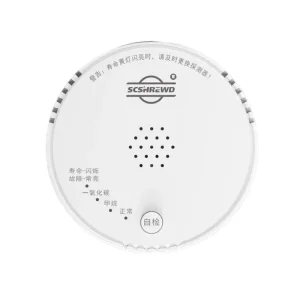
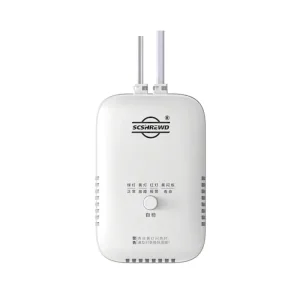
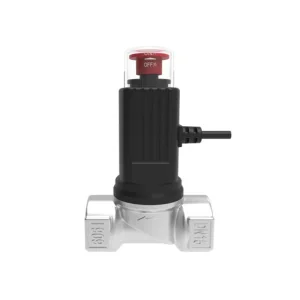
Commercial culinary operations and boiler facilities face risks from natural gas and liquefied petroleum gas (LPG) accumulation. Standalone point detectors paired with electromagnetic shut-off valves (such as the JYFJS-011) guarantee immediate physical pipeline isolation the instant 10% or 25% LEL thresholds are breached.
Confined Space Safety Compliance (OSHA 1910.146): Entering industrial storage vessels, utility sewer shafts, silo tanks, or ballast holds requires strict stratified testing. Combustible hydrocarbon gases may rise (Methane, lighter than air at vapor density ~0.55) or sink into sump pits (LPG/Propane at vapor density ~1.55). Our multi-gas portables feature high-flow internal motorized sampling micro-pumps with telescopic anti-static probes, enabling operators to profile atmospheric stratification at 1-meter intervals prior to physical man entry.
Macro Industrial Solutions: Interlinked Gas Safety Systems
Bridging the gap between personal portable instruments, fixed industrial point detectors, central telemetry controllers, and mechanical shut-off automation.
Gas Alarm Controllers (SD8001 Series)
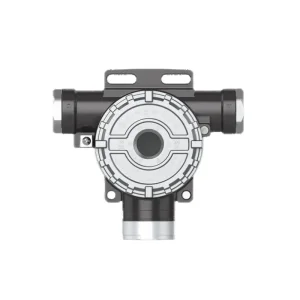
Centralized monitoring units residing in safe zone control rooms. Capable of multi-channel M-Bus / RS485 Modbus RTU communication with fixed field transmitters (SD2100E/SD2100A), displaying continuous real-time gas saturation levels, event logging, and zone-specific relay switching.
SCADA & Cloud Telemetry Bridging
Transmitting isolated gas alarms across building management systems (BMS) and distributed control networks (DCS) via 4-20mA analog loops, HART protocols, and wireless gateways. Facilitates plant-wide safety interlocks, automated sirens, and immediate evacuation protocols.
Emergency Isolation Valves (JYFJS-011)
Heavy-duty, precision machined aluminum alloy electromagnetic shut-off valves. Triggered within 50 milliseconds via micro-pulse signals upon high-level alarm trip. Features manual mechanical reset to guarantee gas flow cannot resume until the hazard has been verified cleared by certified engineers.
Global Procurement Demands: Engineering Specifications & RFP Compliance
Critical verification checkpoints for procurement managers, distributors, and safety engineers when qualifying combustible gas detector factories.
Ex-Proof Certification
Mandatory certification for explosive atmospheres: ATEX (Zone 0, 1, 2), IECEx, and China Ex standards (GB 3836.1/2/4). Intrinsically safe protection (Ex ia IIC T4) ensures electronic circuitry cannot ignite flammable gas mixtures under normal or fault conditions.
Ingress Protection (IP66/67)
Field instruments operate under severe deluge, marine salt spray, desert dust storms, and heavy rain. Double injection-molded elastomer seals protect internal sensors and circuit components from catastrophic fluid and particulate ingress.
Calibration Traceability
Verify that the factory utilizes National Institute of Metrology (NIM) certified calibration gases with fully automated span-test reporting, providing individual calibration certificates traceable by equipment serial number.
After-Sales & Sensor Replacement
Evaluate factory support for pre-calibrated smart plug-and-play sensor replacement modules, field bump test stations, and available spare parts inventories to minimize lifetime cost of ownership (TCO).
High-Precision Detection Instrumentation Series (Part II)
Complete product spectrum including residential natural gas alarms, handheld survey monitors, industrial point sensors, and emergency solenoid shut-off valves.
Technical Q&A: Combustible Gas Detection & ODM Manufacturing
Expert answers addressing calibration frequencies, cross-sensitivities, explosion protection ratings, and OEM lifecycle customization.
Q What is the operational distinction between % LEL, % VOL, and PPM when monitoring combustible gases?
PPM (Parts Per Million) measures microscopic gas concentrations, predominantly used for toxic monitoring or early trace-leak surveying. % LEL (Lower Explosive Limit) tracks atmospheric explosibility. For methane, 100% LEL is approximately 5.0% by volume. A reading of 20% LEL indicates the air contains 1.0% methane by volume (20% of the explosion point). % VOL (Percent Volume) measures pure volumetric saturation up to 100% gas content, typical for inert gas blanket monitoring and pipeline purge validation where oxygen is depleted.
Q How does catalytic bead sensor poisoning occur, and how do Shield portable instruments defend against it?
Catalytic pellistors oxidize flammable gases on an active coated bead. Exposure to volatile silicones (found in lubricants and sealants), tetraethyl lead, sulfur compounds, and chlorinated hydrocarbons forms an impermeable glassy layer over the platinum/alumina surface, permanently diminishing sensitivity (sensor poisoning). Shield portable detectors utilize dual-stage sintered stainless-steel flame arrestors and proprietary chemical filter matrices that absorb silicone and heavy contaminants before vapors enter the combustion chamber.
Q What are the standard calibration intervals and bump-testing protocols for industrial portable gas detectors?
International safety standards (including OSHA and EN 60079-29-2) mandate a bump test (functional challenge test) before each day’s use. This exposes the instrument to a known gas concentration to verify sensor response and audible/visual alarm activation without adjusting calibration. Full span calibration is recommended every 90 to 180 days using traceable calibration gas standards to adjust electronic amplification and correct for natural baseline drift.
Q Why must natural gas (Methane) and LPG (Propane/Butane) detectors be mounted at fundamentally different heights?
Mounting position depends entirely on relative vapor density compared to air (air = 1.0). Natural gas is predominantly methane (relative density ~0.55), meaning it is lighter than air and rises rapidly toward ceilings; detectors must be mounted 30 cm below the ceiling near potential leak sources. Conversely, liquefied petroleum gas (LPG) consists of propane and butane (relative densities ~1.55 to 2.0), making it significantly heavier than air. LPG sinks to the floor and accumulates in low pockets; detectors must be placed 30 cm above the finished floor level.
Q What are the minimum order quantities (MOQ) and timeline milestones for custom ODM portable detector projects?
Our standard ODM engagement features a tiered structure: Private-label silkscreening, customized packaging, and localized menu firmware typically require an MOQ of 200–500 units with a 3-week fulfillment timeline. Full mechanical redesigns involving custom mold tooling, bespoke housing ergonomics, and proprietary circuit architecture start at an MOQ of 1,000–2,000 units, moving from 3D CAD sign-off to functional tooling and pilot production within 60 to 90 days.
Q How does an interlinked solenoid shut-off valve (such as the JYFJS-011) operate alongside point gas detectors?
The JYFJS-011 is a normally open, electromagnetic pulse-actuated shut-off valve. When a connected gas detector (e.g., SD6200 household or SD2130 industrial) reaches its pre-configured alarm threshold (typically 10% to 25% LEL), the detector's internal relay discharges a DC 9V–12V pulse to the valve coil. Within 50 milliseconds, a spring-assisted mechanical seal snaps shut, isolating the gas line immediately. The valve requires manual pull-pin reset, preventing accidental gas resumption until a technician inspects the pipeline and verifies that all atmospheric readings have normalized.