Industrial / Commercial
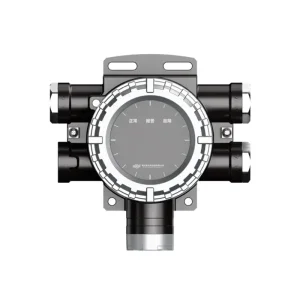
Industrial and Commercial Gas Detector SD2130 Series - Real-Time Detection
Explore Technical Specs
Continuous gas-hazard mitigation through high-accuracy sensing nodes, standalone controllers, and fail-safe electromagnetic isolation valves.
Mitigating toxic inhalation risks and optimizing indoor environmental quality (IEQ) requires uncompromising sensor chemistry, robust micro-electromechanical systems (MEMS), and deterministic fail-safe response loops.
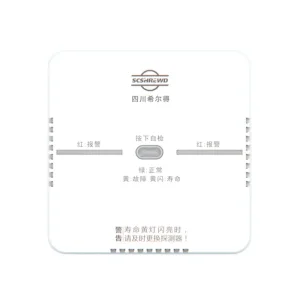
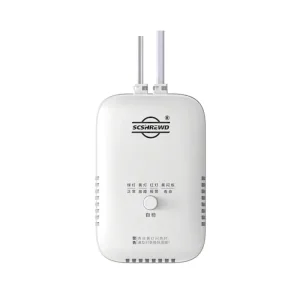
Our ODM CO detector platforms deploy three-electrode potentiostatic amperometric sensors. When Carbon Monoxide diffuses across a porous hydrophobic PTFE membrane, oxidation occurs at the working sensing electrode ($CO + H_2O \rightarrow CO_2 + 2H^+ + 2e^-$), generating a direct linear nanoampere current proportional to PPM concentrations. Integrated software-level temperature and humidity drift algorithms eliminate seasonal false positives in compliance with EN 50291 and UL 2034 specifications.
For Carbon Dioxide detection ranging from 400 PPM baseline ambient to 50,000 PPM industrial limits, Shield utilizes dual-channel NDIR optical benches. Incorporating a 4.26 μm narrow bandpass interference filter matched strictly to the molecular resonance of the $CO_2$ asymmetric stretch vibration, the secondary reference channel automatically offsets thermal emitter aging, dust settling, and optical mirror degradation for unmatched zero-drift baseline stability over a 15-year lifecycle.
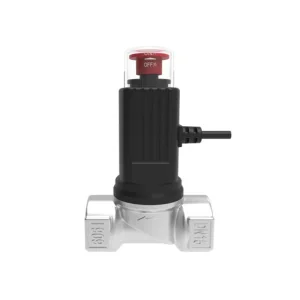
Detection without instantaneous physical containment leaves properties vulnerable. As an integrated manufacturer of both gas detection instrumentation and aluminum alloy electromagnetic shut-off valves (JYFJS-011 series), Shield provides a hardware-level linkage. Upon trip threshold attainment, an ultra-fast high-energy capacitive discharge activates the solenoid valve within 1 second, maintaining mechanical seal until manual field verification occurs.
| Target Gas & Sensor Topology | Typical Measurement Range | T90 Response Time | Cross-Interference Mitigation | Primary Industrial Standards |
|---|---|---|---|---|
| CO (Electrochemical 3-Electrode) | 0 – 1,000 PPM (Res: 1 PPM) | < 30 seconds | Chemical filter for $SO_x$, $NO_x$, alcohol scrubbing | EN 50291 / UL 2034 |
| CO2 (Dual-Beam NDIR Optical) | 400 – 5,000 / 10,000 PPM | < 20 seconds (diffusion) | Spectral isolation at 4.26 μm; immune to humidity | ASHRAE 62.1 / Title 24 |
| Combustible Gas (Catalytic Bead) | 0 – 100% LEL ($CH_4$, LPG) | < 10 seconds | Anti-poisoning silicone barrier coating | EN 60079-29-1 / GB 15322 |
| Combustible Gas (Industrial NDIR) | 0 – 100% VOL / LEL Hydrocarbons | < 12 seconds | Zero oxygen requirement, immune to hydrogen sulfide | IECEx / ATEX Zone 1 & 2 |
Bridging the gap between legacy analog detection and future autonomous edge ecosystems through solid-state sensing, acoustic metrology, and multi-protocol IoT intelligence.
Shield’s R&D center in Chengdu is actively qualifying sub-miniature Photoacoustic Spectroscopy (PAS) sensors for $CO_2$. By converting infrared absorption pulses directly into acoustic micro-barometric waves measured by high-SNR silicon microphones, our next-gen modules reduce optical chamber volume by over 75% while achieving true ppb-level resolution, allowing seamless mechanical packaging into standard gang-boxes and flush ceiling architectures.
Moving beyond simple hard-threshold alarms, our embedded ARM Cortex-M4 architectures run real-time rate-of-rise ($dC/dt$) and multi-parameter sensor fusion algorithms. By correlating VOC spikes, relative humidity shifts, and temperature gradients alongside raw CO/CO2 measurements, the system reliably filters out transient kitchen fumes or cosmetic spray aerosols, drastically cutting false dispatch rates for smart-city utility fleets.
Recognizing the transformation of modern Building Management Systems (BMS), Shield’s ODM platforms support modular plug-and-play communication daughterboards. Whether your industrial pipeline mandates Modbus RTU (RS-485) and 4-20mA current loop outputs or your residential IoT smart home requires LoRaWAN, NB-IoT, Zigbee 3.0, or Matter over Thread, our hardware accommodates universal field bus protocols.
Field-proven gas monitoring topologies designed to resolve specific environmental challenges, thermal stratification risks, and strict life-safety compliance codes across global enterprises.
High-density educational institutions, commercial towers, and smart hospitals deploy Shield’s duct-mount and room-type NDIR $CO_2$ transducers to automate fresh air damper intake. Aligned with ASHRAE Standard 62.1 and Title 24, our systems provide continuous PPM telemetry to minimize cooling energy consumption by up to 35% without risking cognitive impairment or sick building syndrome (SBS).
Automotive exhaust accumulation poses deadly acute CO risks combined with $NO_2$ combustion hazards. In accordance with EN 50545-1 standards, our industrial bus detectors (such as the SD2100E and GTY-SD2130 series) orchestrate multi-zone staged ventilation fans, triggering low-speed extraction at 30 PPM CO and full-throttle emergency exhaust with audio-visual evacuation alarms at 100 PPM.
Photosynthetic optimization in commercial indoor ag-tech requires tight Carbon Dioxide enrichment (typically maintained between 800 and 1,500 PPM). Shield’s IP65-rated agricultural gas sensors withstand high humidity condensation, sulfur evaporation cycles, and daily washdown protocols, driving direct $CO_2$ generator or liquid gas dosing solenoid linkages.
As natural refrigerants transition toward $CO_2$ (R744) to meet global F-gas phase-out mandates, catastrophic leak detection becomes a mandatory occupational safety issue. Operating down to -40°C, Shield’s specialized low-temperature NDIR detectors guard cellar lines, carbonation facilities, and brewery storage spaces against rapid asphyxiation hazards.
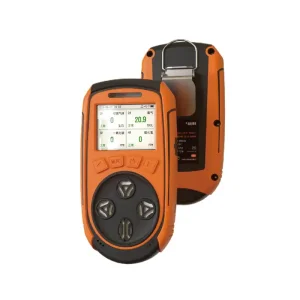
Entering chemical reaction chambers, utility vaults, and sewer shafts requires strict multi-gas validation. The BTYQ-Z4 portable 4-in-1 monitor delivers real-time diffusion or pump-suction analysis of combustible gases (%LEL), Oxygen ($O_2$), Hydrogen Sulfide ($H_2S$), and Carbon Monoxide (CO), ensuring worker safety with intrinsically safe (Ex ia IIC T4 Ga) certifications.
Centralized hydronic heating systems, gas water heaters, and enclosed kitchen spaces represent persistent risks of incomplete combustion. Deploying Shield SD6200 and SD6101 series residential detectors paired with emergency pipeline shut-off valves gives housing authorities and private real estate managers centralized multi-unit gas monitoring with automatic line isolation.
Headquartered within the Southwest Airport Economic Development Zone in Chengdu, Sichuan Shield Technology operates a high-precision manufacturing complex designed for high-yield throughput, automated calibration, and vertical component control.
Shield's dust-controlled cleanroom assembly floor utilizes fully automated high-speed Panasonic and Yamaha SMT placement lines capable of 01005 passives and fine-pitch BGA mounting. Every manufactured board undergoes 100% inline 3D Automated Optical Inspection (AOI) followed by In-Circuit Testing (ICT) and conformal coating to protect sensitive gas-sensing electronics against moisture, sulfurization, and aggressive chemical environments.
Gas sensor reliability depends on rigorous metrological calibration. Rather than relying on manual batch sampling, Shield runs custom robotic multi-point calibration arrays. Mass flow controllers (MFCs) inject certified balance air, standard Carbon Monoxide calibration gases, and precision $CO_2$ mixtures across dynamic thermal profiles (-20°C to +55°C). Calibration curves and zero-offset baselines are automatically flashed directly into each sensor’s EEPROM.
From industrial concept to white-box global shipping, Shield’s ODM engineering framework reduces commercialization risk and accelerates regional compliance milestones for international brand owners.
Defining measurement ranges, operating environments, mechanical enclosure constraints (IP ratings, hazardous area classifications), and target unit economics to establish product architecture.
Developing 3D industrial designs, aerodynamic gas-inflow acoustic simulation, mold flow optimization, and custom injection tooling for fire-retardant (UL94-V0) ABS/PC plastics or explosion-proof die-cast aluminum.
Tailoring alarm trip levels, latching versus self-resetting parameters, custom Modbus registers, multi-color LED status indicators, and proprietary cloud-ready IoT communication stacks.
In-house EMC chamber testing, climatic chamber aging, mechanical drop/vibration stress analysis, and poisonous cross-gas exposure tests to ensure first-pass certification success at accredited third-party labs.
Fabricating dedicated Bed-of-Nails functional testers, laser serialization systems, and automated gas verification jigs to lock down yield metrics before authorizing high-volume serial assembly.
Complete custom artwork printing, user manual translation, retail blister packaging or bulk industrial master cartons, and drop-ship logistics coordination to regional distribution hubs.
Mitigate regulatory liability and accelerate regional market access. Shield engineers manufacture products compliant with North American, European, and Asian life-safety directives.
Our residential CO alarm algorithms mirror the biological carboxyhemoglobin (COHb) accumulation curve. Firmware precisely handles time-weighted alarm conditions: 50 PPM for 60–90 minutes, 100 PPM for 10–40 minutes, and 300 PPM within 3 minutes, protecting occupants while avoiding false alarms from brief cooking exhaust transients.
For heavy petrochemical installations, gas compressor stations, and bulk solvent handling, Shield point detectors utilize rugged flameproof enclosures certified Ex d IIC T6 Gb. Flame arrestors on optical and catalytic sensor inlets prevent internal sparks from igniting external volatile atmospheres, with ingress ratings up to IP66/IP67.
All factory production runs operate under audited ISO 9001 and ISO 14001 Quality Management Systems. Shield holds China Compulsory Certification (3C/CCC) for gas safety instrumentation, CE-EMC compliance for European commercial integration, and guarantees full lead-free, non-toxic material compliance across all plastic and metal substrates.
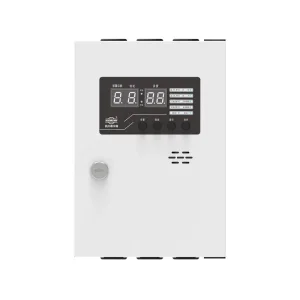
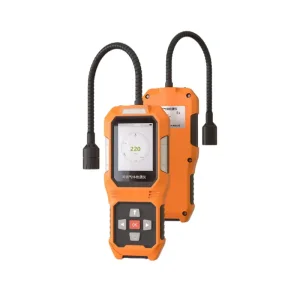
Complete the field ecosystem with central multi-channel supervisory controllers, rapid-action shut-off valves, and intrinsically safe portable survey detectors.
Detailed engineering answers covering sensor drift characteristics, calibration protocols, safety valve linkage parameters, and minimum order requirements.