Integrated LPG Detection & Emergency Mitigation Array
Precision-engineered combustible gas monitoring instruments, bus-type controllers, and certified shut-off valves deployed worldwide across residential and industrial infrastructures.
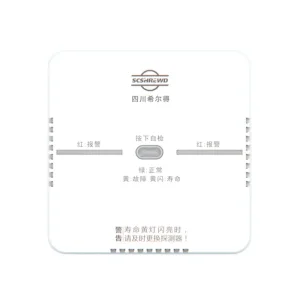
The Macro Evolution of Industrial LPG Safety Architecture
Liquefied Petroleum Gas (LPG)—predominantly composed of propane (C₃H₈), butane (C₄H₁₀), or varying volumetric blends—remains an indispensable clean primary fuel across global residential complexes, commercial culinary centers, and heavy process manufacturing. However, its thermophysical properties present severe combustible safety challenges that diverge fundamentally from methane-dominated Compressed Natural Gas (CNG).
Unlike natural gas, which is lighter than air and naturally diffuses upward, LPG vapor possesses a relative density ranging between 1.52 to 2.00 times heavier than ambient air. Consequently, fugitive releases do not dissipate quickly; they gravitate toward grade level, sinking into floor conduits, utility sumps, elevator shafts, and cellar voids.
Modern industrial safety engineering requires transitioning away from reactive warning bells toward automated, closed-loop mitigation chains. Sourcing certified LPG gas detection systems from established Original Equipment Manufacturers (OEM) ensures seamless interoperability across sensory edge nodes, central processing annunciators, and rapid-acting mechanical shut-off valves.
| Physical Parameter | Commercial Propane | Commercial Butane | Natural Gas (Methane) |
|---|---|---|---|
| Chemical Formula | C₃H₈ | C₄H₁₀ | CH₄ |
| Vapor Density (Air = 1.0) | 1.52 (Sinks) | 2.01 (Sinks) | 0.55 (Rises) |
| Lower Explosive Limit (LEL) | 2.1% Vol (100% LEL) | 1.8% Vol (100% LEL) | 5.0% Vol (100% LEL) |
| Upper Explosive Limit (UEL) | 9.5% Vol | 8.4% Vol | 15.0% Vol |
| Mandatory Sensor Elevation | 0.1m - 0.3m from Floor | 0.1m - 0.3m from Floor | 0.1m - 0.3m from Ceiling |
| Primary Failure Risk | Trench pool accumulation | Low-lying puddle boiling | Ceiling pocket trapping |
Localized Engineering Application Scenarios & Field Topology
Tailoring sensing kinetics, explosion-proof barriers, and hardware enclosures to the unique environmental stresses of mission-critical commercial and industrial zones.
Commercial Kitchens & Food Hospitality
Commercial culinary venues operate under heavy airborne grease, water vapor humidity, high thermal cycling, and constant surfactant cleaning. Catalytic sensors deployed here require hydrophobic fluoropolymer sinter filters and anti-poisoning catalysts to resist silicone washouts.
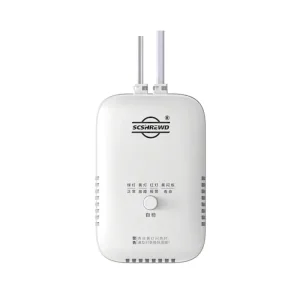
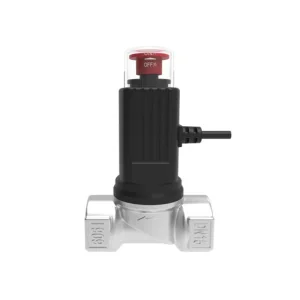
Topology: The standalone SD2130 Series mounted 20cm above the floor, directly wired to a rapid JYFJS-011 Solenoid Valve, guarantees instantaneous localized line isolation without requiring complex supervisory cabling.
LPG Cylinder Storage & Filling Depots
Bulk gas terminals and automated carousel filling plants represent Zone 1 / Class I, Division 1 hazardous environments. Constant mechanical handling of 12kg–50kg steel cylinders poses frequent micro-leak hazards from degraded valve stem O-rings and pigtail couplings.
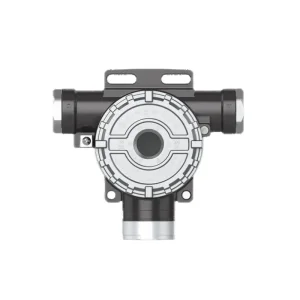
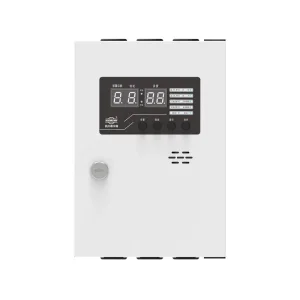
Topology: Continuous fixed flameproof point detectors such as the SD2100A/E Series with stainless housings, interconnected via RS485 Modbus RTU or intelligent 2-wire bus to an explosion-proof multi-channel Shield 8001AB Controller in the central control facility.
Industrial Kilns, Furnaces & Boilers
Manufacturing facilities utilizing LPG vaporizers for high-BTU heat treatment, ceramic kilns, and metallurgical annealing require massive flow conduits operating at elevated line pressures. Transient flameout or ignition delays create explosive gas accumulation in combustion chambers.
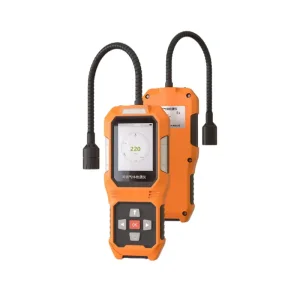
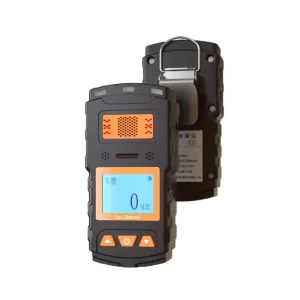
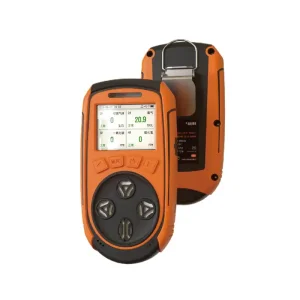
Topology: Multi-tiered monitoring pairing high-temperature point sensing at burner manifolds with portable survey teams equipped with the JLY-CP100 and BTYQ-Z4 for pre-entry hot-work permitting and confined space maintenance.
Municipal Underground Valve Pits & Sumps
Buried piping networks and district LPG vapor delivery pipelines are susceptible to ground shifting, soil compaction, and joint stress cracking. Leaked LPG migrates into municipal drainage conduits and telecom wireways.
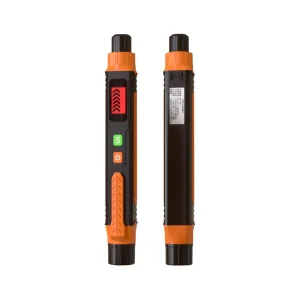
Topology: Regular field inspections with the high-sensitivity pen-type JLY-50A coupled with continuous submersible diffusion heads rated IP67/IP68 connected to centralized supervisory telemetry networks.
Technological Roadmap: From Pellistor Catalysis to MEMS-AI Optical Sensing
Analyzing sensing kinetics, life-cycle drift compensation, and the transition toward wireless autonomous safety telemetry.
The Next Decade of LPG Sensing Kinetics
Historically, catalytic pellistors (Wheatstone bridge combustion beads) have served as the undisputed workhorse for LPG detection. While robust and cost-effective, classic pellistors are vulnerable to chemical poisoning by sulfurous odorants (mercaptans), silicones, and chlorinated compounds, while consuming significant heating power (typically 120–150 mA at 3V).
Shield Technology’s R&D facility in Chengdu has spearheaded three architectural leaps to circumvent these historical bottlenecks:
- MEMS Catalytic Nanostructures: Integrating sub-micron platinum heating spirals on ceramic micro-hotplates reduces operating power consumption by over 75% while dramatically accelerating T90 response times down to under 8 seconds.
- Dual-Wavelength NDIR Optical Sockets: For severe industrial zones with zero oxygen or high H₂S presence, Shield leverages Non-Dispersive Infrared sensors tuned to the fundamental C-H vibrational stretch at 3.3μm to 3.4μm. Optical sensing cannot be poisoned, is failsafe, and guarantees 10+ years of operational stability.
- Edge-Computing AI Drift Algorithms: Embedded ARM Cortex microcontrollers continuously sample ambient temperature, absolute humidity, and long-term base resistance, utilizing polynomial matrix regression to virtually eliminate seasonal baseline drift and nuisance false alarms.
Intelligent Wireless IoT Integration
Industrial facility retrofit costs are heavily dominated by armored conduit, ATEX-rated cable glands, and hazardous-area trenching. The newest Shield telemetry modules integrate low-power NB-IoT, LoRaWAN, and Zigbee Pro mesh radios. Battery-assisted wireless LPG edge nodes run autonomously for up to 5 years, transmitting real-time concentration telemetry and battery health directly to SCADA or cloud dashboards.
SIL-2 / SIL-3 Functional Safety Compliance
For chemical refiners and bulk ship offloading manifolds, risk reduction demands strict adherence to IEC 61508 / IEC 61511. Shield's industrial detectors incorporate internal dual-channel redundant ADCs, continuous microprocessor watchdog routines, and self-testing sensor impedance checks to ensure safe failure states and verified high Safe Failure Fraction (SFF) ratings.
China Factory Supply Chain Resilience & Production Scale
How Sichuan Shield Technology leverages Chengdu’s advanced electronics manufacturing ecosystem to deliver unmatched OEM/ODM speed, cost leadership, and uncompromising quality assurance.
Vertical In-House Integration
Unlike assembly-only vendors, Shield operates a fully integrated manufacturing pipeline spanning die-casting aluminum tooling, CNC explosion-proof enclosure machining, high-speed SMT surface mounting, and automated conformal coating lines. Eliminating third-party reliance slashes lead times by 40%.
Automated Wind Tunnel Calibration
Every single sensor element undergoes rigorous multi-point span and zero calibration within computerized gas wind tunnels. Exposing detectors to certified NIST-traceable propane/butane balance-air test gases guarantees precision sensitivity curves and zero field false-trigger rates.
Severe Environmental Stress Aging
To eliminate early-life field mortality, all assembled circuit boards and finished detectors complete 72-hour burn-in stress testing in high-temperature, high-humidity climatic chambers (-40°C to +70°C at 95% RH) accompanied by intense multi-axis vibration testing.
Agile OEM & ODM Customization
Backed by over 40 patents and a 30-member specialized R&D engineering division, Shield supports global distributor private labeling, custom firmware protocol integration (BACnet, HART, Modbus), localized language displays, and bespoke mechanical enclosures with low MOQ barriers.
Global Regulatory Standards & Closed-Loop Isolation Architecture
Achieving fail-safe performance through certified ATEX/IECEx hazardous area compliance and instantaneous electromagnetic line shut-off linkage.
The Anatomy of an Unbroken Safety Chain
Audible alarms alone cannot avert catastrophe when leaks occur during unattended night shifts, in noisy mechanical boiler rooms, or when occupants succumb to asphyxiation. True industrial life-safety is strictly contingent upon a 100% autonomous closed-loop architecture:
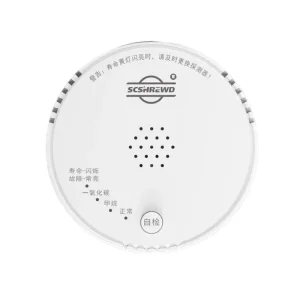
- Continuous Detection: Fixed point sensors (SD2100A/E) or household nodes (SD6200) sample ambient atmosphere continuously.
- Multi-Stage Threshold Tripping: Reaching Low Alarm (typ. 10%–20% LEL) triggers local audible/visual flashers and starts mechanical exhaust blowers to purge accumulating gas.
- High Alarm Emergency Cut-Off: Breaching High Alarm (typ. 25%–50% LEL) sends an instantaneous millisecond electrical impulse to the JYFJS-011 Solenoid Valve.
- Positive Mechanical Interlock: The valve snaps shut under internal spring force and permanent magnetic retention, hermetically isolating upstream LPG line pressure.
- Mandatory Manual Reset: The valve cannot reopen electronically. An authorized technician must personally inspect the facility, verify zero gas concentration, resolve the leak source, and manually pull the mechanical reset knob.
International Regulatory Harmonization
Shield LPG detection systems and electromagnetic valves are engineered to comply with demanding international standards:
High-Integrity LPG Shut-Off Valves & Portable Safety Instruments
Complementing fixed installations with rapid-response aluminum alloy emergency valves and field-proven diagnostic multi-gas portables.
Engineering FAQ for Global LPG Procurement Directors & EPC Engineers
Definitive technical insights into sensor physics, calibration intervals, mounting geometry, and system integration.