Gas Alarm Controller Shield 8001AB Series
Supervises up to 64 addressable gas sensing channels. Built-in programmable high/low relays, Modbus RTU/BACnet bridge, and fail-safe solenoid shutdown logic.
View Controller SpecsPre-configured controller mainframes, fast-sniff leak surveys, and certified life-safety instruments tailored for Massachusetts Fire Code (527 CMR 1.00) and NFPA 72/54 installations.
Supervises up to 64 addressable gas sensing channels. Built-in programmable high/low relays, Modbus RTU/BACnet bridge, and fail-safe solenoid shutdown logic.
View Controller Specs
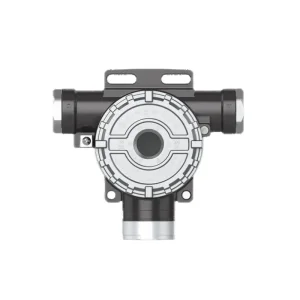
High-precision electrochemical/catalytic sensing for targeted toxic or combustible hazards. IP67 waterproof sealed casing with vibration, visual, and 90dB acoustic alarms.
View Detector Specs
Designed for residential multi-family and commercial kitchens. Features auto-temperature compensation, active drift suppression, and fast pulse pulse valve shut-off relay.
View Multi-Family Unit
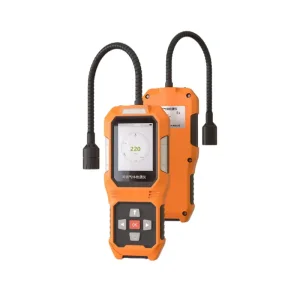
Equipped with semi-conductor and catalytic diffusion sampling for pinpoint leak profiling along municipal risers, boiler fuel trains, and district energy pipeline manifolds.
View Sniffer SpecsA comprehensive engineering and procurement analysis examining why Boston’s institutional density demands high-reliability centralized gas alarm controllers with SIL-2 logic, addressable bus loops, and seamless building management system (BMS) integration.
The Greater Boston metropolitan area—encompassing Cambridge, South Boston Seaport, Route 128 Technology Belt, and Middlesex County—presents one of the most technologically demanding and safety-critical operating environments for gas detection instrumentation in the Western Hemisphere. Unlike conventional petrochemical hubs characterized by vast open-air refineries, Boston’s industrial profile is defined by an ultra-dense confluence of biotechnology cleanrooms, pharmaceutical synthesis vivariums, Ivy League cryogenic research centers, century-old commercial real estate infrastructure, and high-volume marine LNG terminals along Boston Harbor.
In this densely built urban matrix, gas leaks cannot simply be vented to the ambient environment. The Massachusetts Comprehensive Fire Safety Code (527 CMR 1.00), adapted alongside NFPA 1, NFPA 54 (National Fuel Gas Code), and NFPA 45 (Standard on Fire Protection for Laboratories Using Chemicals), imposes zero-tolerance thresholds on hazardous gas containment. System specifiers, mechanical, electrical, and plumbing (MEP) consulting engineers, and plant operations directors require wholesale gas alarm controllers that serve not merely as simple threshold alarms, but as autonomous, failsafe command-and-control safety directors.
Regulatory Compliance Notice (Massachusetts & Boston Fire Dept.): Under Boston Fire Department (BFD) technical bulletins and 780 CMR (Massachusetts State Building Code), centralized gas detection systems protecting commercial boiler rooms exceeding 400,000 BTU/hr, cryogenic nitrogen dewars, or hazardous process spaces must implement fail-to-safe dry-contact relay interlocks capable of instantly cutting primary solenoid valve fuel feeds and triggering emergency positive-pressure ventilation fans within <2.0 seconds of reaching 25% LEL or OSHA PEL toxic thresholds.
Historically, commercial and light-industrial facilities in New England utilized standalone, point-type gas detectors equipped with simple on-board buzzers. However, facility managers across Boston’s academic and pharmaceutical institutions encountered severe operational bottlenecks with this obsolete approach:
Modern wholesale gas alarm controllers, such as the Shield SD8001A/B Series, solve these critical systemic challenges through advanced multi-channel microprocessor architectures. By routing 4-20mA current loops or RS-485 Modbus RTU / BACnet MS/TP digital protocols back to a single central panel situated in an unclassified engineering control room, facility engineers gain real-time visibility into concentration metrics across up to 64 discrete detection nodes simultaneously.
A comparative structural evaluation for Boston MEP contractors, safety consultants, and international EPC project leads.
| Evaluation Parameter | Legacy Standalone Detectors | Commercial BMS-Direct Inputs | Dedicated Shield Gas Alarm Controller |
|---|---|---|---|
| Functional Safety Integrity | Unrated / Non-redundant | Software-based; high risk of OS reboot failure | SIL-2 Hardware Compliant Dual-MCU |
| Response Latency to Actuator | 3.0s – 8.0s (Mechanical delay) | 2.0s – 10.0s (BMS polling lag) | < 1.2s Direct Relay Drive |
| Cabling Topology & Capex | Home-run star wiring; heavy copper cost | Variable analog inputs; high wiring density | M-Bus / RS-485 Daisy Chain (60% cable savings) |
| Hazardous Area Separation | Controls located directly in hazard zone | Requires intermediate explosion-proof barriers | Class I, Div 1 / Zone 1 Field with Safe Control Room Panel |
| Fail-Safe Backup Power | Individual internal batteries fail unpredictably | BMS building UPS dependency | Integrated 24VDC Lead-Acid Smart Float Charger |
| Multi-Tier Alarm Voting | Single point false alarms trigger shutdowns | Complex logic scripting prone to bugs | Built-in 2oo3 (2 out of 3) Voting & Zonal Logic |
How Sichuan Shield Technology bridges high-precision manufacturing, end-to-end component traceability, and extreme cost efficiencies for global wholesale distributors and Boston system integrators.
In modern industrial gas instrumentation, hardware reliability is an uncompromising imperative. A false positive in a Kendall Square biotechnology laboratory halts millions of dollars in biomanufacturing runs; a false negative in an Everett district energy boiler room risks catastrophic deflagration. Sichuan Shield Technology Co., Ltd., headquartered in the high-tech industrial cluster of Chengdu, represents the pinnacle of China’s Industry 4.0 transformation in gas-safety equipment manufacturing.
Operating over 18+ years with 40+ patented sensing algorithms, ASIC circuit topologies, and structural enclosures, Shield combines the cost efficiencies of Chinese high-tier manufacturing with the rigid quality assurance demanded by international standards such as UL 2075, EN 50545-1, IECEx, and China CCC/Ex certifications.
Surface-mount technology (SMT) production lines operating under Class 100,000 cleanroom environments. Automated optical inspection (AOI) and 3D X-ray testing eliminate cold-solder defects on high-frequency microcontroller boards.
Robotic gas-distribution testing chambers run each sensor and controller motherboard through multi-point temperature, humidity, and target gas concentration curves (-40°C to +70°C, 10% to 95% RH).
Direct factory engineering eliminates middleman premiums, offering Boston security wholesalers, MEP distributors, and brand owners custom firmware, enclosures, and protocol gateways within accelerated lead times.
Engineered to mitigate risk in distinct architectural and operational profiles throughout the Massachusetts industrial footprint.
Biomedical incubators utilizing volatile solvents, methane reactors, and liquid nitrogen storage require oxygen depletion detection coupled with LEL hydrocarbon monitoring.
Cryogenic natural gas bunkering, coastal fuel storage, and maritime transport along Massachusetts Bay exposed to extreme saline mist and freeze-thaw cycles.
Aging urban buildings retrofitting legacy steam boilers with high-efficiency gas-fired systems, demanding compliance with strict BFD mechanical ventilation cutoff regulations.
Harvard, MIT, and Boston University research laboratories deploying manifold systems for hazardous specialty gases including hydrogen, argon, and carbon monoxide.
Underground municipal steam, electric, and gas distribution chambers prone to sewer gas accumulation (H2S), methane infiltration, and oxygen deficiency.
High-density restaurant clusters and institutional hospitality kitchens operating heavy cooking equipment requiring mandatory automatic fuel isolation upon gas detection.
Complete product chain spanning industrial point-type transmitters, personal life-safety instruments, and residential/commercial safety hubs.
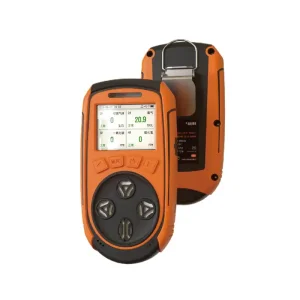
Simultaneous detection of Combustible Gas (%LEL), Oxygen (%VOL), Carbon Monoxide (PPM), and Hydrogen Sulfide (PPM). Ruggedized rubberized casing.
View 4-in-1 Instrument
Rapid gooseneck probe sniffer designed for gas utility field technicians inspecting buried pipe welds, gas meters, pressure relief valves, and boiler connections.
View Wholesale Sniffer
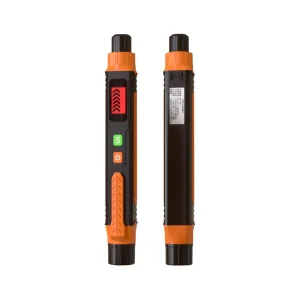
Ultra-compact pocket form-factor engineered for fast leak checking on residential appliance flare fittings, threaded gas couplings, and regulator diaphragms.
View Pen Detector
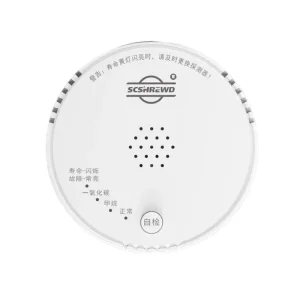
High-precision semiconductor sensor calibrated for methane and LPG. Integrated pulse drive port triggers automatic gas valve shut-off before combustible accumulation.
View Domestic Unit
Single-gas monitor equipped with micro-electrochemical sensors for toxic gas detection (CO, H2S, NH3, Cl2). High-contrast backlit LCD with real-time TWA/STEL tracking.
View Toxic Monitor
Advanced domestic sensor platform with dual alarm stage logic, silence button, and remote status telemetry output for centralized residential building management.
View Residential Hub
Heavy cast-aluminum explosion-proof transmitter. 4-20mA and RS-485 Modbus outputs with on-site OLED display and non-intrusive magnetic wand calibration.
View Industrial Transmitter
Customizable combustible gas alarm module supporting private labeling, protocol adaptation (Zigbee/LoRaWAN/NB-IoT), and tailored trigger voltage outputs for valves.
View OEM/ODM OptionsAuthoritative technical guidance resolving critical specification, protocol compatibility, and compliance questions.
Under Massachusetts Fire Safety Code (527 CMR 1.00) and NFPA 54 Section 7.12, commercial gas installations in excess of 400,000 BTU/hr (or spaces designated as assembly occupancies) require positive fuel shut-off interlocks. The Shield 8001AB provides dedicated dry-contact form-C SPDT relays rated at 250VAC/5A with configurable low (typically 20% LEL) and high (typically 40% LEL) thresholds. Upon reaching AL1, the controller activates an audible-visual warning and energizes local exhaust fans; upon reaching AL2, the controller de-energizes the fail-safe pulse circuit, closing the pipeline emergency solenoid shut-off valve within <1.0 second. Once triggered, the controller enforces a manual-reset lockout ensuring gas flow cannot be restored without certified technician inspection.
Yes. The Shield SD8001A/B Series features native isolated RS-485 Modbus RTU communication operating on standard baud rates (9600 to 115200 bps). Each connected sensor’s live concentration value, fault code (e.g., zero drift, sensor disconnection, voltage sag), and alarm status are mapped to standard holding registers. For native BACnet/IP or MS/TP requirements prevalent in Boston commercial facilities, Shield supplies pre-configured industrial gateway modules that seamlessly translate all holding registers into BACnet Analog Input (AI) and Binary Input (BI) objects without custom scripting.
In extensive multi-story retrofit projects common in Boston's historic building stock, running conduit and 4-wire shielded cable (power + RS-485 data) introduces substantial installation costs. Shield's intelligent M-Bus architecture combines 24VDC operating power and bi-directional digital telemetry over a single non-polarized 2-wire twisted pair (e.g., Belden 8471 or 16 AWG). This eliminates wiring polarity errors during installation and reduces physical copper infrastructure costs by up to 55% over runs exceeding 1,000 meters. For heavy industrial installations with intense electromagnetic interference (VFD motors, high-voltage transformers), Shield’s 4-wire RS-485 bus topology provides superior common-mode noise rejection and rapid polling response.
Cleanroom environments throughout Cambridge and the Seaport District frequently utilize vaporized hydrogen peroxide (VHP), isopropyl alcohol (IPA), and quaternary ammonium disinfectants, which rapidly poison or cause false alarms on low-grade catalytic bead sensors. Shield point-type transmitters (such as the SD2100A and SD2100E) incorporate poisoned-resistant pellistors with proprietary active catalytic coatings, or alternatively, non-dispersive infrared (NDIR) optical sensors that do not chemically interact with the target gas. NDIR sensors are completely immune to silicone and lead poisoning and do not require oxygen to operate accurately.
As a direct manufacturer based in Chengdu with an 18-year industrial footprint, Sichuan Shield Technology maintains standard chassis inventories for rapid fulfillment. Standard controller mainframes (SD8001A/B) and point detectors ship within 7–10 business days for commercial volumes. For OEM/ODM wholesale partners requiring custom branded enclosures, bespoke firmware alarm logic, English/Spanish silk screening, and pre-calibrated sensor heads matching regional gas mixes, prototyping is executed within 14 days with full production rollouts completed within 20–25 days. MOQs for standard units start at single-tier evaluation samples, with wholesale volume discounts scaling from 50+ units.
Normal atmospheric air is composed of approximately 20.9% oxygen by volume (209,000 PPM). When inert gases such as liquid nitrogen (LN2), argon, or helium boil off in enclosed cryogenic vivariums, oxygen is displaced rapidly. Because safe human respiration requires oxygen concentrations between 19.5% and 23.5% VOL, monitoring in parts-per-million would require cumbersome six-figure metrics (e.g., alarm trip at 195,000 PPM). Percentage Volume (%VOL) provides clean, rapid, human-readable clarity for life-safety egress alarms and NFPA 55 compressed gas storage compliance.
Whether you are engineering a multi-channel safety loop for a Cambridge biotech vivarium, distributing certified gas instruments across New England, or developing an OEM branded product line, Shield provides unmatched factory direct precision, compliance documentation, and engineering support.