Tier-1 Core Deployments
Featured Industrial Safety Controllers & Portable Systems for Australia
Direct-from-manufacturer architectures engineered for harsh Australasian environments. Fully certified, bus-networked controllers and precision instruments.
Looking for AS/NZS 60079 & AS 5601 System Compliant Configurations?
Our senior engineering group customizes controller telemetry, Modbus registers, and relay outputs for Australian OEM contracts.
Regional Market Intelligence
Gas Alarm Controller Demand Across Australian Industry
Australia's industrial base spans resource extraction across remote desert territories, mega-scale LNG liquefaction plants, hydrogen hub pilots, and stringent national building codes for urban hospitality and HVAC networks.
LNG Infrastructure & Western Australian Mining
The Pilbara and Bowen Basin demand unyielding instrumentation. Control hubs in remote LNG train terminals and underground hard-rock mines must withstand extreme thermal cycling (+50°C), heavy particulate ingress (IP66 minimum), and explosive atmospheric conditions.
- Continuous CH₄ Lower Explosive Limit (LEL) monitoring via RS485 loop
- Toxic gas detection (H₂S, CO, SO₂) integrated into single central controllers
- Automatic failsafe relay shut-offs for pneumatic and solenoid valves
Australian Green Hydrogen & Ammonia Transition
With billions invested into the Gladstone, Hunter Valley, and Pilbara clean energy corridors, Australian facilities are rapidly upgrading to controllers capable of tracking wide-spectrum gas leaks, especially early-stage low molecular H₂ escaping at high velocity.
- Hydrogen-specific high-speed response controllers with milli-second relays
- Ammonia (NH₃) refrigeration plant leak protection in cold-chain logistics
- SIL-2 capable fault supervision architecture ensuring non-stop uptime
AS/NZS 5601 Commercial Kitchens & Multi-Res
Metropolitan Sydney, Melbourne, and Brisbane require strict compliance with AS/NZS 5601.1 (Gas Installations). Commercial dining kitchens, hospitals, university laboratories, and residential high-rises necessitate interconnected gas leak controllers linked directly to rapid solenoid isolation valves.
- Interlocking with fire suppression systems and HVAC exhaust dampers
- Audio-visual warning panels compliant with municipal fire authority rules
- Tamper-proof manual-reset shut-off triggers preventing recurring incidents
18+
Years Gas Safety R&D Expertise
80+
Mass-Production Safety Models
40+
Patented Core Technologies
< 1s
Controller Relay Linkage Response
Technology Forecasting
Global Industry Trends: The Shift Towards Intelligent, Connected Gas Safety
Procurement managers and system integrators across Australasia, North America, and Europe are transitioning from isolated point alarms to fully integrated industrial IoT monitoring nodes.
Decentralized Sensing with Centralized Microprocessor Control
Modern industrial installations are shifting from heavy star-wired analog configurations (4-20mA loops requiring excessive copper wiring across vast facilities) to multiplexed RS485 Modbus RTU and industrial Ethernet networks.
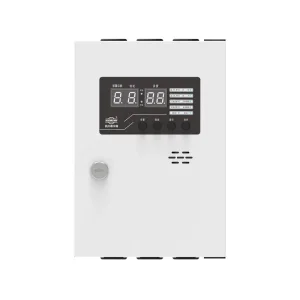
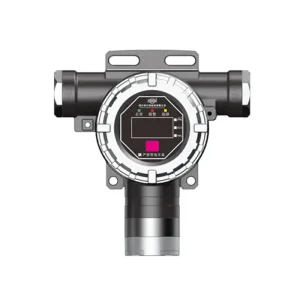
Shield gas alarm controllers (such as the SD8001AB Series) aggregate up to dozens of digital bus-type detectors across hundreds of meters, reducing copper installation costs by up to 60% while providing precise channel-by-channel calibration, diagnostic fault isolation, and pinpoint drift compensation directly from the safe-area control room.
Demand for Full-Chain Hardware Reliability (Detect + Control + Isolate)
Global procurement teams have identified integration latency as the number one failure point during industrial emergencies. Sourcing detector heads from Vendor A, control modules from Vendor B, and solenoid shut-off valves from Vendor C creates communication mismatches, impedance drops, and finger-pointing during compliance sign-offs.
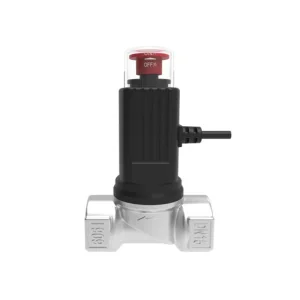
Shield provides a vertically manufactured, single-source gas protection ecosystem. Detectors send precision signals, our controllers analyze thresholds with intelligent noise-filtering algorithms, and immediate linkage fires the JYFJS-011 aluminum alloy emergency valve instantly.
Smart Manufacturing Competence
China Factory 4.0: Supply Chain Resilience, Scalability & Precision
Operating from our high-tech Chengdu manufacturing headquarters, Sichuan Shield Technology delivers direct factory-level pricing without compromising the rigorous metrology required by international certification bodies.
Automated SMT & Sensor Burn-in Labs
Every controller PCB is manufactured using surface-mount technology with automated optical inspection (AOI). Raw catalytic combustion, electrochemical, and NDIR sensors undergo extended environmental chamber aging, mitigating early-life drift before leaving the factory.
Direct OEM/ODM Firmware & Housing Customization
For Australian engineering distributors, we provide white-label branding, customized steel/polycarbonate enclosure stamping, custom-configured LCD/LED interface firmware, Modbus register matching, and complete compliance documentation bundles tailored to local engineering approvals.
Unbroken Raw Material & Component Pipelines
By owning our core mechanical toolings, solenoid valve die-casting lines, and assembly workshops, we insulate our global partners from the chronic component shortages and multi-month delays common among Western brand distributors.
Field Application Engineering
Tailored Safety Blueprints for Australian Facilities
How Shield's integrated detector-controller-valve loop secures critical infrastructure against catastrophic fire, toxic exposure, and regulatory shutdown.
1
Commercial Precincts & Hospitality (AS 5601.1)
Challenge: Australian shopping center food courts and commercial hotel kitchens utilize extensive LPG or Natural Gas manifolds. Minor unlit burners or cracked flexible hoses present massive explosive risks in confined ceiling spaces.
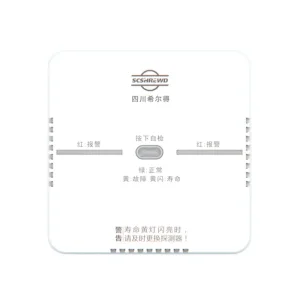
System Solution: Standalone SD2130 detectors or bus-type SD2100E units placed strategically above appliances and pipe risers. Connected directly to the JYFJS-011 aluminum alloy emergency shut-off valve installed upstream on the main line. At 20% LEL, the controller activates audible sirens and snaps the gas supply off in under 1 second. Manual resetting is mandatory, guaranteeing an engineer investigates prior to restarting gas flow.
2
Mining Workshops & Heavy Machinery Fuel Depots
Challenge: Western Australian remote mines store massive volumes of diesel, LNG, and solvent gases. Equipment wash bays and battery charging banks build up hazardous concentrations of hydrogen and volatile organic vapors under extreme heat.
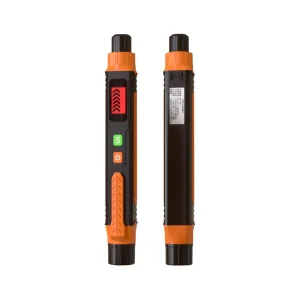
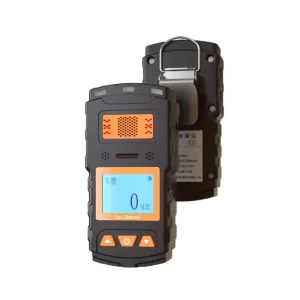
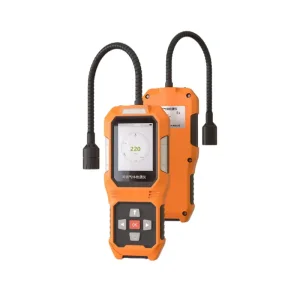
System Solution: Heavy-duty point gas detectors networked into the Shield 8001AB multi-channel controller seated in the central safety office. Workers wear the BTYQ-Z4 portable 4-in-1 monitor for confined tank inspections, while the fixed network activates heavy-duty ventilation fans automatically when flammable gas reaches initial setpoints.
Complete Hardware Ecosystem
Full OEM/ODM Product Catalog for Global Importers
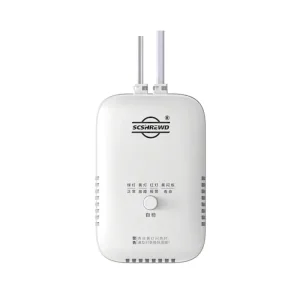
Original manufactured product units ready for private labeling, customized firmware integration, and batch distribution across Australasia.
Compliance & Engineering FAQs
Frequently Asked Technical Questions: Australian OEM Procurement
Essential technical answers on system topology, communication protocols, Australian code alignment, and factory capabilities.
What communication protocols do Shield Gas Alarm Controllers use to integrate with Australian SCADA systems?
Shield Gas Alarm Controllers, including the SD8001AB Series, feature standard RS485 Modbus RTU serial interfaces alongside configurable 4-20mA current outputs. This allows seamless integration into industrial Australian SCADA networks, building management systems (BMS), PLC automation racks, and DCS setups common in Australian refineries, power stations, and municipal wastewater treatment plants.
How do Shield controllers support compliance with Australian Standards (AS/NZS 60079 & AS 5601)?
While local certification requires state-specific gas fitter sign-offs and regulatory approval bodies, Shield designs all hardware architectures to meet or exceed IEC 60079 and ISO 9001 standards. Our explosion-proof field detectors feature heavy-duty flameproof (Ex d) enclosures, and our controllers provide isolated fail-safe relay circuits explicitly suited for driving AS-compliant emergency shut-off valves and extraction fans required under AS/NZS 5601.
What is the difference between Stand-Alone detectors and Centralized Controller architecture?
A stand-alone detector (such as our SD2130) contains onboard detection, audio-visual buzzers, and dry contact relays directly on the unit. It is ideal for single-room installations like a commercial restaurant kitchen or small boiler room. Centralized architecture (e.g., SD2100E detectors combined with an SD8001AB controller) moves the human-machine interface, alarm status, and emergency relay decisions to a safe control room, enabling multi-zone supervision across expansive industrial processing plants.
Can the controller drive automatic gas shut-off valves without intermediate PLCs?
Yes. Shield controllers and standalone detectors feature dedicated high-current relay outputs designed to directly trigger pulse-operated solenoid valves like our JYFJS-011 aluminum alloy valve. The system operates with zero reliance on third-party software, guaranteeing that when the sensor detects combustible gas at 20% or 25% LEL, the mechanical valve snaps closed in fractions of a second.
What OEM / ODM options are available for Australian safety equipment brands?
As a true source factory with over 18 years of R&D, Sichuan Shield Technology offers complete customization. We provide custom front panel silk-screening with your company brand, tailored enclosure colors, custom-programmed alarm setpoints, modified Modbus address maps, custom English language LCD screen menus, and localized packaging for bulk distribution across Australia, New Zealand, and international territories.
Partner with an Established Gas Alarm Controller Manufacturer
Whether you require an engineered quote for an Australian mining installation, bulk commercial kitchen safety devices, or private-label OEM controller manufacturing, our engineering department is ready to assist.