Primary Point-Type Detectors & Environmental Analyzers
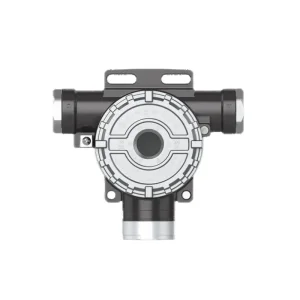
Direct-from-factory instrumentation featuring SIL-2 compliance, ATEX/IECEx explosion-proof cast enclosures, and real-time controller integration.
Evolutionary Trends in Point-Type Gas Detection Technology
The transition from legacy analog catalytic pellistors to smart multi-spectrum optical and solid-state sensing architectures in modern hazardous environments.
NDIR Optical vs. Catalytic Pellistor
Traditional catalytic bead sensors are inherently vulnerable to chemical poisoning by airborne silicones, lead, sulfur compounds, and halogenated hydrocarbons. Modern point-type gas detectors increasingly integrate Dual-Beam Non-Dispersive Infrared (NDIR) optical engines.
NDIR sensors operate fail-safe in inert (oxygen-depleted) atmospheres, do not degrade upon exposure to over-range combustible gas concentrations, and exhibit long-term zero baseline stability over a 10-year operational lifecycle.
- Zero poisoning risk from hexamethyldisiloxane (HMDS)
- No oxygen required for accurate LEL quantification
Digital Bus & Wireless Industrial IoT Mesh
Point-type gas detectors have transitioned from isolated 4-20mA current loop nodes to intelligent digital fieldbus peripherals. Shield instruments feature native RS-485 Modbus RTU, 2-wire M-BUS power-and-data communication, and HART over 4-20mA.
In brownfield and remote retrofits, LoRaWAN and WirelessHART mesh protocols drastically eliminate trenching and explosive-rated conduit expenditures, reducing multi-node plant installation costs by up to 60%.
- Bi-directional remote diagnostic & calibration logging
- Over-the-air firmware updates via non-intrusive IR interfaces
Functional Safety (SIL-2/3) & Self-Diagnostics
Under international safety standards IEC 61508 and IEC 61511, fixed point gas detectors play an active role as Safety Instrumented Functions (SIF). Modern transmitters feature multi-core microcontrollers that continuously interrogate internal sensor impedance.
Comprehensive algorithmic diagnostics detect optical path obscuration, cracked catalyst beads, thermal drift, and amplifier clipping, triggering predictable fault states (<3.6 mA) rather than failing into undetected silence.
- Safe Failure Fraction (SFF) exceeding 90%
- Built-in automated bump test and bump-fail warning logic
Enterprise Buyer Matrix: Sensor Principles vs Target Hazards
A rigorous engineering reference for industrial EPCs, mechanical contractors, and refinery safety directors evaluating point-type detector architectures against real-world chemical matrices.
Key Procurement Consideration: Sensor Specificity & Cross-Interference
Point-type detectors must be carefully matched to physical ambient conditions. Catalytic combustion sensors measure combustible energy indiscriminately across all hydrocarbons, whereas Photoionization Detectors (PID) require matching of ionization potential (IP) lamp energies (9.8eV, 10.6eV, 11.7eV). NDIR sensors, while highly stable, cannot detect homonuclear diatomic gases such as Hydrogen (H₂).
| Sensor Mechanism | Target Gas Families | Typical Dynamic Range | Response Metric (T90) | Environmental Limitations | Optimal Industrial Application |
|---|---|---|---|---|---|
| Dual-Beam NDIR (Infrared) | Hydrocarbons, Methane (CH₄), Propane, CO₂, Refrigerants | 0–100% LEL or 0–100% Vol | < 15 seconds | Cannot detect Hydrogen (H₂), CS₂; degraded by severe optic fogging | Offshore Rigs & LNG Terminals |
| Poison-Resistant Catalytic Bead | All combustible gases & vapors (including H₂) | 0–100% LEL | < 12 seconds | Requires >10% ambient O₂; poisoned by silicones, lead, high sulfur | Boiler Rooms, Gas Turbines |
| Electrochemical Cell (EC) | Toxic gases: H₂S, CO, SO₂, Cl₂, NH₃, HCN, NO₂ & O₂ Deficiency | 0–50 ppm up to 0–5000 ppm (gas specific) | < 20 seconds | Electrolyte dry-out in extreme desert heat; freeze risk < -40°C | Chemical Plants, Water Treatment |
| Photoionization (PID) | Volatile Organic Compounds (VOCs), Benzene, Toluene, Xylene | 0.1 ppm – 2,000 ppm | < 3 seconds | High humidity dampens UV signal; optical lamp cleaning required | Petrochemical Tank Farms & Paint Shops |
| Thermal Conductivity (TCD) | High-concentration gases with divergent thermal properties (H₂, He) | 0–100% Volume | < 10 seconds | Non-specific; carrier gas composition variations induce drift | Hydrogen Electrolyzers, Fuel Cell Skids |
China Industry 4.0: Advanced Supply Chain Resilience & Quality Governance
Inside Sichuan Shield Technology's Chengdu smart facility: Precision automated robotic gas mixing, multi-stage burn-in chambers, and end-to-end component traceability.
Automated SMT & Conformal Coating
Every detector motherboard is fabricated in ISO 9001-certified cleanrooms using high-speed automated Surface Mount Technology (SMT) lines with 100% Automated Optical Inspection (AOI) and X-ray solder integrity audits.
To resist corrosive hydrogen sulfide and saline offshore mists, printed circuit board assemblies (PCBAs) undergo precision robotic selective silicone/polyurethane conformal dip coating compliant with IPC-CC-830 standards.
- Hermetically sealed electronics rated up to IP66/IP67
- Military-grade component derating for -40°C to +70°C
Dynamic Multi-Gas Automated Calibration
Unlike artisanal assembly operations reliant on manual syringe injection, Shield utilizes precision computer-controlled mass flow controllers (MFC) fed by primary certified reference standard gases traceable to NIST/NIM.
Every point-type detector undergoes continuous dynamic temperature and humidity profiling inside automated climatic chambers (-40°C to +70°C, 10% to 95% RH) to write unique polynomial compensation curves to onboard EEPROM.
- Zero-drift mathematical matrix compensation
- Individual factory calibration certificate archive per serial ID
Extended Thermal Aging & Burn-In
Early sensor mortality is systematically eradicated through an uncompromised 72-hour operational burn-in protocol under energized cyclic load. Detectors are continuously scanned for drift, thermal noise, and internal component impedance spikes.
Cast aluminum alloy and 316 stainless steel explosion-proof flame paths undergo 100% hydrostatic and helium pressure leak tests to ensure non-propagating containment during hazardous internal flashovers.
- Ex d IIC T6 Gb certified flameproof integrity
- Defect rates constrained below 120 PPM across 500,000+ units
Localized Engineering Topologies Across Global Industrial Landscapes
Deploying specialized point-type detection matrices tailored to localized safety standards, environmental microclimates, and dynamic physical risks.
Refinery Tank Farms & Loading Terminals
High-volatility hydrocarbon vapours pool in low-lying relief pits and loading bays. SD2100A/E point-type detectors are deployed at ground elevation (within 30cm of the floor) with weatherproof splash guards to deliver sub-second alarms before vapor plumes encounter ignition sources.
- Topology: 4-20mA loop with HART into Honeywell Experion DCS
- Zone Classification: ATEX Zone 1 / Class I, Div 1
Hydrogen Production & Fuel Cell Skids
Hydrogen’s ultra-low density causes rapid vertical dispersion, while its low ignition energy (0.017 mJ) requires rapid intervention. Point detectors with high-speed micro-pellistors or thermal conductivity cells are ceiling-mounted directly above electrolyzer stacks and compressor heads.
- Topology: High-speed relay trip driving automated Nitrogen purges
- Enclosure: 316 Stainless Steel Group IIC certified
Commercial Kitchens & Central Boiler Plants
Commercial culinary facilities and boiler rooms require autonomous protection without requiring complex programmable logic controllers. The standalone SD2130 series features built-in 85dB sirens, strobe LEDs, and direct 24V dry contacts to immediately actuate JYFJS-011 emergency shut-off valves.
- Topology: Standalone unit triggering solenoid valves & roof fans
- Target: Methane (ceiling-mounted) or LPG (floor-mounted)
Underground Utility Corridors & Vaults
Municipal sewer interceptors, utility tunnels, and underground electrical vaults suffer from dual hazards: methane accumulations from pipe breaks and fatal H₂S/CO concentrations from organic breakdown. Shield bus systems connect hundreds of transmitters over 2-wire lines spanning several kilometers.
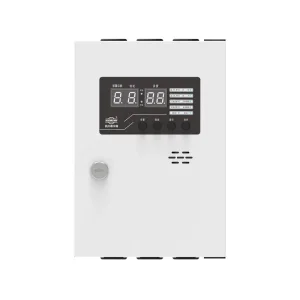
- Topology: 2-Wire M-BUS network linked to Shield 8001AB panels
- Environmental: IP67 submersion-proof enclosures
Gas Detection Engineering FAQ: Standards, Mounting & Calibration
In-depth responses compiled by Shield’s Chief Instrumentation Engineers to resolve key system design challenges encountered during procurement and commissioning.
How do engineers determine the physical mounting height and radius of point-type detectors? +
Mounting location is governed strictly by the Vapor Density of the target gas relative to air (defined as 1.0 at standard temperature and pressure) and local engineering standards such as NFPA 72, ISA-12.13.01, and EN 60079-29-2:
- Lighter-than-air gases (e.g., Methane < 0.55, Hydrogen ~ 0.07, Ammonia ~ 0.59): Install transmitters 30 cm to 50 cm below the highest ceiling accumulation pockets, avoiding direct exhaust drafts or dead zones behind overhead structural I-beams.
- Heavier-than-air gases (e.g., Propane ~ 1.52, Butane ~ 2.05, Hydrogen Sulfide ~ 1.19): Install transmitters 30 cm to 45 cm above the finished floor or trench bottom to capture creeping vapors before they pool toward ignition sources.
- Detection Radius: In enclosed industrial plant areas without dominant wind currents, typical point detector spacing assumes an effective protective radius of 5 to 7.5 meters per detector. Outdoor process units require spacing reduction based on prevailing wind rose models.
What is the explicit operational difference between LEL% and Gas Volume% (%VOL)? +
This is the most critical configuration parameter in combustible gas safety:
The Lower Explosive Limit (LEL) represents the minimum concentration of a combustible gas in air capable of propagating a flame when ignited. For example, Methane has an LEL of approximately 5.0% by volume in air (under IEC standards, or 4.4% by volume under NFPA/US standards). Therefore, if an instrument display reads 100% LEL, it indicates the air currently contains 5.0% pure methane by volume.
Alarm setpoints are set well below this threshold: the Low Alarm (AL1) is customarily set at 20% to 25% LEL (which corresponds to only 1.0% to 1.25% pure methane by volume), giving automated exhaust blowers time to dilute the concentration long before it approaches an explosive condition.
What are the maintenance intervals, bump testing protocols, and calibration cadences? +
To ensure life-safety readiness, industrial facilities must delineate between Bump Testing and Full Span Calibration:
- Bump Test (Qualitative Verification): Involves brief challenge gas exposure to verify sensor response and alarm actuation without altering internal zero/span values. Recommended weekly or bi-weekly in safety-critical refinery zones.
- Span Calibration (Quantitative Adjustment): Adjusts the instrument's amplification curve using certified span gas mixtures. Recommended every 3 to 6 months for catalytic and electrochemical sensors, and 12 to 24 months for NDIR optical devices.
- Non-Intrusive Magnetic Wand / IR Calibration: Shield detectors feature through-the-glass optical calibration interfaces, allowing single-technician calibration in hazardous Zone 1 environments without opening the enclosure or hot-work permits.
How does a Standalone Point Detector (SD2130) differ architecturally from a Bus System (SD2100E)? +
The choice between standalone and networked point detectors depends on spatial distribution and the control hierarchy:
Standalone Transmitters (SD2130 Series): Contain integrated high-power relays (NO/NC) and onboard audible/visual strobe alarms. They operate as fully autonomous safety nodes, directly powering solenoid shut-off valves or exhaust fans upon alarm without needing external PLC or controller wiring. Ideal for isolated commercial kitchens, boiler rooms, and laboratory vaults.
Digital Bus/Branch Detectors (SD2100A/E Series): Designed for centralized plant architecture. Detectors transmit live gas readings and diagnostic codes over two-wire non-polar M-BUS or RS-485 Modbus networks back to central control consoles (such as the Shield 8001AB Series) positioned in non-hazardous control centers, aggregating up to 128 channels per master unit.
What certifications are required for hazardous location gas detector deployment? +
Point-type gas detectors deployed in volatile areas must be certified against potential explosive atmospheres created by combustible gases, vapors, or mists:
- ATEX & IECEx: Certified for Zone 1 and Zone 2 hazardous locations under Ex d (flameproof containment) or Ex ia/ib (intrinsic safety). Shield industrial series utilize Ex d IIC T6 Gb rated enclosures.
- Functional Safety (SIL-2 / SIL-3): Compliance with IEC 61508 demonstrating rigorous hardware fault tolerance and low Probability of Failure on Demand (PFD).
- In China: Mandatory CCC certification (China Compulsory Certification) and Ex-proof conformity approval by national testing bodies (e.g., NEPSI, CQST).
Wholesale Fixed Transmitters, Specialized Leak Detectors & Home Units
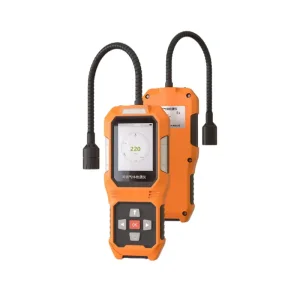
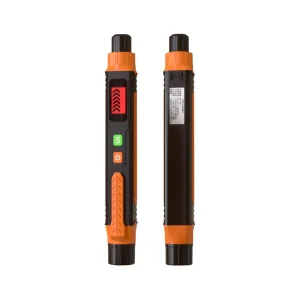
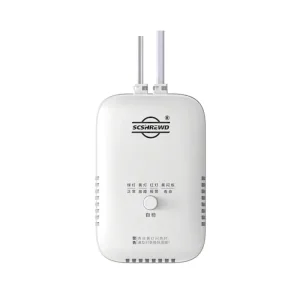
Complete safety hardware portfolio engineered for end-to-end gas containment, automated pipeline isolation, and mobile hazard surveys.
Initiate Your Factory-Direct Point Detector Order or OEM Partnership
Connect directly with Sichuan Shield Technology's engineering and export operations. Benefit from custom sensor range calibration, private-label branding, full explosion-proof compliance documentation, and scalable production lead times.