OEM/ODM Core LPG Monitoring & Shut-Off Hardware
Pre-engineered hardware platforms manufactured under strict ISO9001 and CCC fire safety protocols, configured for rapid private-label global distribution.
Global Macro Paradigm: Navigating Liquefied Petroleum Gas Volatility & Safety Governance
Liquefied Petroleum Gas (predominantly commercial propane $C_3H_8$, butane $C_4H_{10}$, or tailor-blended seasonal compositions) constitutes an indispensable primary energy pillar across global off-grid residential heating, light-industrial metal processing, commercial hospitality, and agricultural operations. Unlike natural gas (methane, $CH_4$, relative vapor density approximately 0.55 relative to air), vaporized LPG carries an aerial density index between 1.50 and 2.00. In the event of containment degradation, fugitive LPG fails to rise toward soffits or ceiling vents; instead, it behaves as a heavy, floor-hugging vapor blanket, migrating silently into drainage sumps, service trenches, crawlspaces, and basement cavities.
When airborne concentrations penetrate the explosive perimeter—spanning the Lower Explosive Limit (LEL) of 1.7% to 2.1% to an Upper Explosive Limit (UEL) around 9.5% to 10.1% by volume—the introduction of even sub-millijoule parasitic electrical arcs can trigger violent deflagration or vapor cloud explosions (VCE). Consequently, the global procurement landscape for OEM LPG monitors has shifted definitively away from generic consumer alarms toward precision-engineered, dual-tier alarm instrumentation equipped with SIL-rated fail-safe electromagnetic isolation linkages, wide-range thermal drift compensation, and robust resistance to chemical cross-poisoning.
| Gas Hydrocarbon Fraction | Molecular Weight (g/mol) | Relative Vapor Density (Air = 1.0) | LEL (Vol % / %LEL Equiv.) | Target Sensor Height Mandate | Dominant Industrial Standards |
|---|---|---|---|---|---|
| Commercial Propane ($C_3H_8$) | 44.10 | 1.52 (Sub-surface sinking) | 2.1% Vol = 100% LEL | 0.1m – 0.3m Above Floor Level | NFPA 58 / EN 50194-1 / UL 1484 |
| Commercial Butane ($C_4H_{10}$) | 58.12 | 2.01 (Heavy stratification) | 1.8% Vol = 100% LEL | 0.1m – 0.2m Above Floor Level | EN 50194-2 / AS/NZS 5601.1 |
| LPG Auto-Mix ($70/30 - 60/40$) | ~48.30 | 1.66 – 1.82 (Dense creeping) | ~1.9% Vol = 100% LEL | Within 300mm of Finished Floor | GB 15322.1 / GB 15322.2 / ATEX Zone 1/2 |
| Pipeline Methane Reference ($CH_4$) | 16.04 | 0.55 (Buoyant ceiling ascent) | 5.0% Vol = 100% LEL | 0.3m – 0.5m Below Highest Ceiling | EN 60079-29-1 / IECEx Ex db IIC |
High-Risk Localized Application Scenarios
From central LPG vaporizing stations to commercial culinary lines, our OEM detector-valve topologies isolate gas hazards instantly at point of failure.
Commercial Cloud Kitchens & Hotels
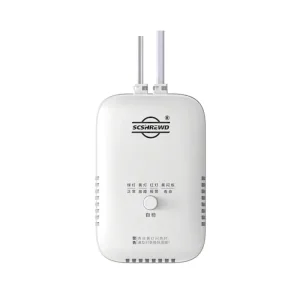
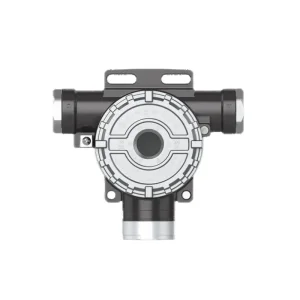
Continuous exposure to oil mist, high ambient humidity (up to 95% RH), and volatile organic food acids causes rapid baseline drift in entry-level detectors. Shield’s OEM industrial point-type platforms (such as the SD2100A and stand-alone SD2130) deploy micro-porous PTFE sinter filters and catalytic pellistors treated with anti-silicone passivation. In the event of a manifold leak, auxiliary relays trigger dry contacts to drop exhaust fire dampers and command JYFJS-011 valves shut within 1 second.
Vaporization Plant & Bulk Manifolds
Multi-cylinder banks, electrical water-bath vaporizers, and pressure-regulating skids demand continuous wide-area hazardous zone surveillance. Utilizing RS-485 Modbus RTU or 4-20mA two-wire industrial loops, clusters of SD2100E explosion-proof point detectors interface seamlessly with the centralized SD8001A/B rack controller placed inside safe control rooms, executing matrix shutdowns of main supply solenoids under Ex d IIC T6 Gb parameters.
Multi-Family Residential Apartments
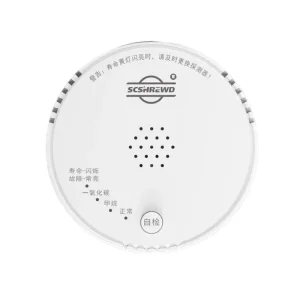
Large-scale urban municipal housing initiatives deploying shared piped LPG or localized metered cylinder cabinets require high reliability without false positive alarms caused by cooking wine, aerosol sprays, or ethanol vapors. Shield's household series (SD6200, SD6103K, SD6101) leverage custom algorithmic peak detection to differentiate short ethanol spikes from steady-state hydrocarbon leak curves, directly powering local pulse solenoids without external AC contactors.
Sensor Architecture Roadmap: Catalytic Bead vs. Dual-Beam NDIR vs. MEMS
Selecting the ideal sensing platform represents the ultimate trade-off in OEM hardware design. Our Chengdu R&D engineering facility designs, bonds, and packages three divergent transducer technologies, aligning strictly with the customer's target price envelope, deployment context, and maintenance ecosystem:
| Detection Metric | Catalytic Combustion (Pellistor) | Non-Dispersive Infrared (NDIR) | Smart Thin-Film MOX / MEMS |
|---|---|---|---|
| Operating Principle | High-temp surface oxidation changing Wheatstone bridge resistance balance. | Infrared optical absorption at 3.3–3.4 μm hydrocarbon absorption band. | Surface chemi-sorption altering semiconductor oxide depletion layer. |
| Oxygen Dependency | Mandatory (>10% Vol $O_2$ required for catalytic combustion reaction). | Completely immune to anaerobic/inert atmospheres ($0\%\;O_2$ functional). | Partial (baseline drifts significantly in depleted $O_2$ air volumes). |
| Poisoning Vulnerability | High susceptibility to silicone vapors, lead, and sulfur compounds. | Impervious to chemical poisons, siloxanes, and hydrogen sulfide ($H_2S$). | Moderate susceptibility; exhibits reversible thermal desorbing profiles. |
| Power Profile | Moderate to high (~120–160 mA @ 3.3V DC continuous heater coil load). | Medium (~35–60 mA active micro-optical pulse / LED emitter cycling). | Ultra-low (sub-15 mW micro-hotplate pulse driving suitable for battery). |
| Expected Sensor Lifespan | 3 to 5 Years under typical non-continuous exposure environments. | 8 to 10+ Years with negligible optical drift degradation curves. | 5 to 7 Years; compact micro-die form-factor for high-density SMT. |
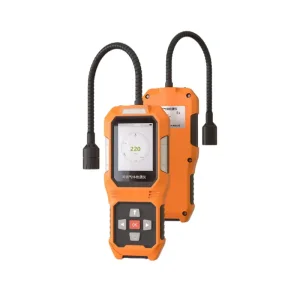
| Recommended OEM Role | Universal commercial kitchen alarms, portable leak sniffers (JLY-CP100). | Industrial petrochemical platforms, remote unattended bulk LPG depots. | Smart municipal battery-operated domestic meters & LoRaWAN detectors. |
IoT Connectivity Matrix: Telemetry, Protocols, and Interlocking Cut-Off
Standalone sensing without deterministic isolation creates a catastrophic gap in life safety. Shield’s OEM engineering ecosystem integrates three tiers of hardware control logic:
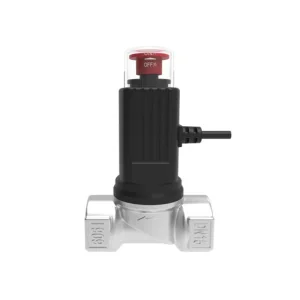
Tier 1: Direct Electrical Pulse Interlocking: For household and small commercial setups, our detectors feature internal capacitor bank discharging circuits that deliver an instantaneous 12V–24V DC pulse (duration: <50ms) to the JYFJS-011 solenoid cut-off valve. This snap-action pulse closes the mechanical valve in less than 1.0 second without requiring external continuous holding power. Crucially, the valve is engineered with a manual reset lockout: once activated, the gas supply cannot be physically restored by electronic software until a trained human technician physically clears the leak origin and raises the red reset collar.
Tier 2: Industrial Multi-Drop Bus Telemetry: In multi-point commercial structures, the SD2100 series communicates via non-polarized 2-wire intelligent power-line carrier or isolated RS-485 Modbus RTU buses across distances exceeding 1,200 meters. Detectors transmit continuous LEL status, self-test health metrics, dirty-sensor warning flags, and ambient temperature readings back to the SD8001 central controller, which governs high-power relay outputs for explosion-proof extraction blowers.
Tier 3: Low-Power Wireless Telemetry (NB-IoT & LoRaWAN): To accommodate retrospective municipal installations without breaking concrete walls for conduit, our battery-operated and hybrid OEM modules feature integrated Sub-GHz LoRaWAN (868MHz / 915MHz) or cellular NB-IoT transceivers. These transmit daily keep-alive heartbeat pings, battery cell voltage metrics, and instant push-alarm states directly to municipal utility SCADA servers via MQTT/CoAP interfaces.
Chengdu Manufacturing Facility: End-to-End Vertical Integration
Direct supply-chain mastery eliminating middle-tier markups. In-house tooling, SMT high-speed placement, and multi-gas dynamic calibration chambers under one roof.
Automated Gas Calibration Rigs
Unlike competitors performing static box calibration, Shield employs custom-built multi-station dynamic flow mixing benches. Sensors are exposed to certified primary standard propane and butane gas blends in environmentally regulated wind chambers, automating zero-point baseline trimming and span sensitivity programming at high volume.
Rapid Tooling & Mold Prototyping
With an in-house tooling center and precision injection molding machinery, we amortize Non-Recurring Engineering (NRE) costs rapidly. We can modify housing acoustics, add private brand logos, create IP66 dust/waterproofing seals, or customize mounting brackets in as little as 14 to 21 business days.
Supply Resilience & Component Control
Our Chengdu manufacturing headquarters leverages mature regional supply chains for high-volume SMT PCBA assembly, precision brass and cast aluminum machining, and automated coil winding. This vertical depth ensures complete isolation from global component shortages and stable shipping windows.
Global Regulatory Compliance & Factory Verification Pathways
Navigating international safety certifications is a core strength of Shield’s OEM engineering team. We assist brand distributors, engineering contractors, and energy conglomerates in preparing compliance dossiers for various regulatory authorities:
- European Union (CE, EN 50194-1, EN 50194-2, ATEX): Electrical safety and electromagnetic compatibility (EMC EN 50270), functional performance testing for domestic electrical apparatus for detecting combustible gases in domestic and recreational craft premises, and ATEX directive (2014/34/EU) compliance for hazardous area explosion proofing (Ex db IIC T6 Gb).
- North American Standards (UL 1484, NFPA 54 & 58, CSA 6.19): Standards covering residential gas detectors, commercial valve requirements, and safe installation clearances for Liquefied Petroleum Gas systems.
- China Compulsory Certification (CCC Fire Protection): Comprehensive full-scale type testing under GB 15322.1 (industrial point-type detectors), GB 15322.2 (household combustible alarms), and GB 3836 series explosion-proof electrical protocols.
Frequently Asked Questions: Technical & OEM Procurement
Detailed technical guidance on gas physics, sensor longevity, interlocking solenoids, and factory OEM private labeling.
1. What is the fundamental physical difference between installing an LPG monitor versus an LNG (Methane) monitor?
2. Why does an OEM LPG monitor alarm setpoint typically trigger at 10%–25% LEL instead of 100% LEL?
3. How does the JYFJS-011 Solenoid Valve ensure fail-safe operation during power outages or post-alarm scenarios?
4. What strategies prevent false alarms caused by airborne cooking vapors and alcohol in commercial kitchens?
5. What are the minimum order quantities (MOQ) and lead times for OEM private labeling and housing tooling?
6. How do bus-type networkable detectors (SD2100A) compare with standalone detectors (SD2130) for industrial installations?
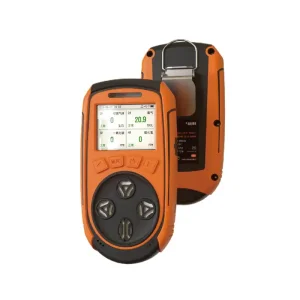
Complementary Industrial Monitoring & Shut-Off Hardware
Integrate our multi-gas portable instruments, domestic alarms, and high-flow cast aluminum valves into your safety procurement framework.
Collaborative OEM/ODM Engineering Engagement Roadmap
Partnering with Sichuan Shield Technology Co., Ltd. gives engineering contractors, distributors, and global brands direct access to our manufacturing infrastructure in Chengdu, China. Every OEM deployment follows a structured, milestone-driven framework:
Phase 1: Application Review & Target Gas Profiling: Our application engineers evaluate your deployment profile—target hydrocarbon mix (pure propane, commercial butane, LPG/Air SNG), operational humidity ranges, hazardous zone classifications (Safe Area, Zone 1, Zone 2), and required output triggers (dry contact relays, 12V pulse, Modbus, or wireless LoRaWAN/NB-IoT).
Phase 2: DFM, PCBA Customization & Prototyping: We tailor the PCBA layout, select matching transducer elements (catalytic bead, NDIR, or semiconductor), optimize power dissipation, and prepare prototype tooling for bespoke enclosures. First-article functional prototypes are delivered within 15 to 25 business days.
Phase 3: Environmental Chamber Validation & Gas Calibration: Prototype units undergo 100% automated calibration across our dynamic multi-gas calibration benches. We verify zero-drift, cross-sensitivity suppression, thermal endurance from -40°C to +70°C, and drop-impact resistance.
Phase 4: Regulatory Dossier Packaging & Volume Rollout: We provide full engineering support, including schematic documentation, PCB Gerber data, component bill of materials (BOM), and factory verification certificates, assisting partners in securing local certifications (UL, CE/ATEX, Inmetro, EAC, or CCC). Routine bulk production runs operate on predictable 20-to-30 day cycles, backed by end-to-end component traceability.