Enterprise-Grade Gas Safety & Toxic Detection Equipment
Explore our certified toxic and combustible gas hardware ecosystem, built with high-repeatability electrochemical sensor cores, multi-topology bus protocols, and automated valve shut-off linkages.
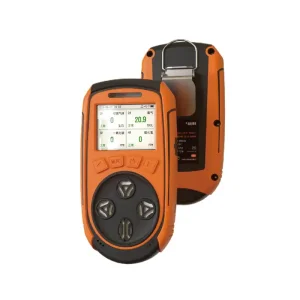
OEM 4 in 1 Portable Gas Detector BTYQ-Z4 Series - Reliable Safety Solution from China Suppliers and Factory Manufacturer, Manufacturers
Explore Model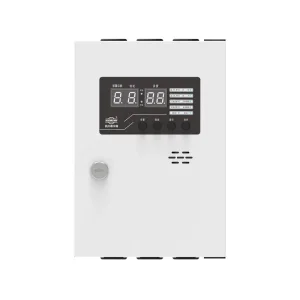
ODM Gas Alarm Controller Shield 8001AB Series - Reliable Gas Detection by China Suppliers and Factory Manufacturers, Factories
Explore Model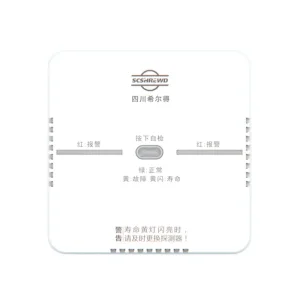
Wholesale Household Combustible Gas Detector SD6200 Series - China Suppliers & Factory Safety Solution Manufacturers, Supplier
Explore Model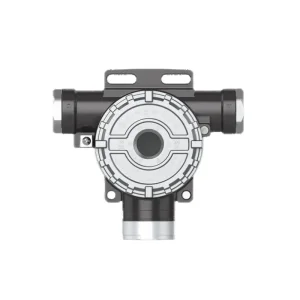
High-Quality Industrial and Commercial Gas Detector SD2100A Series - Reliable Solutions by China Suppliers and Factory Manufacturer, Factories
Explore Model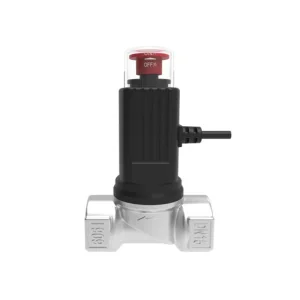
ODM China JYFJS-011 Aluminum Alloy Electromagnetic Gas Shut-off Valve - Reliable Suppliers & Factory Supplier, Factory
Explore Model
Wholesale China SD2100A Series Industrial and Commercial Gas Detectors - Reliable Suppliers and Factory Quality Solutions Manufacturer, Manufacturers
Explore Model
OEM Gas Alarm Controller Shield 8001AB Series - Reliable Gas Detection System from China Suppliers & Factory Factory, Factories
Explore Model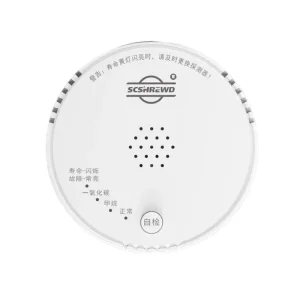
High-Quality China Household Combustible Gas Detector SD6103K Series - Reliable Safety Solution from Trusted Suppliers and Factory Manufacturers, Factories
Explore ModelGlobal Landscape of Carbon Monoxide Mitigation & Smart Sensing
Analyzing critical life-safety trends, toxic atmospheric profiling, and the transition from legacy passive alarms to intelligent, connected multi-protocol gas safety systems.
The "Silent Killer" Imperative
Carbon Monoxide (CO) represents one of the most perilous non-sensory occupational and domestic toxins globally. With a molecular weight of 28.01 g/mol—nearly identical to ambient air (28.96 g/mol)—CO mixes homogenously without stratified buoyancy separation.
Because it binds to hemoglobin with an affinity approximately 210 times greater than oxygen, forming carboxyhemoglobin (COHb), human exposure triggers tissue hypoxia even at trace parts-per-million (ppm) levels. Global industrial regulations (OSHA, EN 50291, UL 2034) mandate uncompromising accuracy down to ±5 ppm across fluctuating relative humidity and temperature regimes.
Commercial & Regulatory Evolution
The global demand for high-reliability Smart Carbon Monoxide Detectors is experiencing exponential compound annual growth (CAGR > 8.4%), accelerated by mandatory multi-family residential building codes, hotel hospitality guest safety legislation, and subterranean vehicular parking facility decarbonization mandates.
Modern enterprise procurement is decisively moving away from isolated, buzzer-only standalone units. Facility engineers and safety integrators now demand automated closed-loop mitigation: local acoustic-optical alerts, BACnet/Modbus telemetry, and immediate pneumatic or electromagnetic shut-off of incoming gas fuel lines.
IoT Integration & Connected Edge
Emerging standards require smart detectors to serve as active edge nodes. Shield's design methodology incorporates low-power microcontrollers running advanced digital filtering algorithms (Savitzky-Golay and recursive Kalman filtering) to eliminate false positives induced by volatile organic compounds (VOCs) or cooking ethanol.
With integrated RF meshes (Sub-GHz, Zigbee 3.0, Matter, NB-IoT, and LoRaWAN), these devices communicate instantaneous ppm curves directly to building management systems (BMS) and cloud safety dashboards, triggering auxiliary exhaust fans and emergency notification cascades within sub-second reaction windows.
Electrochemical Sensing Dynamics vs. Cross-Sensitivity Interference
Delivering high-accuracy toxic detection requires strict sensor physics, robust electrolyte formulation, and intelligent baseline temperature-drift compensation.
3-Electrode Electrochemical Cell Architecture
At the center of Shield's advanced smart CO detectors lies a high-precision, fuel-cell-type electrochemical sensor. The sensing system utilizes a three-electrode configuration: Working Electrode (Anode), Counter Electrode (Cathode), and Reference Electrode submerged within an acidic aqueous electrolyte matrix.
When carbon monoxide molecules diffuse through an anti-condensation porous PTFE membrane, an electro-oxidation process occurs at the catalytic working electrode: CO + H₂O → CO₂ + 2H⁺ + 2e⁻. Concurrently, oxygen dissolved at the counter electrode undergoes reduction: ½ O₂ + 2H⁺ + 2e⁻ → H₂O. The resulting nanoampere-level electron flow is linearly proportional to the ambient CO concentration in parts per million (ppm).
- Stable Reference Electrode: Maintains constant interfacial potential, preventing baseline drift across continuous operational life exceeding 5 to 10 years.
- Anti-Acid Poisoning Catalyst: Advanced platinum-ruthenium catalyst mixtures prevent passivation from sulfur dioxide (SO₂) and nitrogen oxides (NOx).
- Hermetic Ultrasonic Sealing: Elimination of adhesive seals prevents electrolyte leakage across deep thermal cycles (-20°C to +55°C).
Hydrogen & Humidity Compensation Matrices
A persistent operational dilemma in industrial boiler facilities and commercial kitchens is false triggering from non-target gases, primarily airborne Hydrogen (H₂) and volatile hydrocarbon vapors. Shield applies a multi-layered hardware and algorithmic filter mechanism:
We incorporate dual-catalyst differential sensing chambers alongside chemical-grade charcoal scrubbers that mechanically absorb interfering alcohols and solvent vapors. On the digital edge, our onboard 32-bit ARM Cortex M4 processor continuously queries an ultra-precise NTC thermistor and capacitive hygrometer to execute dynamic baseline curve rectification.
- Cross-Sensitivity Rejection: Less than 1% cross-sensitivity to Hydrogen at 100 ppm H₂ levels.
- Active Polynomial Drift Algorithms: Dynamic thermal lookup tables maintain measurement integrity from 5% to 95% non-condensing relative humidity.
- Self-Diagnostic Pulsed Voltammetry: Every 24 hours, the internal MCU applies a non-intrusive micro-pulse to verify catalyst impedance and electrolyte conductivity.
| Detection Technology | Response Time (T90) | Long-Term Baseline Drift | Cross-Gas Interference | Power Consumption | Primary Industrial Sector |
|---|---|---|---|---|---|
| 3-Electrode Electrochemical (Shield Proprietary) | < 15 seconds | < 2% per annum | Extremely Low (Built-in Carbon Filter) | < 15 μA (Battery-friendly) | Residential / Commercial / Industrial |
| Metal Oxide Semiconductor (MOS) | 30 – 60 seconds | > 8% per annum | High (Alcohol, Moisture, VOCs) | 150 – 300 mA (Heater required) | Low-Cost Consumer Only |
| Dual-Beam NDIR Infrared Core | < 20 seconds | < 1% per annum | Immune to chemical poisons | 35 – 80 mA (Optical source) | Heavy Petrochemical & Tunnels |
| Catalytic Combustion Bead (Pellistor) | < 12 seconds | Subject to silicone poisoning | Responds to all combustibles | > 250 mA (High thermal load) | Explosive Combustibles Only |
China Factory Efficiency & Scalable Manufacturing Supremacy
How Sichuan Shield Technology leverages Chengdu's high-tech aerospace & precision instrumentation cluster to deliver unmatched quality consistency, rapid OEM turnaround, and cost optimization.
Automated SMT & Cleanroom Production
Our manufacturing complex located in Chengdu's Southwest Airport Economic Development Zone houses fully automated Japanese high-speed Yamaha SMT placement lines and nitrogen-atmosphere reflow ovens.
Every printed circuit board assembly (PCBA) undergoes 100% 3D Automated Optical Inspection (AOI) followed by In-Circuit Testing (ICT). Surface conformal coatings are robotically applied to protect critical traces against industrial chemical corrosion, sulfurization, and condensation, meeting stringent class IP66/IP67 ingress ratings.
Automated Multi-Point Chamber Gas Calibration
Unlike assembly shops that utilize random statistical batch testing, Shield enforces a strict 100% full-run gas verification protocol across computerized environmental walk-in chambers.
Every detector unit is subjected to calibrated analytical-grade target gases at precise concentrations (30 ppm, 50 ppm, 100 ppm, and 300 ppm CO) blended with synthetic air. Automated robotic test racks record sensor output curves, calculate exact sensitivity coefficients, and burn individual digital calibration matrices directly onto the device's onboard EEPROM.
Vertical Supply Chain & BOM Compression
China's comprehensive electronics and mechanical ecosystem enables Shield to integrate mold design, high-pressure die-casting for explosion-proof aluminum housings, precision plastic injection, and valve machining in-house.
By bypassing multiple intermediate distributor tiers, our OEM partners achieve 25% to 40% BOM (Bill of Materials) cost compression relative to Western peers, while maintaining superior engineering tolerances, faster NPI (New Product Introduction) cycles, and uncompromised regulatory compliance.
Localized Applications: From Micro-Residential to Mega-Industrial
Architecting multi-point safety configurations tailored to real-world gas dispersion dynamics, ambient airflow variables, and automated plant shut-down mechanisms.
1. High-Density Residential Apartments & Smart Urban Real Estate
Modern enclosed residential buildings with gas water heaters, forced-air gas furnaces, and integrated domestic kitchens face significant carbon monoxide risks caused by compromised flue liners or backdrafting. Shield’s residential smart CO solutions (e.g., SD6200 and JT-SD6103K series) provide continuous ambient sampling.
When airborne levels breach pre-alarm thresholds (typically 50 ppm for 60–90 min, or 100 ppm for 10–40 min per EN 50291/UL 2034 curves), the detector triggers an 85 dB local acoustic horn, pulses a high-candela strobe, broadcasts push alerts via Wi-Fi/Matter, and fires a millisecond pulse to activate an emergency shut-off valve (JYFJS-011) situated on the main gas riser.
- Mounting Practice: Installed on breathing zone wall planes (1.5 m above floor) or 1–3 meters horizontal distance from gas combustion appliances.
- Fail-Safe Protocol: The shut-off valve mechanically locks drop-tight, requiring physical on-site human inspection before manual reset.
2. Subterranean Parking Garages & Logistics Freight Docks
Enclosed multi-tier parking garages and enclosed loading hubs accumulate hazardous CO plumes from internal combustion engine exhaust during peak traffic intervals. Operating ventilation exhaust fans at 100% capacity continuously incurs catastrophic electric utility costs.
Shield’s industrial point-type detectors (SD2100A and SD2100E series) communicate seamlessly over an RS-485 Modbus RTU or 4–20 mA loop to central controllers (SD8001A/B). The system executes multi-zone variable-speed drive (VFD) fan sequencing: activating staged ventilation at 25 ppm CO, escalating to high-velocity extraction and audio alerts at 50 ppm, and sounding severe fire-service alarms at 100 ppm.
- Energy Conservation: Reduces commercial building HVAC and ventilation energy consumption by 45% to 70%.
- Zonal Bus Topology: A single 2-wire or 4-wire bus connects up to 64 detector heads back to the non-hazardous control room rack.
3. Commercial Hospitality Kitchens & Industrial Boiler Rooms
Large commercial kitchens in hotels, hospitals, and educational campuses operate high-capacity gas woks, convection ranges, and commercial steam generators under heavy kitchen exhaust hoods. Extractor fan failure or negative pressure fluctuations can cause rapid flue gas back-spillage into prep stations.
Standalone point gas detectors like the Shield SD2130 series feature integrated alarm relays that directly trip localized gas solonoid supply valves, energize emergency fresh-air make-up fans, and signal the main fire alarm control panel (FACP) without requiring an intermediate PLC.
- High-Temperature & Grease Immunity: Stainless steel sintered flame arrestors and hydrophobically coated diaphragms shed oil mist and steam.
- Dual-Hazard Gas Detection: Combined CO and Combustible Hydrocarbon (Methane/LPG) dual-sensor units safeguard against both explosion and asphyxiation.
4. Petrochemical Plants, Metallurgy Furnaces & Confined Spaces
In basic oxygen furnace steelmaking, blast furnaces, petroleum refining cracking towers, and municipal utility tunnels, CO is a critical byproduct present at deadly concentrations exceeding thousands of ppm. Workers entering these spaces risk rapid unconsciousness within two breaths.
Shield BTYQ-Z4 portable 4-in-1 multi-gas detectors accompany maintenance personnel into confined entry vessels. Concurrently, explosion-proof fixed point detectors (Ex d IIC T6 Gb certified) provide permanent perimeter surveillance around flanges, compressor seals, and flare gas recovery systems.
- Explosion-Proof Enclosure: Heavy cast aluminum and 316 stainless steel enclosures contain internal sparks, guaranteeing safety in Zone 1/2 environments.
- Man-Down & Lone-Worker Telemetry: Wireless portable units ping personal status, location, and gas peaks to safety watch teams in real time.
Frequently Asked Questions on Smart CO Safety Systems
Expert answers addressing sensor longevity, mounting physics, alarm thresholds, and factory customization capabilities.
High-grade industrial and commercial electrochemical CO sensors feature an operational lifespan of 5 to 10 years, dictated primarily by electrolyte evaporation rates and catalyst degradation. Shield smart detectors integrate an automated firmware countdown timer cross-referenced with continuous internal impedance measurements. When sensor sensitivity drops below acceptable life-safety thresholds or when the operational time limit is achieved, the unit triggers a distinct EOL acoustic chirp and visual yellow LED flash, alongside a digital supervisory trouble signal sent over the network to the central BMS.
Smoke detectors operate on optical scattering (photoelectric) or ionization principles designed to identify suspended microscopic particulate matter produced during combustion. Carbon monoxide is a pure, colorless, odorless, and completely invisible gas whose molecules (CO) cannot scatter light waves or disrupt photoelectric chambers. Therefore, a smoldering flue backdraft or an improperly tuned gas boiler emitting lethal concentrations of CO will not trigger a smoke alarm until catastrophic visible fire or soot occurs. A dedicated electrochemical sensor is mandatory to measure toxic CO gas molecules directly.
International life-safety standards such as UL 2034 and EN 50291 specify time-weighted response matrices engineered to match human carboxyhemoglobin (COHb) accumulation curves while avoiding nuisance alarms:
• At 30 ppm: No alarm allowed for at least 120 minutes (prevents false alarms from transient external traffic).
• At 50 ppm: Unit must alarm within 60 to 90 minutes.
• At 100 ppm: Unit must alarm within 10 to 40 minutes.
• At 300 ppm: Immediate alarm required within 3 minutes.
Shield commercial and industrial models also offer fully programmable instantaneous alarm setpoints (e.g., Low Alarm 25 ppm, High Alarm 50 ppm) configured to project specifications.
Upon reaching an alarm condition, the detector's internal driver discharges a high-energy capacitive pulse (typically 12VDC, 1A for 100ms) or closes an internal SPDT relay connected to the JYFJS-011 solenoid coil. This releases an internal mechanical latch, allowing a spring-loaded stainless steel valve disc to seal the gas line in less than 1 second. Safety standards strictly prohibit automatic reopening once the gas leak dissipates. The valve can only be restored by physical on-site human intervention (pulling the red reset knob), ensuring that maintenance personnel verify the pipeline integrity and isolate the hazard before fuel flow is restored.
Shield supports full end-to-end OEM/ODM private-label development for global distributors, gas utilities, and system integrators. Capabilities include: custom industrial enclosure molding (colors, private laser-etched branding, IP-grade housings), custom firmware protocol implementation (Modbus RTU, BACnet MSTP, Zigbee, LoRaWAN, proprietary RF), bespoke PCB layout design to match unique mechanical envelopes, multi-language packaging, and international certification support (providing full testing documentation for CE, ATEX, IECEx, and UL submission).
Integrated Toxic & Gas Instrumentation Portfolio
Deploy specialized handheld sniffers, pen locators, explosion-proof fixed transmitters, and multi-gas monitors for field technicians and facility managers.
Wholesale 4 in 1 Portable Gas Detector BTYQ-Z4 Series - Reliable China Suppliers and Factory for Safety Monitoring Manufacturers, Factory
Explore Model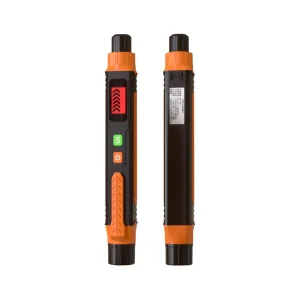
OEM Portable Gas Detector Pen Shield JLY-50A Series Suppliers, Factory
Explore Model
ODM China SD6200 Series Household Combustible Gas Detector - Reliable Safety Solution from Leading Suppliers and Factory Supplier, Factories
Explore Model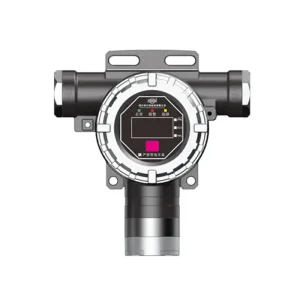
High-Quality Industrial and Commercial Gas Detector SD2100E Series from China Suppliers and Factory for Real-Time Leak Detection Manufacturer, Factory
Explore Model
High-Quality Portable Gas Detector Pen JLY-50A Series - Reliable Gas Detection by China Suppliers and Factory Manufacturer, Supplier
Explore Model
ODM China Suppliers Factory JYFJS-011 Aluminum Alloy Electromagnetic Shut-off Valve for Gas Pipeline Safety Supplier, Suppliers
Explore Model
OEM 4 in 1 Portable Gas Detector BTYQ-Z4 Series - China Suppliers and Factory for Industrial Safety Solutions Suppliers, Factory
Explore Model
Wholesale Gas Alarm Controller Shield 8001AB Series - Reliable Gas Detection Systems from China Suppliers and Factory Supplier, Factories
Explore Model