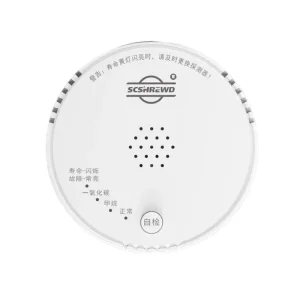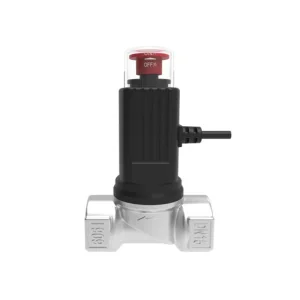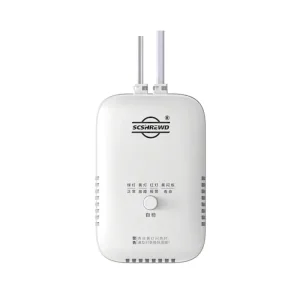
Enterprise Gas Sensing & Pipeline Isolation Engineering

High-Quality Gas Leak Detector Machine Factory & Factories

OEM/ODM Point-Type, Multi-Gas Portable Instruments, Industrial Controllers & Automated Pipeline Emergency Shut-Off Valves Engineered for Zero-Tolerance Operations.

Direct-From-Source Catalog

Featured Industrial & Residential Safety Systems

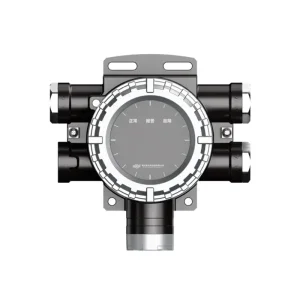
Factory-verified explosion-proof detectors, multi-channel controllers, and high-frequency solenoid valves fabricated under ISO9001 and CCC fire safety standards.
Strategic Procurement Framework

Global Sourcing Requirements in Gas Leak Detection Machinery

Procurement directors and health, safety, and environment (HSE) executives face evolving regulatory mandates. Sourcing reliable gas leak detection machinery requires balancing localized safety directives with certified manufacturing repeatability.

18+
Years Engineering Provenance
80+
Standardized Industrial Models
40+
Proprietary Patent Registrations
< 30s
High-Precision Response Time (T90)

Intrinsic Safety & Explosion-Proof Verification

Factory-direct instruments must comply with strict ATEX, IECEx, and China CCC explosion-proof standards (Ex d IIC T6 Gb / Ex ia IIC T4 Ga). Industrial deployments inside hazardous Zone 1 and Zone 2 necessitate casting designs engineered to contain internal arcs and prevent surface heat ignition under heavy hydrocarbon presence.

Sensor Topology Calibration & Longevity

Sensing matrices must be matched precisely to field conditions: catalytic bead sensors for cost-effective %LEL combustible detection, non-dispersive infrared (NDIR) sensors for oxygen-deficient and silicone-poisoning environments, and electrochemical cells for low-ppm toxic monitoring (CO, H2S, NH3).

Interoperable SCADA / DCS Architecture

Modern factory equipment must bridge local detection with plant-wide telemetry. Transmitters with standard RS-485 Modbus-RTU, 4-20mA current loops, and dry relay contacts enable direct connection to centralized Gas Alarm Controllers (such as the SD8001A/B) and industrial distributed control networks.

Integrated Safety Solutions

Macro-Industry Safety Architecture: Closing the Detection Loop

Detecting an uncontrolled hydrocarbon or toxic gas release without an automated, verified isolation protocol provides incomplete protection. Sichuan Shield Technology engineers a closed-loop ecosystem linking sensing, central dispatch, and physical gas cut-off.

Operational Segment Primary Hazard Profiles Recommended Sensing Machine System Linkage Action Compliance Reference
Petrochemical & Refinery CH4, C2H6, H2S, Voc Explosive Mixes SD2100A / SD2100E Point Detectors Trips automated deluge, reports to SD8001A/B Controller GB 15322.1, IEC 60079-29-1
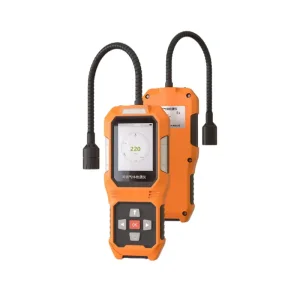
Municipal Pipeline & Regulators High-pressure Natural Gas, Methane Leaks JLY-CP100 Handheld / JLY-50A Pen Triggers acoustic warning; initiates pipeline isolation EN 50194-1, ISO 26142
Commercial Kitchens & Boilers LPG (Propane/Butane), Methane, CO SD2130 Stand-Alone Point Detector Direct relay triggers JYFJS-011 Solenoid Valve closure UL 1484, GB 15322.2
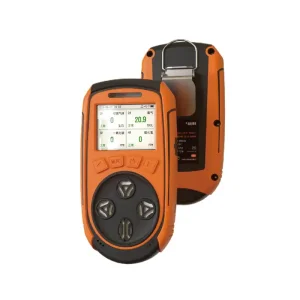
Confined Tanks, Tunnels, Sewers O2 Deficiency, CO, H2S, Explosive Gas BTYQ-Z4 4-in-1 Portable Detector Real-time personal HUD alert; telemetry tracking OSHA 1910.146, NIOSH 504
Residential Housing & Apartments Piped Town Gas, Micro-fissure Pipeline Loss SD6103K / SD6200 Household Detectors 85dB acoustic chime + pulse shut-off via solenoid EN 50194, NFPA 715
Future Outlook

Gas Sensing Technology Roadmap: 2026 and Beyond

Digital transformation across energy networks requires gas detection equipment to evolve from passive analog units into intelligent, predictive telemetry nodes.

Phase 01 · Current Standard

Solid-State Micro-Sensing

Diffusion-mode catalytic and advanced planar semiconductor micro-elements offering standard zero/span self-check, local sound-and-light alarm, and analog 4-20mA current loop output.

Phase 02 · Active Deployment

Bus Networking & Controllers

2-wire and 4-wire M-Bus / Modbus integration. Centralized supervision via SD8001A/B platforms, linking real-time concentrations across up to 128 field nodes into supervisory systems.

Phase 03 · Transition

NB-IoT / LoRaWAN Gas Gateways

Battery-optimized wireless point monitors providing direct-to-cloud MQTT streaming. Eliminates trenching costs across sprawling pipeline complexes and legacy plant retrofits.

Phase 04 · Next Generation

Edge-AI Predictive Modeling

Embedded microprocessors running atmospheric dispersion algorithms to project plume vectors and warn downstream operators before hazardous gas volumes cross safety thresholds.

OEM/ODM Engineering Direct

Localized Regulatory Alignment & Factory Assurance

Procuring direct from Sichuan Shield Technology provides global engineering support, custom enclosures, and verified compliance for international tenders.

Certified Manufacturing Lineage

Our Chengdu production base operates under ISO 9001, ISO 14001, and ISO 45001 frameworks. Every point-type instrument, portable monitor, and solenoid shut-off valve undergoes multi-point standard gas calibration and thermal chamber testing before delivery.

Full-Cycle Pipeline Isolation

Unlike factories assembling generic sensors, Shield produces precision electromagnetic shut-off valves such as the aluminum-alloy JYFJS-011. When triggered by the detector, it isolates pipeline pressure within 1 second and requires manual intervention to reset.

Private Label & OEM Flexibility

We provide distributors, system integrators, and multinational brands with private labeling, custom firmware setpoints, customized aluminum die-cast tooling, and localized interface packaging across all 80+ gas safety platforms.

Complete Equipment Fleet

Explore Specialized Detection & Shut-Off Hardware

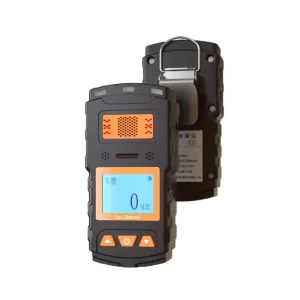
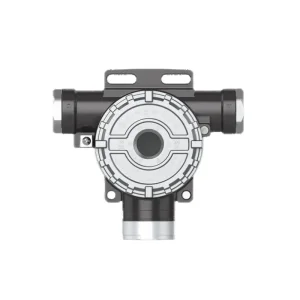
From domestic residential kitchen protection to field-patrol inspection instruments and explosion-proof point transmitters.
Procurement & Engineering FAQ

Frequently Asked Gas Leak Detection Machine Questions

Common engineering, specification, and procurement inquiries addressed by our technical team.

What is the operational distinction between LEL and Alarm Setpoint?
The Lower Explosive Limit (LEL) represents the minimum volume percentage of combustible vapor in air required to sustain a flame upon ignition (for methane, roughly 5.0% by volume = 100% LEL). Gas detector alarm thresholds are never set at the LEL; rather, they are calibrated well below it to guarantee safety buffers. The primary low-alarm (AL1) is universally established between 10% LEL and 25% LEL, while high-alarms (AL2) are capped at 50% LEL, ensuring plant personnel have ample time to isolate the leak and ventilate before explosive mixtures can accumulate.
How does target gas molecular density dictate mounting geometry?
Proper installation height is strictly dictated by the vapor density of the target medium relative to air (molecular weight ~29 g/mol). Methane (Natural Gas, MW ~16) is significantly lighter than air; therefore, detectors like the SD6103K or SD2100A must be mounted within 30 to 50 cm below the ceiling, and within 1.5 to 4 meters of potential leak points. Liquefied Petroleum Gas (LPG/Propane/Butane, MW ~44-58) is substantially heavier than air; instruments must be installed 30 cm above the finished floor to capture pooling gas before migration into drain lines or basement crawl spaces.
Why are oxygen deficiency monitors calibrated in %VOL instead of PPM?
Ambient terrestrial atmosphere naturally comprises approximately 20.9% oxygen by volume (209,000 ppm). Calculating oxygen displacement or enrichment via parts-per-million would generate cumbersome, slow-to-interpret six-digit metrics for emergency personnel. Calibration in Volume Percent (%VOL) matches standard physiological thresholds: OSHA mandates 19.5% VOL as the minimum threshold for unventilated confined-space entry, while levels exceeding 23.5% VOL indicate serious fire acceleration risk.
What is the mechanical reset requirement of emergency solenoid shut-off valves?
Safety standards dictate that an emergency shut-off valve, such as the JYFJS-011 aluminum alloy series, must utilize an electromagnetic pulse to trip the mechanical internal latch, instantly sealing the gas supply when an alarm triggers. Once tripped, the valve remains locked closed even if the detector returns to normal, power is lost, or the control loop resets. The valve must be manually reopened on site by a technician after the pipeline is inspected, preventing automatic gas re-entry into potentially damaged lines.
When should engineers choose stand-alone point detectors over bus-type architecture?
Stand-alone units such as the SD2130 series are designed for single or dual-zone decentralized applications—such as isolated commercial kitchens, standalone boiler rooms, or small paint booths. They incorporate on-board audio-visual alarms and internal relays that directly drive a shut-off valve and exhaust ventilation without an external control panel. In contrast, multi-point industrial plants, chemical storage complexes, and large energy stations require bus-type or branch-line architecture (SD2100A/E linked to SD8001A/B controllers) to centralize telemetry, support historical datalogging, and integrate with plant DCS/SCADA networks.
What OEM/ODM customization capabilities does Sichuan Shield Technology provide?
Backed by 18+ years of in-house R&D, 80+ standard platforms, and more than 40 registered patents, Shield provides complete private-label manufacturing. This includes custom CNC and aluminum die-casting, PCB layout modifications for specialized industrial communication protocols (BACnet, LoRaWAN, Zigbee, WirelessHART), customized LCD interfaces, and branded multi-language software for international distributors and gas utilities.
Compare 0/3
Get Comparison Datasheets